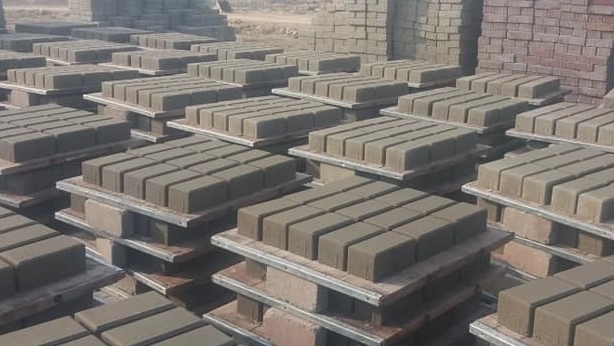
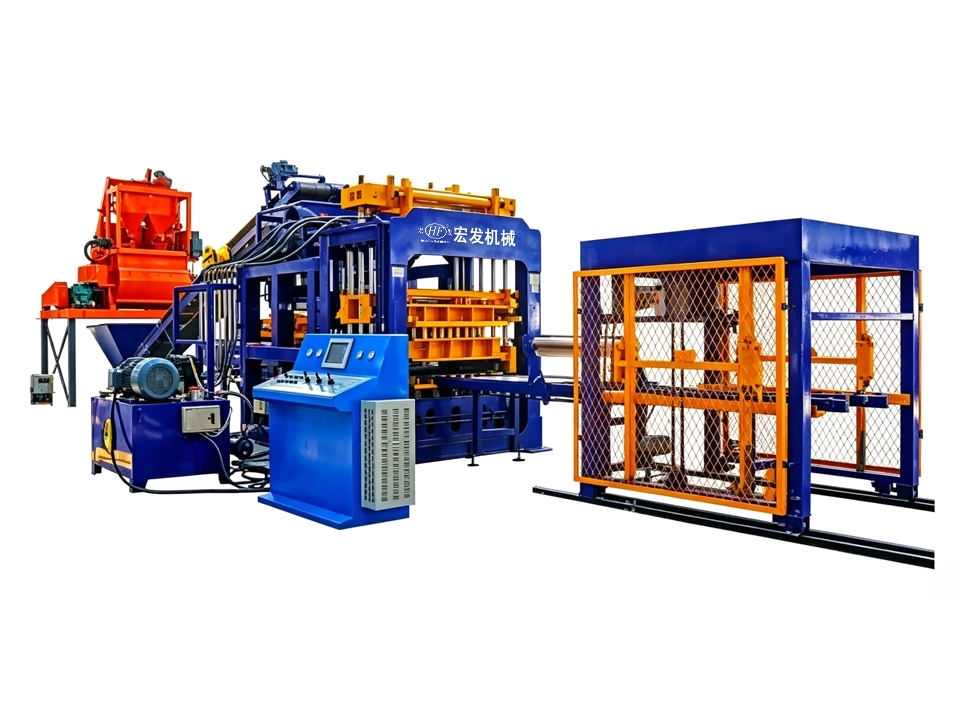
1. Deeply tuned for pavement block pressing‑vibration working condition, supports face‑mix colored blocks, premium durable bricks to win municipal & landscape orders
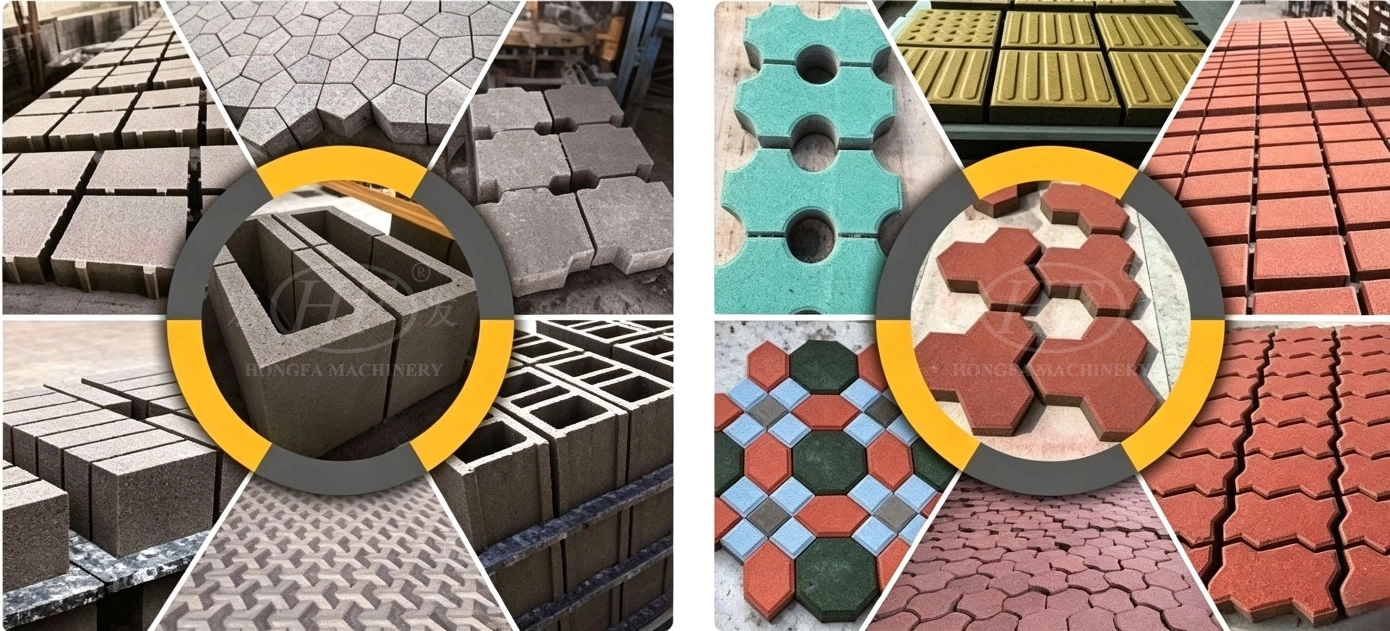
QT8‑15B optimizes table‑vibration and pressing coordination to meet surface density and wear‑resistance requirements for paving blocks and permeable bricks. Optional independent face‑mix feeder produces colored‑surface pavement blocks with firm color layer, avoiding common defects like color fading, sanding and surface peeling. Finished pavement blocks feature high compactness, good freeze‑thaw and wear‑resisting performance that meet overseas municipal construction standards. Low dimensional deviation guarantees neat paving effect. High‑quality finished blocks support both bulk dealer supply and project bidding, bringing higher product premium. It helps you secure more high‑value pavement block orders and reduce losses caused by unqualified brick returns and claims.
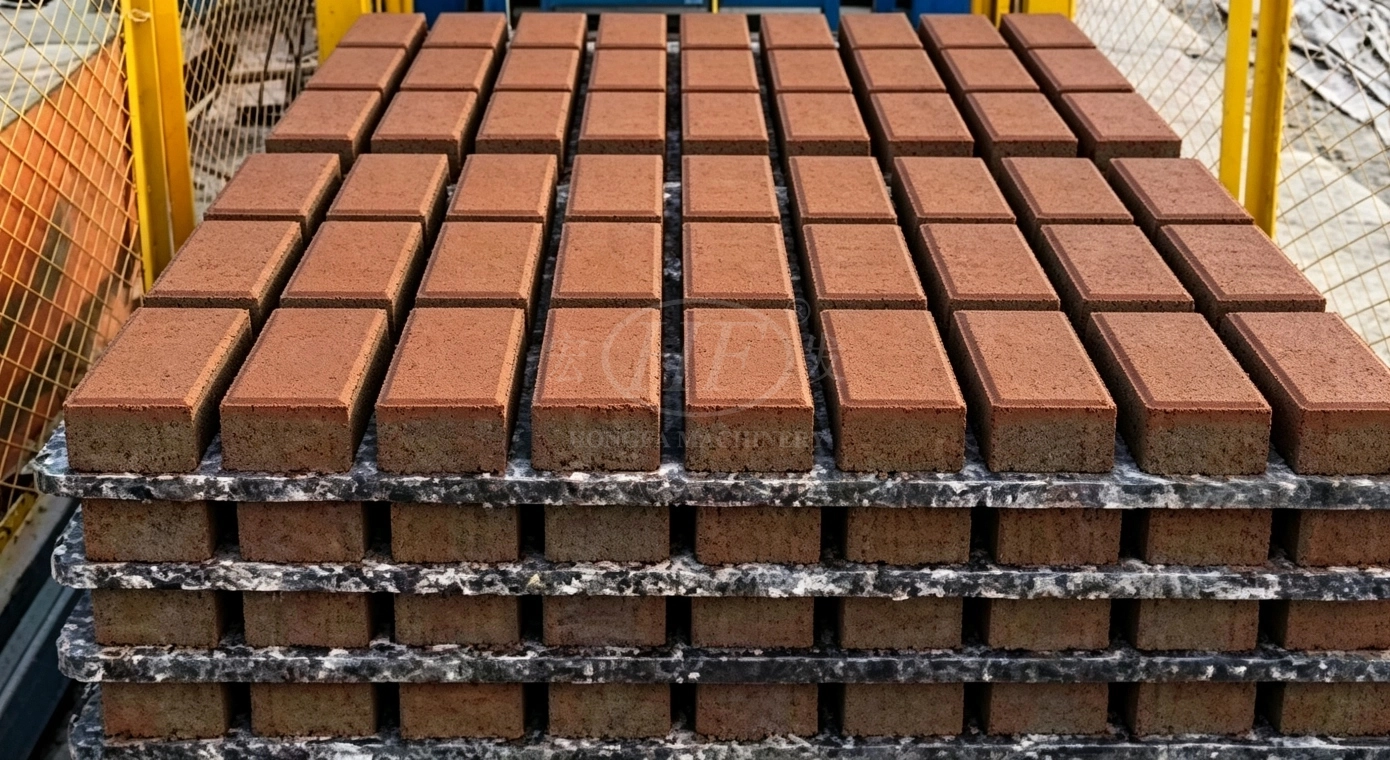
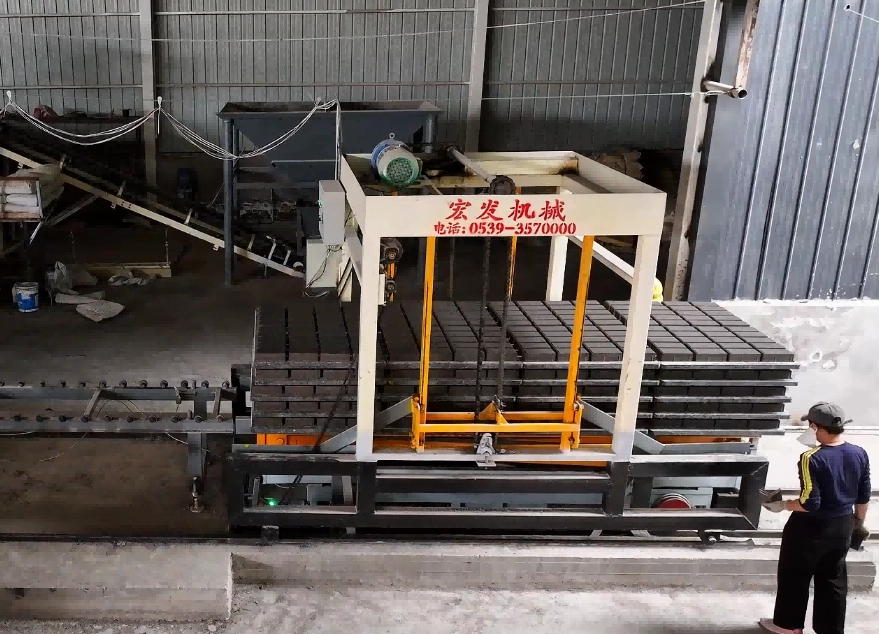
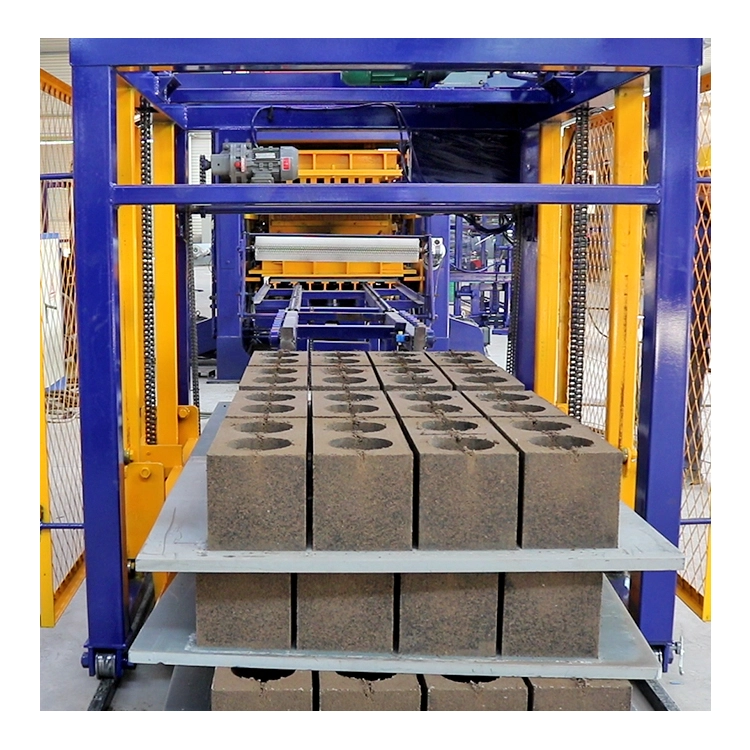
2. High‑capacity automatic cyclic production, more blocks per mold, handle large‑volume pavement orders and prevent order loss
The full workflow including feeding, face‑mix dosing, pressing‑vibration, demolding and pallet conveying runs in automatic closed‑loop. Only minimal operators are required for on‑site supervision and green block handling. Thanks to large mold cavity design, multiple pavement blocks are formed in one single cycle with short cycle time for long‑hour continuous production. When receiving large‑volume orders from municipal projects or trading companies, stable hourly output shortens overall production cycle and ensures on‑time delivery. You do not need to purchase extra main machines for peak‑season production. Labor cost per brick is reduced and factory revenue is maximized.
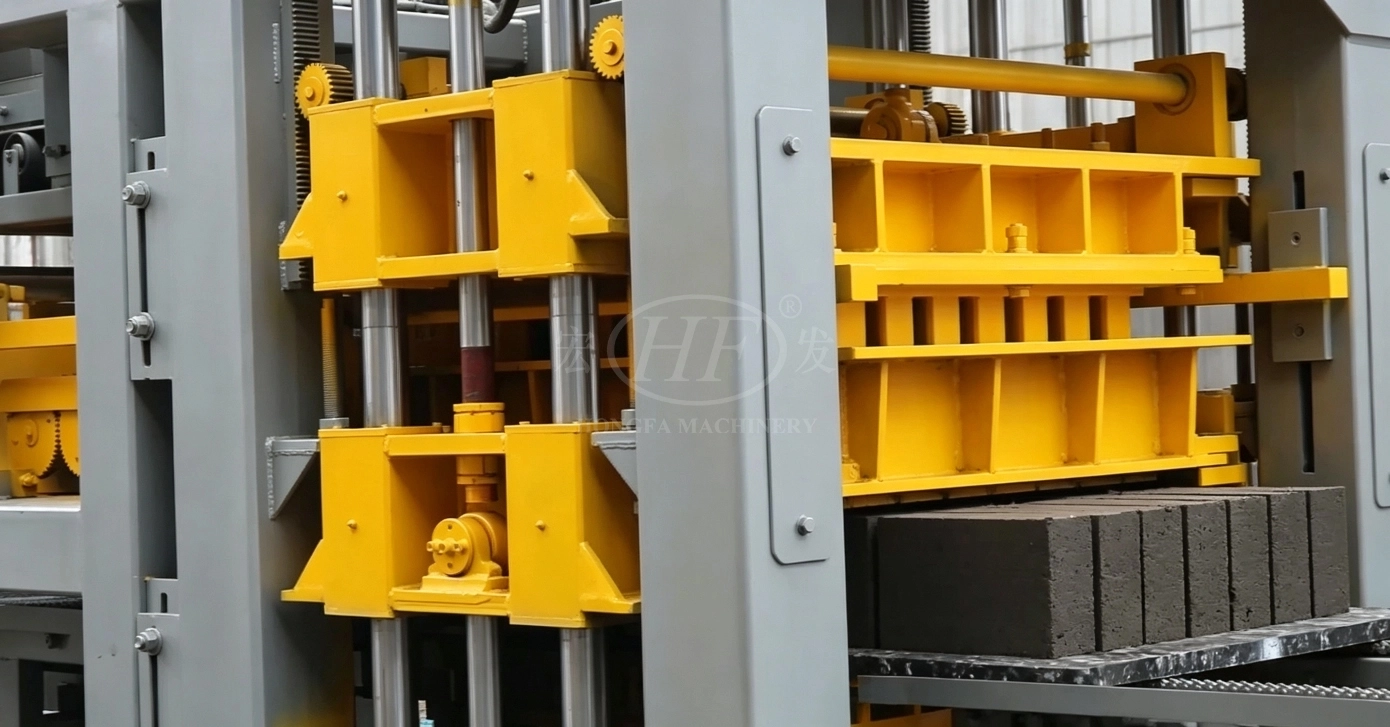
3. Heavy‑duty reinforced frame for frequent continuous pavement block production, less downtime, lower maintenance & order‑breach cost
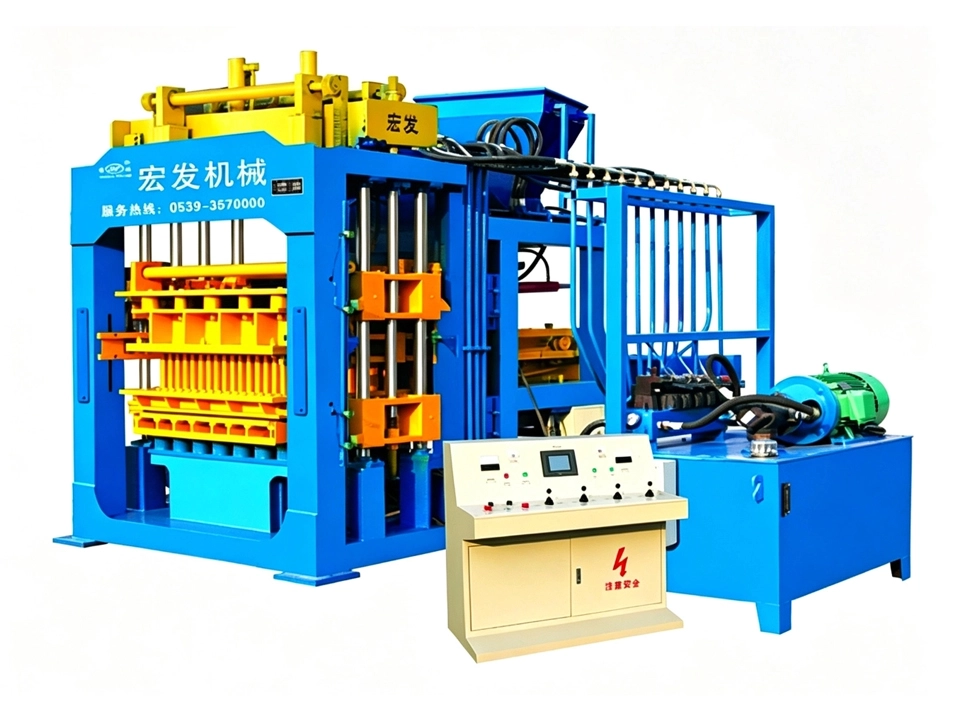
Continuous pavement block production brings high‑frequency vibration and repeated pressure impact. QT8‑15B adopts heavy‑duty thickened steel welded frame plus external independent integrated hydraulic station. Hydraulic components are physically separated from high‑vibration mainframe to reduce damage from dust and continuous vibration for cylinders and valve groups. Improved anti‑fatigue performance adapts to non‑stop pavement‑block mass production. Unexpected shutdown risk is greatly reduced, avoiding green block scrap, raw material waste, delivery delay and customer compensation. Less spare‑part replacement lowers long‑term operation cost and ensures stable production scheduling for pavement block orders with extended service life.
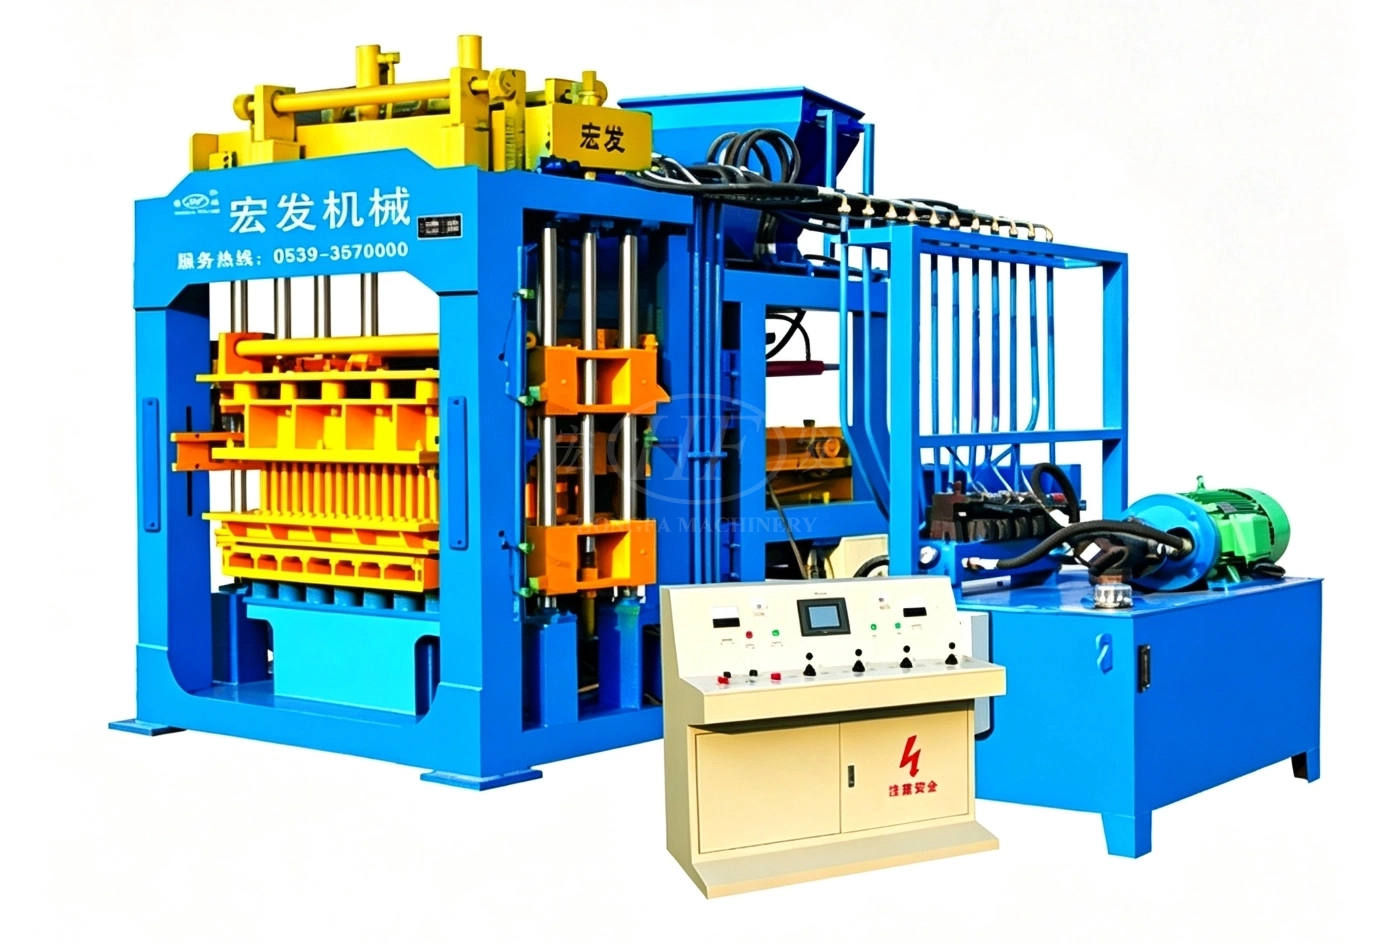
4. PLC touch‑screen with saved process profiles, fast specification change‑over for pavement blocks, less trial‑run waste for mixed orders
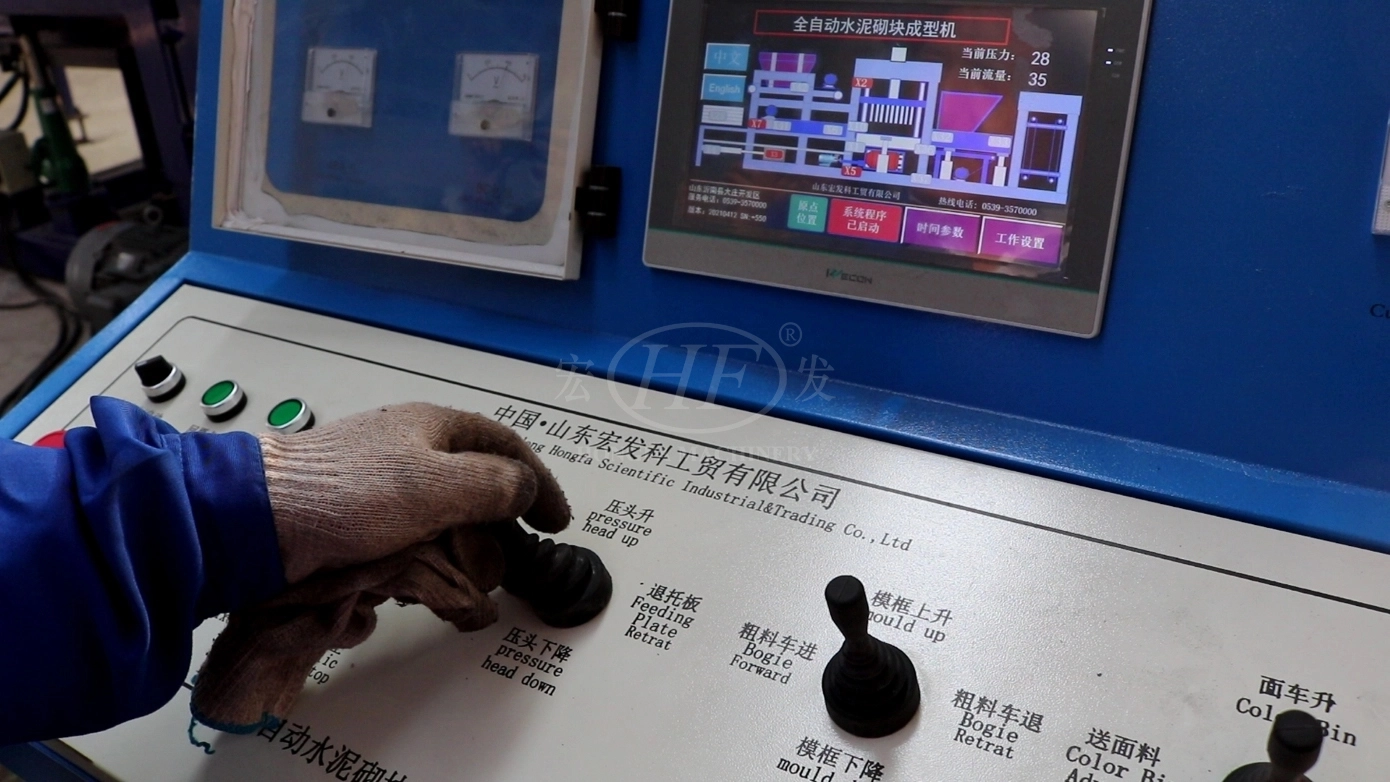
Equipped with PLC controller and industrial touch‑screen HMI. Process parameters including face‑mix feeding duration, pre‑vibration, main vibration and pressure holding for different thickness and porosity pavement / permeable bricks can be saved as independent brick profiles. When switching among various pavement block specifications, recall saved parameters directly instead of repeated manual tuning. It shortens change‑over time and reduces defective bricks and raw‑material waste during trial‑run. Built‑in safety interlock prevents mis‑operation damage and lowers operator skill requirement. Mixed‑batch orders combining permeable bricks, standard paving tiles and thick‑spec blocks can be processed efficiently to satisfy diversified customer procurement.
5. Wide raw‑material compatibility, utilize local industrial waste for pavement blocks, cut logistics cost and boost profit margin
QT8‑15B forming system accepts flexible raw‑material formulas for pavement blocks. Besides standard sand and stone, local cheap materials such as stone dust, slag, fly ash and recycled construction waste can be mixed with cement for production. Sourcing materials nearby eliminates expensive long‑distance transportation. While keeping pavement block indexes of wear‑resistance, compression and water permeability qualified, cement ratio can be reasonably optimized to lower unit production cost. Cost advantage strengthens your quotation competitiveness in overseas building‑material business, and ensures decent profit for both volume‑based general‑grade orders and high‑demand colored pavement block projects.
6. Modular quick‑change mold, extendable full pavement‑block production line, multi‑product capability for better return on investment
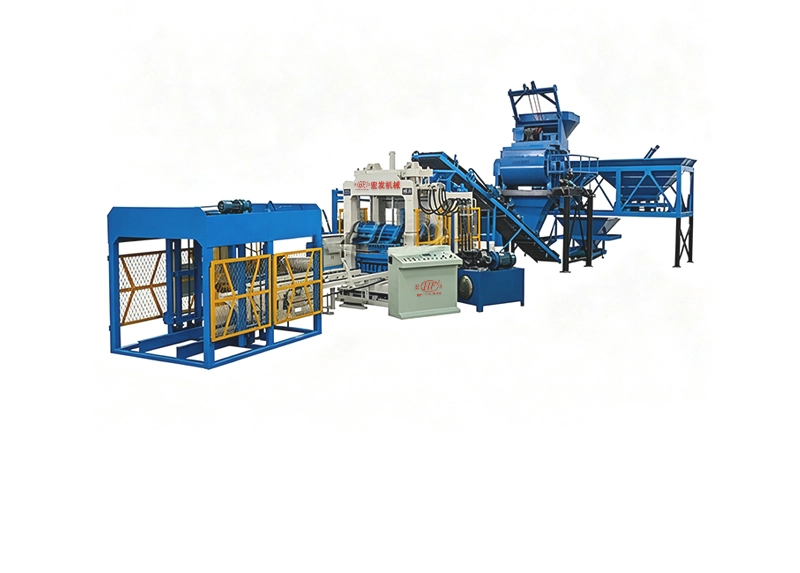
Modular quick‑change mold structure enables fast switch between different sizes and thicknesses of pavement blocks and permeable bricks. One single machine also produces grass‑planting blocks, curbstones and small slope‑protection blocks for municipal use. No need to invest in multiple forming hosts for different building products, cutting your initial capital expenditure. You can select batching silos, forced mixers, face‑mix system, conveyors and automatic stackers according to your workshop size, budget and target output to build semi‑automatic or fully‑automatic complete pavement‑block production line. One‑stop solution avoids multi‑supplier sourcing and compatibility risks. Mass production can be launched quickly after equipment arrival to accelerate payback period.
1. Deeply tuned for pavement block pressing‑vibration working condition, supports face‑mix colored blocks, premium durable bricks to win municipal & landscape orders
QT8‑15B optimizes table‑vibration and pressing coordination to meet surface density and wear‑resistance requirements for paving blocks and permeable bricks. Optional independent face‑mix feeder produces colored‑surface pavement blocks with firm color layer, avoiding common defects like color fading, sanding and surface peeling. Finished pavement blocks feature high compactness, good freeze‑thaw and wear‑resisting performance that meet overseas municipal construction standards. Low dimensional deviation guarantees neat paving effect. High‑quality finished blocks support both bulk dealer supply and project bidding, bringing higher product premium. It helps you secure more high‑value pavement block orders and reduce losses caused by unqualified brick returns and claims.
2. High‑capacity automatic cyclic production, more blocks per mold, handle large‑volume pavement orders and prevent order loss
The full workflow including feeding, face‑mix dosing, pressing‑vibration, demolding and pallet conveying runs in automatic closed‑loop. Only minimal operators are required for on‑site supervision and green block handling. Thanks to large mold cavity design, multiple pavement blocks are formed in one single cycle with short cycle time for long‑hour continuous production. When receiving large‑volume orders from municipal projects or trading companies, stable hourly output shortens overall production cycle and ensures on‑time delivery. You do not need to purchase extra main machines for peak‑season production. Labor cost per brick is reduced and factory revenue is maximized.
3. Heavy‑duty reinforced frame for frequent continuous pavement block production, less downtime, lower maintenance & order‑breach cost
Continuous pavement block production brings high‑frequency vibration and repeated pressure impact. QT8‑15B adopts heavy‑duty thickened steel welded frame plus external independent integrated hydraulic station. Hydraulic components are physically separated from high‑vibration mainframe to reduce damage from dust and continuous vibration for cylinders and valve groups. Improved anti‑fatigue performance adapts to non‑stop pavement‑block mass production. Unexpected shutdown risk is greatly reduced, avoiding green block scrap, raw material waste, delivery delay and customer compensation. Less spare‑part replacement lowers long‑term operation cost and ensures stable production scheduling for pavement block orders with extended service life.
4. PLC touch‑screen with saved process profiles, fast specification change‑over for pavement blocks, less trial‑run waste for mixed orders
Equipped with PLC controller and industrial touch‑screen HMI. Process parameters including face‑mix feeding duration, pre‑vibration, main vibration and pressure holding for different thickness and porosity pavement / permeable bricks can be saved as independent brick profiles. When switching among various pavement block specifications, recall saved parameters directly instead of repeated manual tuning. It shortens change‑over time and reduces defective bricks and raw‑material waste during trial‑run. Built‑in safety interlock prevents mis‑operation damage and lowers operator skill requirement. Mixed‑batch orders combining permeable bricks, standard paving tiles and thick‑spec blocks can be processed efficiently to satisfy diversified customer procurement.
5. Wide raw‑material compatibility, utilize local industrial waste for pavement blocks, cut logistics cost and boost profit margin
QT8‑15B forming system accepts flexible raw‑material formulas for pavement blocks. Besides standard sand and stone, local cheap materials such as stone dust, slag, fly ash and recycled construction waste can be mixed with cement for production. Sourcing materials nearby eliminates expensive long‑distance transportation. While keeping pavement block indexes of wear‑resistance, compression and water permeability qualified, cement ratio can be reasonably optimized to lower unit production cost. Cost advantage strengthens your quotation competitiveness in overseas building‑material business, and ensures decent profit for both volume‑based general‑grade orders and high‑demand colored pavement block projects.
6. Modular quick‑change mold, extendable full pavement‑block production line, multi‑product capability for better return on investment
Modular quick‑change mold structure enables fast switch between different sizes and thicknesses of pavement blocks and permeable bricks. One single machine also produces grass‑planting blocks, curbstones and small slope‑protection blocks for municipal use. No need to invest in multiple forming hosts for different building products, cutting your initial capital expenditure. You can select batching silos, forced mixers, face‑mix system, conveyors and automatic stackers according to your workshop size, budget and target output to build semi‑automatic or fully‑automatic complete pavement‑block production line. One‑stop solution avoids multi‑supplier sourcing and compatibility risks. Mass production can be launched quickly after equipment arrival to accelerate payback period.
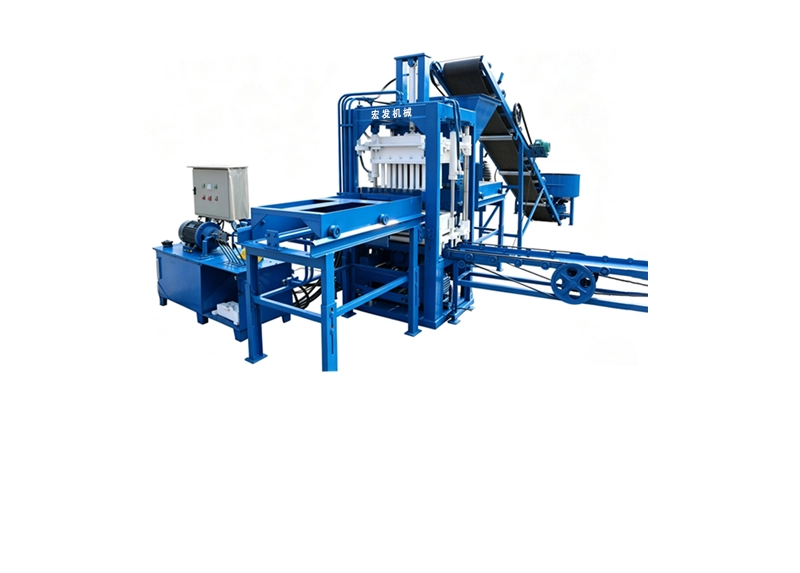 QT3-15 Automatic Concrete Hollow Block Making Machine | Stable High Output for Hollow Blocks
QT3-15 automatic hollow block machine is specially built for hollow block production. It forms multiple hollow blocks in...
 QT3‑15 Fully‑Automatic Solid Brick Making Machine | Concrete Standard Solid Brick Production Line
Hongfa QT3‑15 fully‑automatic solid brick making machine produces 39 pieces of 240×115×53mm standard solid bricks per mo...
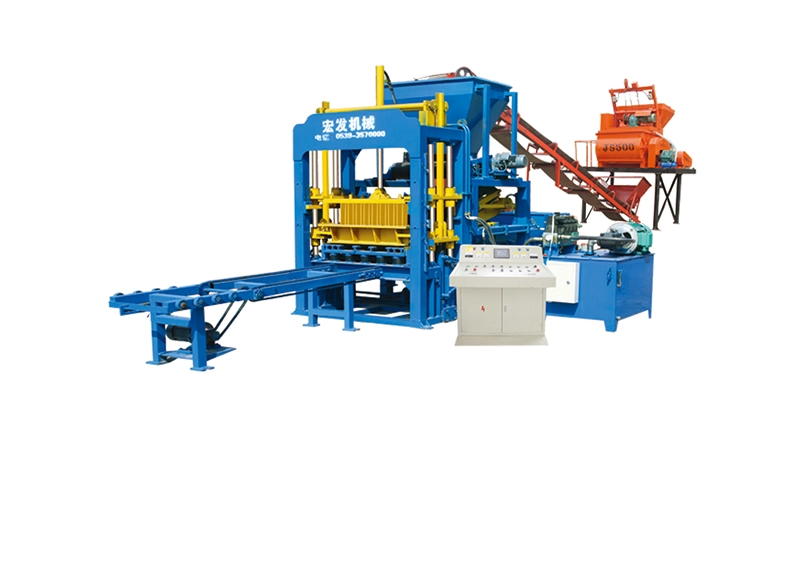 QT4-15 Automatic Concrete Brick Making Machine
QT4-15 automatic concrete brick making machine is an upgraded version of QTY4-20 with higher output and better product q...
Shandong Hongfa Scientific Industrial&Trading Co.,Ltd ©️2026Copyright © LU ICP B 16041216-4