1. Table‑vibration Box & Hydraulic Combined Pressing, Solid Block Ribs & Lower Defect Rate
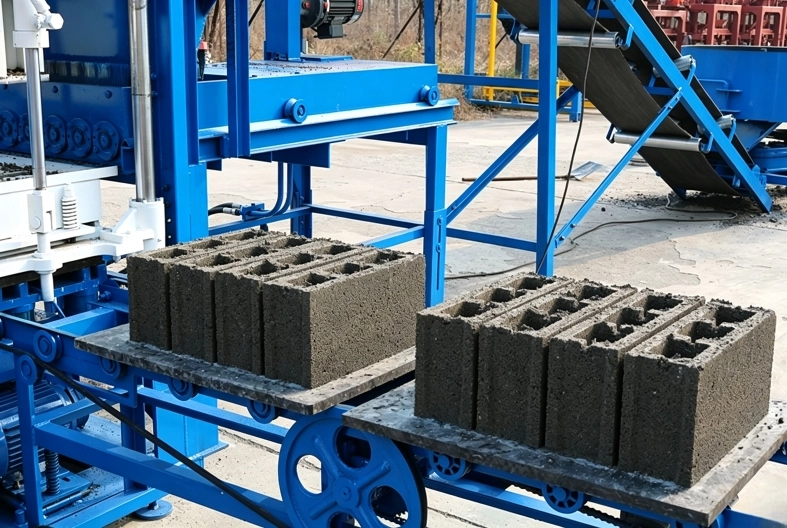
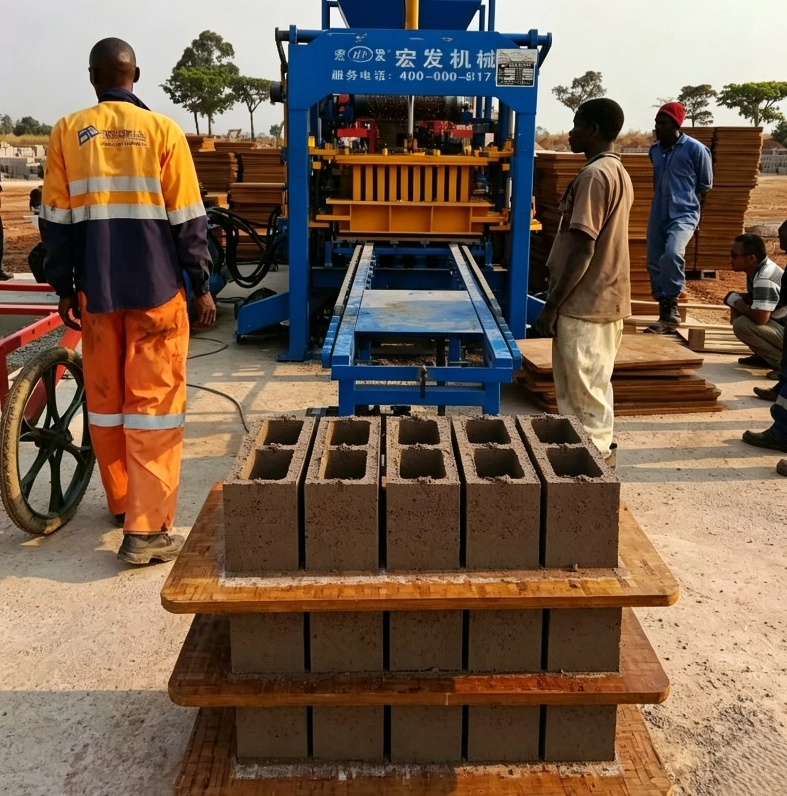
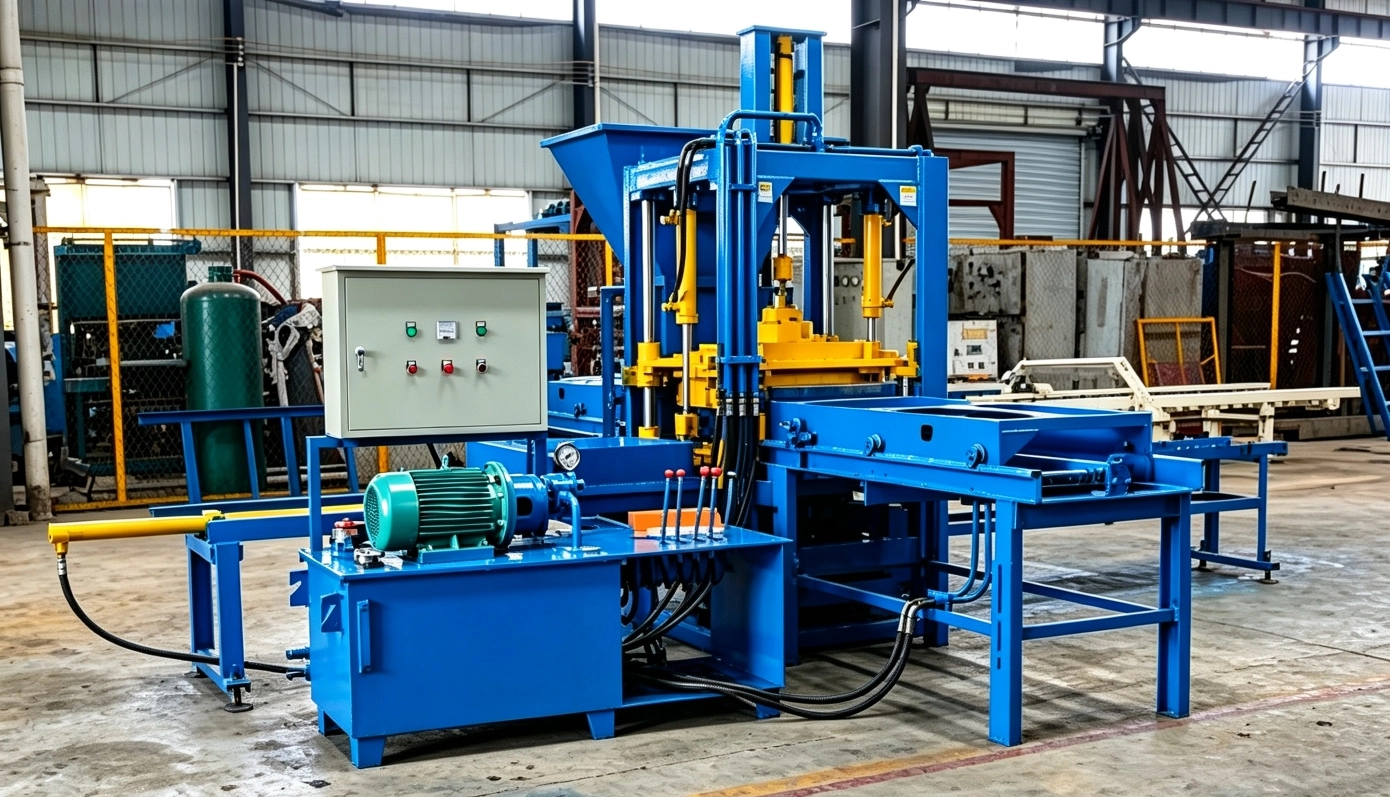
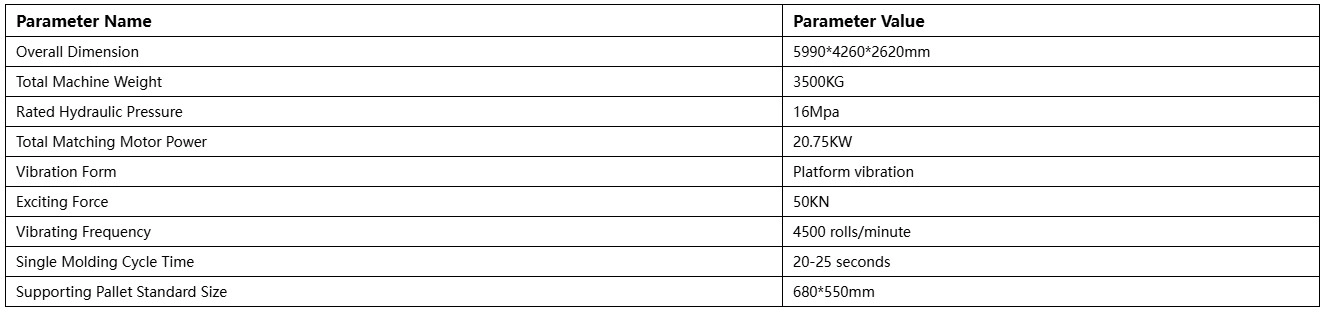
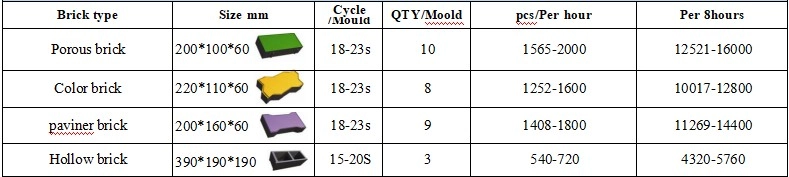
Insufficient material filling around core moulds often leads to broken ribs and cavity collapse and mass rejects. QTF3‑20 host adopts vibration‑box transmission instead of direct motor drive, cooperating with 16 Mpa hydraulic pressure. 50 KN high exciting force at 4500 r/min transfers vibration fully into every mould cavity to fill hollow‑block ribs completely. Finished hollow blocks own neat cavity outline, sturdy unbreakable ribs, uniform density, stable compression strength and small dimensional deviation. Raw‑material waste caused by cavity collapse, rib fracture and corner chipping is greatly reduced. Finished blocks pass acceptance standards for housing and municipal projects. It helps you obtain stable hollow‑block supply contracts and avoid financial loss from defective returns, protecting local and overseas customer reputation.
2. PLC Automatic HMI Control, Full‑forming‑cycle Auto‑operation & Less Skilled‑labor Dependence
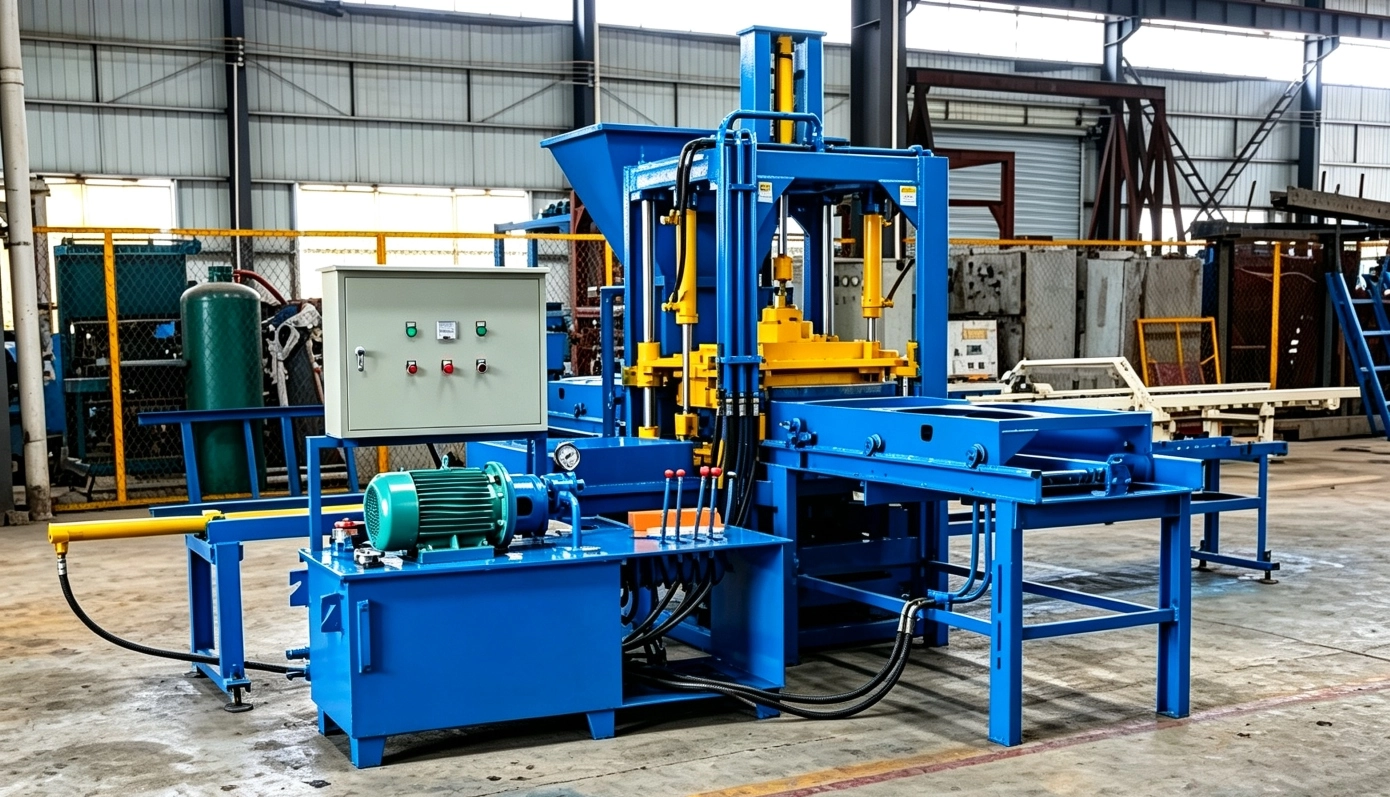
Equipped with PLC intelligent control system and HMI panel. Material feeding, pre‑vibration, pressing, demoulding, pallet feeding and brick ejection run automatically. Built‑in production logic and status prompt. Ordinary workers can operate after simple training without senior technicians. It reduces brick quality fluctuation caused by manual mis‑operation and eases labor‑recruitment pressure. Stable forming rhythm is maintained during long continuous running to guarantee on‑time delivery for hollow‑block orders, perfectly matching large‑volume continuous hollow‑block production of medium‑size factories.
3. Strong Host Expandability, Freely‑selectable Auxiliary Equipment & Controlled Up‑front Cost
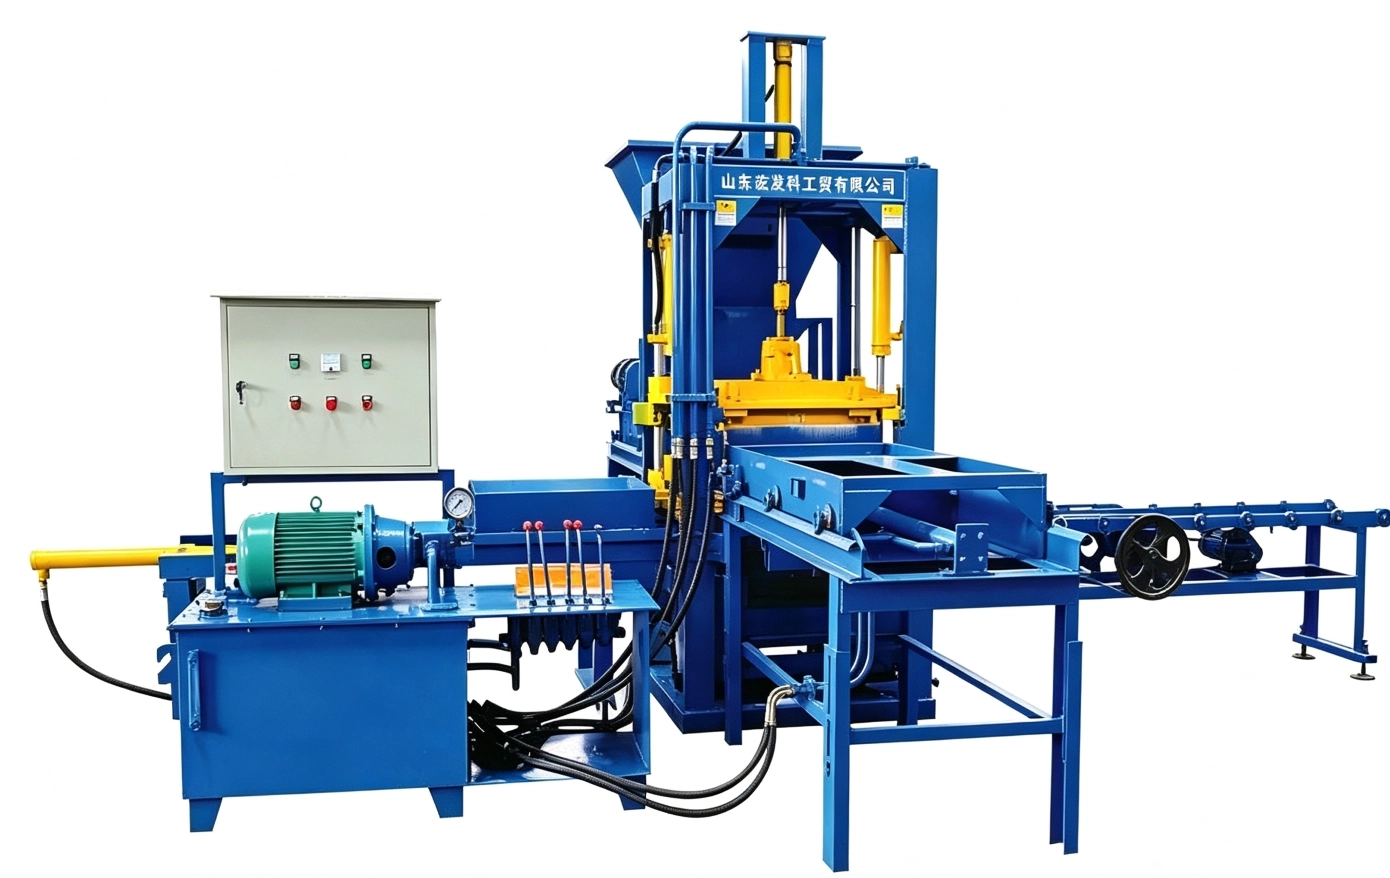
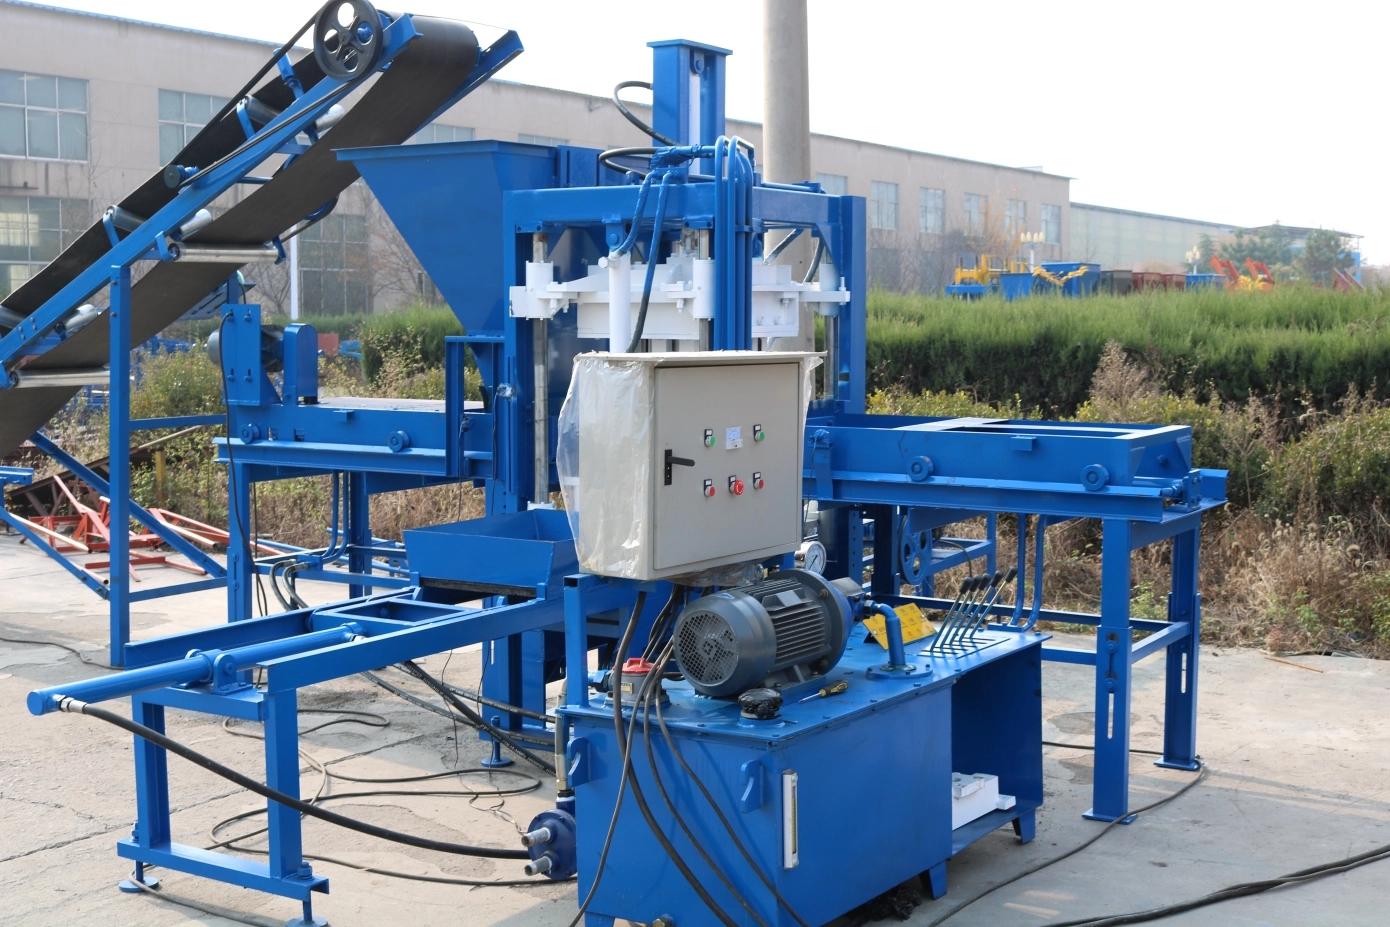
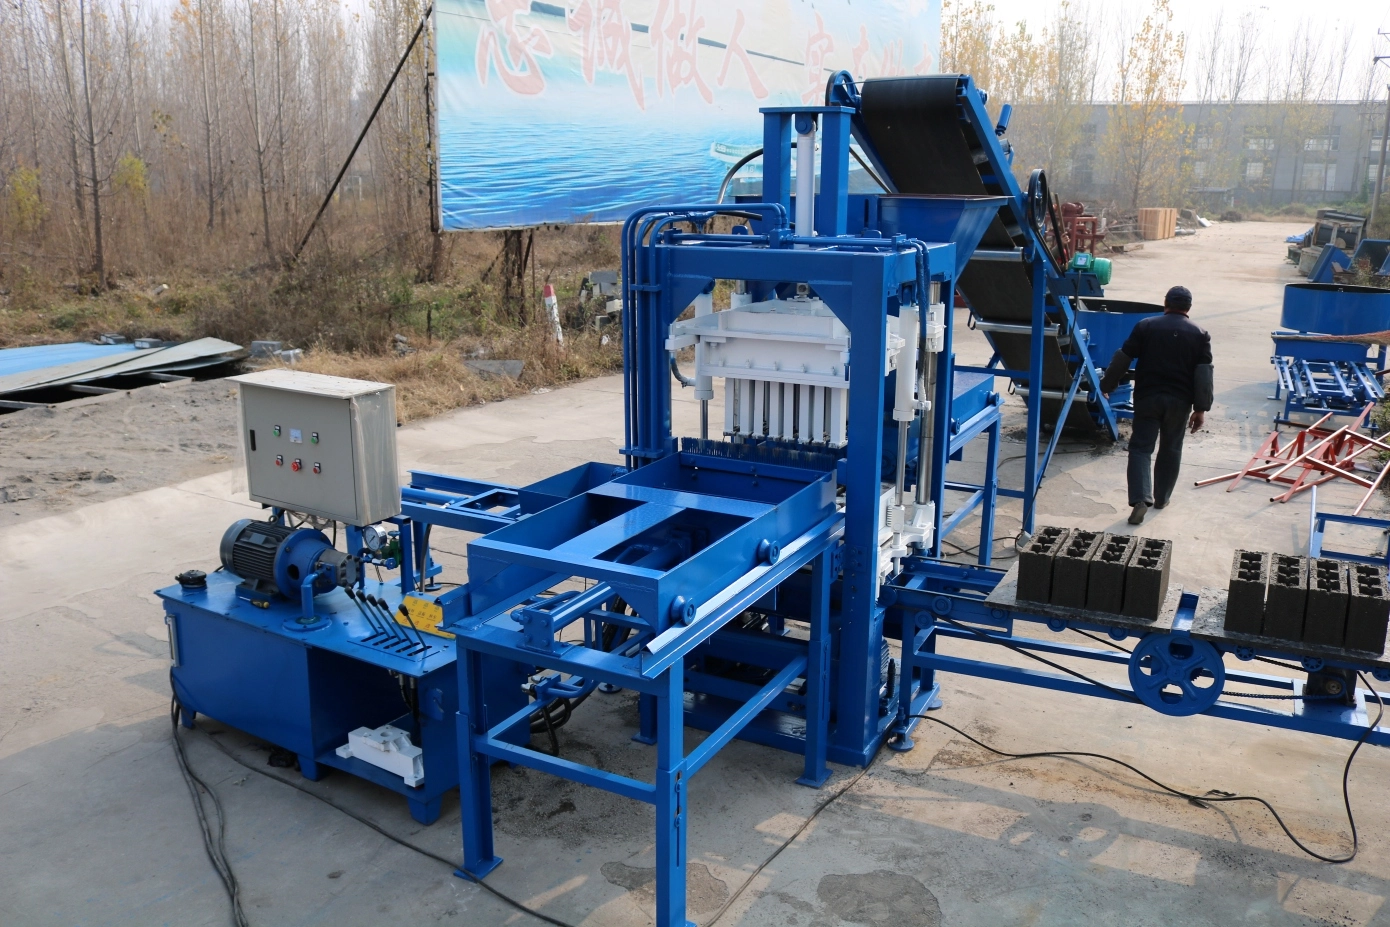
The forming host can run independently or connect with external JQ400 mixer, belt conveyor and automatic stacker. You are not forced to purchase all auxiliary devices at one time. Budget‑limited buyers can start with only the host and add supporting equipment later when orders expand. Compact footprint, works on ordinary hardened concrete floor without heavy‑duty civil foundation. You can configure accessories step‑by‑step according to actual order volume and avoid heavy one‑time capital pressure, lowering entry barrier for hollow‑block manufacturing business.
4. Carburized High‑manganese‑steel Mould, Quick‑change for Multiple Hollow‑block Sizes to Expand Order Sources
Moulds for this host are made of high‑manganese steel with carburizing heat treatment and precise wire‑cut processing, featuring good wear and impact resistance against repeated hollow‑block pressing. You can swap mould assemblies without major host disassembly to produce hollow blocks of different wall thickness and dimensions. It also supports perforated bricks and paving blocks. One single host handles various hollow‑block specifications, no need to invest in multiple forming machines to amortize equipment cost. Maximize machine runtime in peak season and quickly switch for special‑size hollow‑block orders, improving equipment utilization rate and reducing idle downtime.
5. Wide Raw‑material Compatibility, Utilize Local Industrial Waste to Reduce Raw‑material Expense
High‑grade river sand is not compulsory for hollow‑block production. Qualified hollow blocks can be manufactured by mixing limited cement with crushed stone, stone dust, fly ash, cinder, slag, coal gangue, expanded perlite and other industrial residues. You can source cheap local quarry waste and industrial by‑products as main raw materials and cut long‑distance aggregate transportation cost. Stable production can be kept even when premium sand is scarce or price rises. Lower comprehensive material cost brings stronger pricing flexibility, helping you win construction orders or maintain decent profit margin.
6. Robust Steel Frame & Premium Hydraulic Parts, Stable Heavy‑load Operation & Reduce Order‑delay Risk
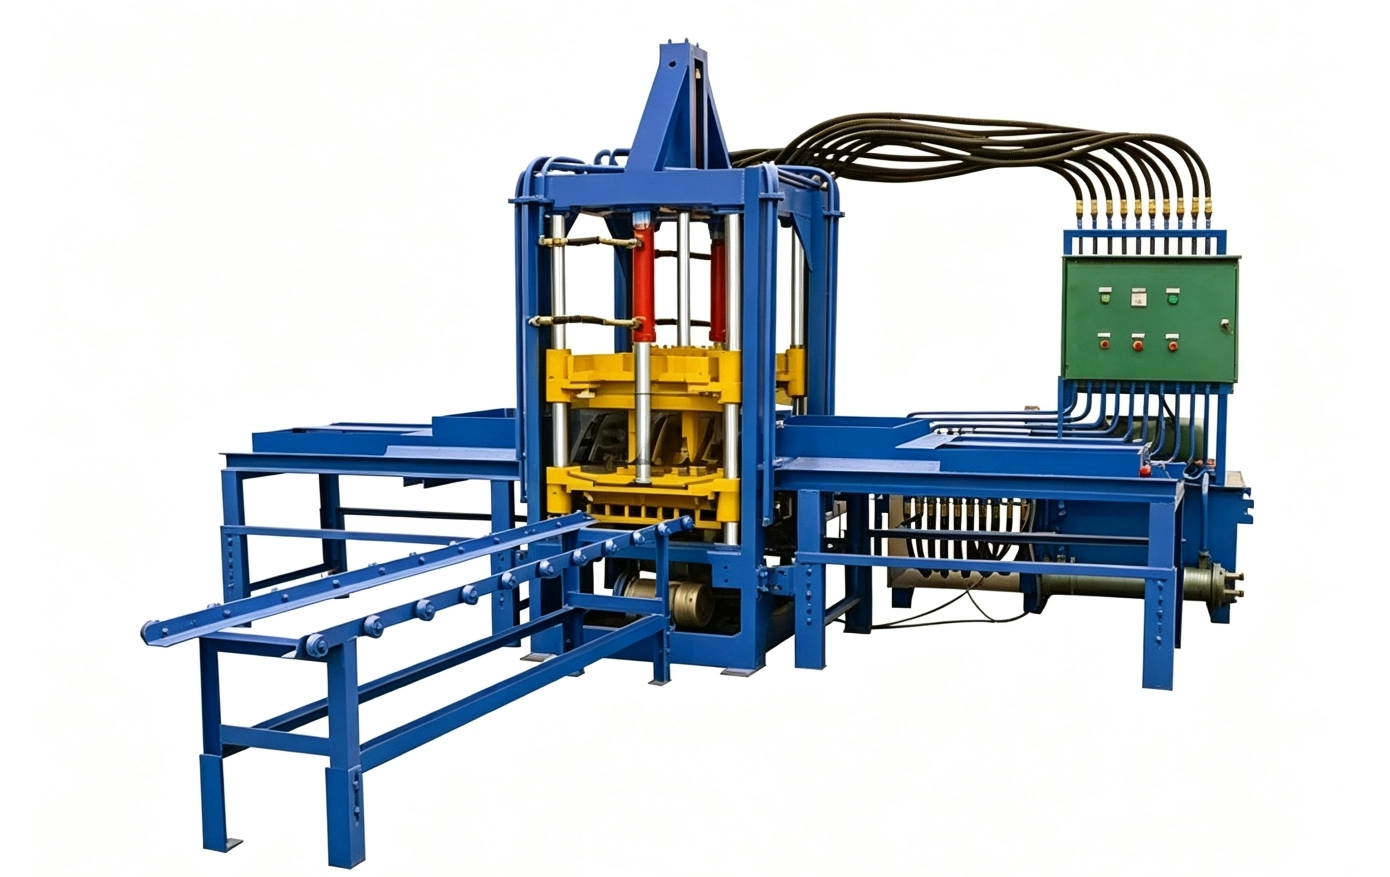
Main frame is welded with heavy‑wall 12×12 cm square steel from Laiwu & Jinggang steel mill for high rigidity, designed for frequent heavy‑load mould vibration of hollow‑block production. Adopt well‑known Taiwan Calyca hydraulic components. Vibration‑box structure protects motors from burnout. Total host weight reaches 3500 kg for solid performance. Key wearing parts are standard industry‑wide items, easy to purchase and replace in overseas local markets instead of waiting for original spare‑parts shipment. It lowers unexpected shutdown risk after hollow‑block supply contracts are signed, extends effective production hours and improves host return‑on‑investment.
1. Table‑vibration Box & Hydraulic Combined Pressing, Solid Block Ribs & Lower Defect Rate
Insufficient material filling around core moulds often leads to broken ribs and cavity collapse and mass rejects. QTF3‑20 host adopts vibration‑box transmission instead of direct motor drive, cooperating with 16 Mpa hydraulic pressure. 50 KN high exciting force at 4500 r/min transfers vibration fully into every mould cavity to fill hollow‑block ribs completely. Finished hollow blocks own neat cavity outline, sturdy unbreakable ribs, uniform density, stable compression strength and small dimensional deviation. Raw‑material waste caused by cavity collapse, rib fracture and corner chipping is greatly reduced. Finished blocks pass acceptance standards for housing and municipal projects. It helps you obtain stable hollow‑block supply contracts and avoid financial loss from defective returns, protecting local and overseas customer reputation.
2. PLC Automatic HMI Control, Full‑forming‑cycle Auto‑operation & Less Skilled‑labor Dependence
Equipped with PLC intelligent control system and HMI panel. Material feeding, pre‑vibration, pressing, demoulding, pallet feeding and brick ejection run automatically. Built‑in production logic and status prompt. Ordinary workers can operate after simple training without senior technicians. It reduces brick quality fluctuation caused by manual mis‑operation and eases labor‑recruitment pressure. Stable forming rhythm is maintained during long continuous running to guarantee on‑time delivery for hollow‑block orders, perfectly matching large‑volume continuous hollow‑block production of medium‑size factories.
3. Strong Host Expandability, Freely‑selectable Auxiliary Equipment & Controlled Up‑front Cost
The forming host can run independently or connect with external JQ400 mixer, belt conveyor and automatic stacker. You are not forced to purchase all auxiliary devices at one time. Budget‑limited buyers can start with only the host and add supporting equipment later when orders expand. Compact footprint, works on ordinary hardened concrete floor without heavy‑duty civil foundation. You can configure accessories step‑by‑step according to actual order volume and avoid heavy one‑time capital pressure, lowering entry barrier for hollow‑block manufacturing business.
4. Carburized High‑manganese‑steel Mould, Quick‑change for Multiple Hollow‑block Sizes to Expand Order Sources
Moulds for this host are made of high‑manganese steel with carburizing heat treatment and precise wire‑cut processing, featuring good wear and impact resistance against repeated hollow‑block pressing. You can swap mould assemblies without major host disassembly to produce hollow blocks of different wall thickness and dimensions. It also supports perforated bricks and paving blocks. One single host handles various hollow‑block specifications, no need to invest in multiple forming machines to amortize equipment cost. Maximize machine runtime in peak season and quickly switch for special‑size hollow‑block orders, improving equipment utilization rate and reducing idle downtime.
5. Wide Raw‑material Compatibility, Utilize Local Industrial Waste to Reduce Raw‑material Expense
High‑grade river sand is not compulsory for hollow‑block production. Qualified hollow blocks can be manufactured by mixing limited cement with crushed stone, stone dust, fly ash, cinder, slag, coal gangue, expanded perlite and other industrial residues. You can source cheap local quarry waste and industrial by‑products as main raw materials and cut long‑distance aggregate transportation cost. Stable production can be kept even when premium sand is scarce or price rises. Lower comprehensive material cost brings stronger pricing flexibility, helping you win construction orders or maintain decent profit margin.
6. Robust Steel Frame & Premium Hydraulic Parts, Stable Heavy‑load Operation & Reduce Order‑delay Risk
Main frame is welded with heavy‑wall 12×12 cm square steel from Laiwu & Jinggang steel mill for high rigidity, designed for frequent heavy‑load mould vibration of hollow‑block production. Adopt well‑known Taiwan Calyca hydraulic components. Vibration‑box structure protects motors from burnout. Total host weight reaches 3500 kg for solid performance. Key wearing parts are standard industry‑wide items, easy to purchase and replace in overseas local markets instead of waiting for original spare‑parts shipment. It lowers unexpected shutdown risk after hollow‑block supply contracts are signed, extends effective production hours and improves host return‑on‑investment.
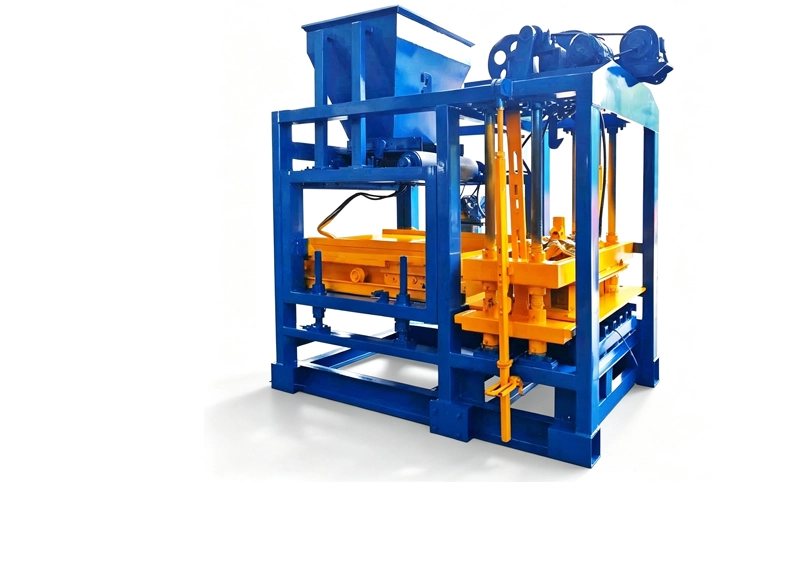 QT4‑25 Fully Automatic Concrete Solid Brick Making Machine | High‑capacity Solid Brick Production Equipment for Medium‑small Factories
QT4‑25 automatic solid brick production machine, specially built for mass‑production of building‑grade standard solid br...

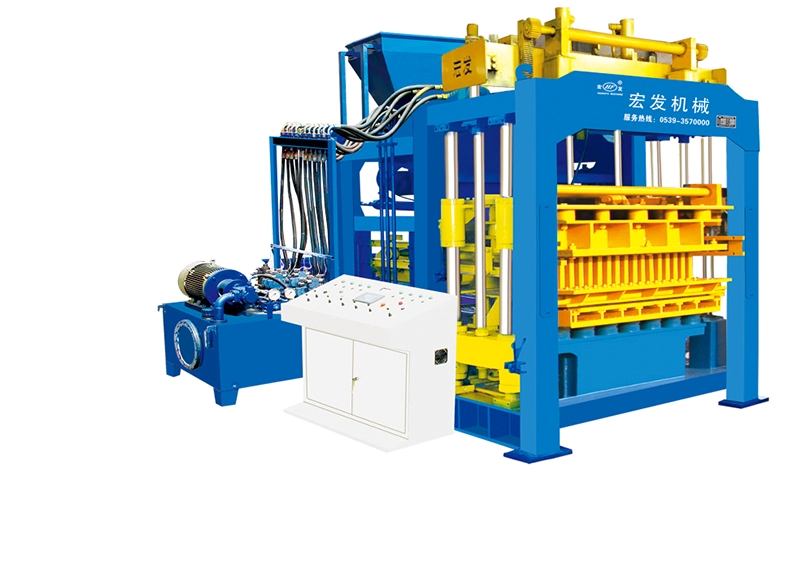 QT12‑15 Fully Automatic Concrete Hollow Block Making Machine | High‑Capacity Hollow Block Machine Host
QT12‑15 automatic hollow block production machine, specially designed for mass‑production of building‑grade concrete hol...
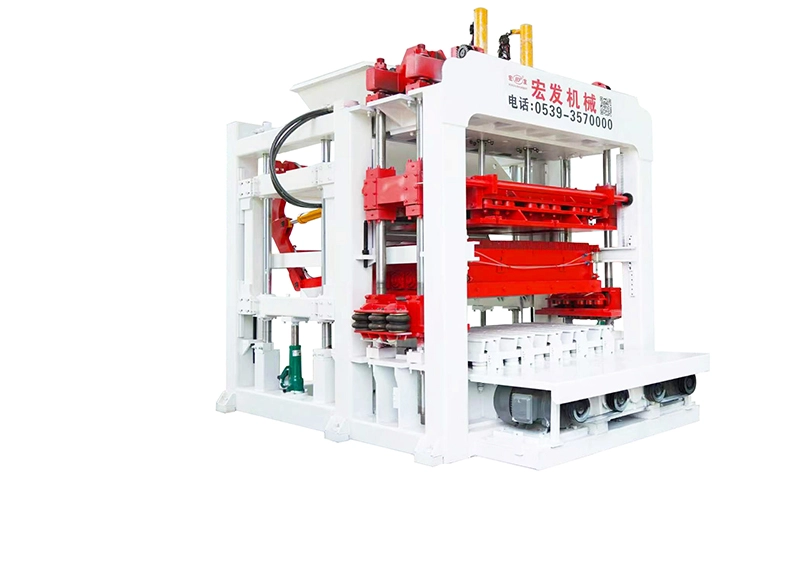 QT12‑15 Fully Automatic Concrete Curb Stone Making Machine | High‑Output Curbstone Brick Machine
QT12‑15 automatic curb‑stone production machine, specially built for mass‑production of municipal road curbstones. High‑...
Shandong Hongfa Scientific Industrial&Trading Co.,Ltd ©️2026Copyright © LU ICP B 16041216-4