1. Compact small‑pallet design, lower consumable cost for solid‑brick production in space‑limited workshops
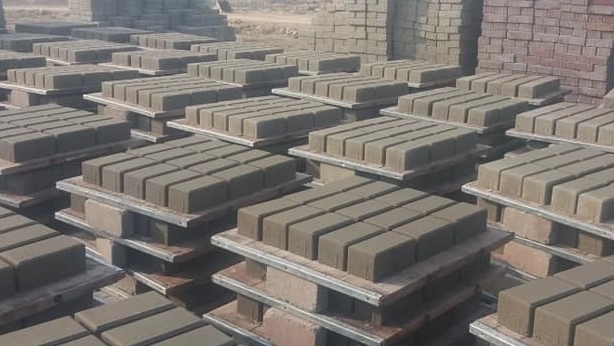
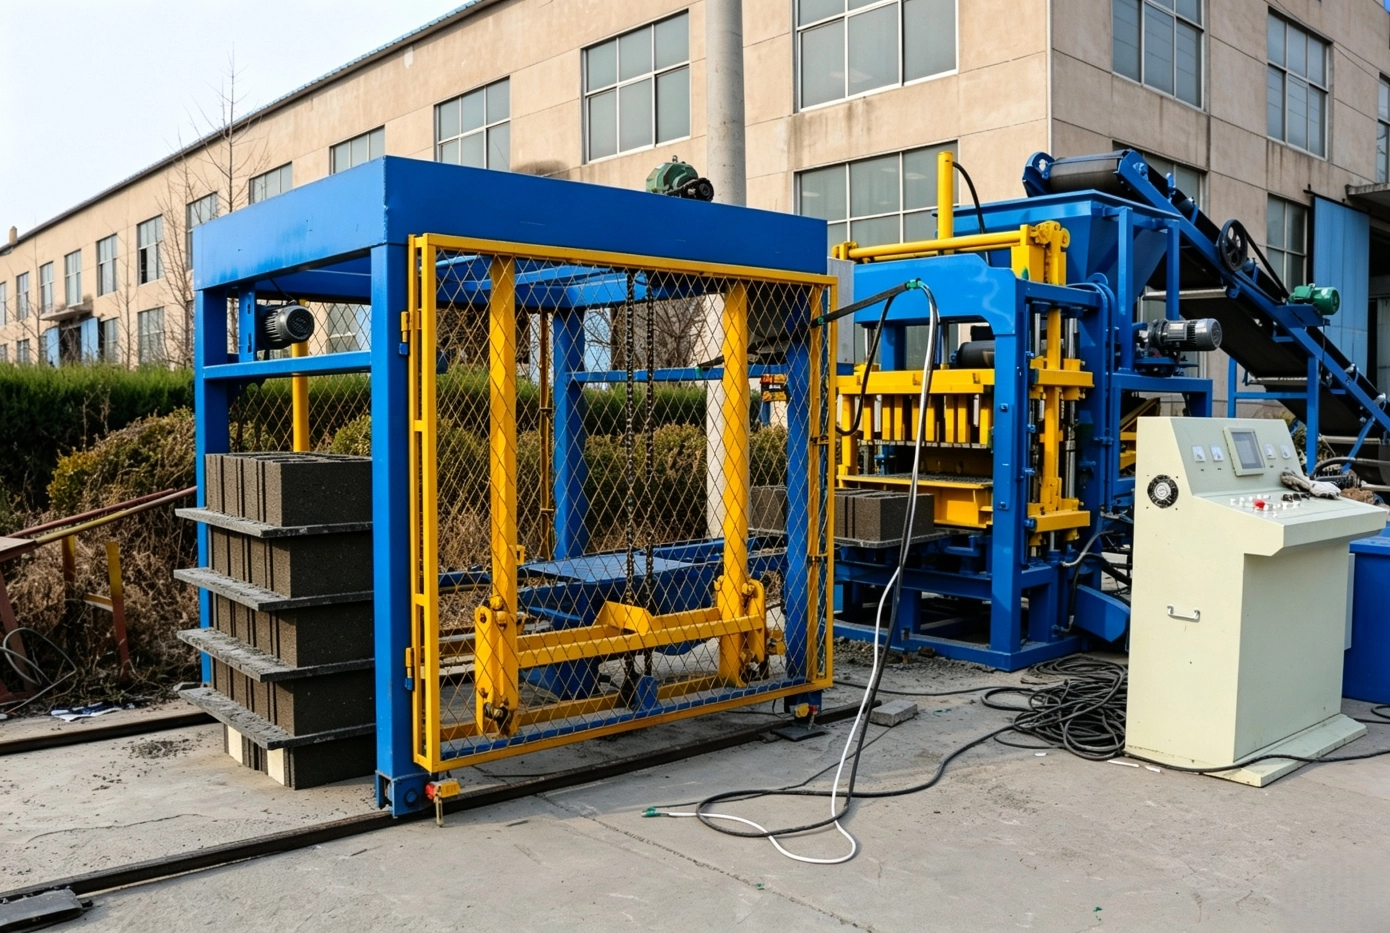
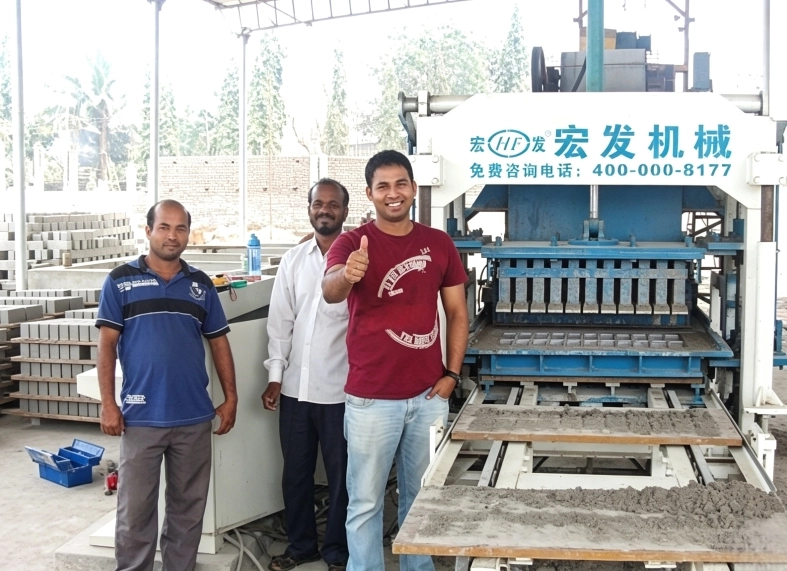
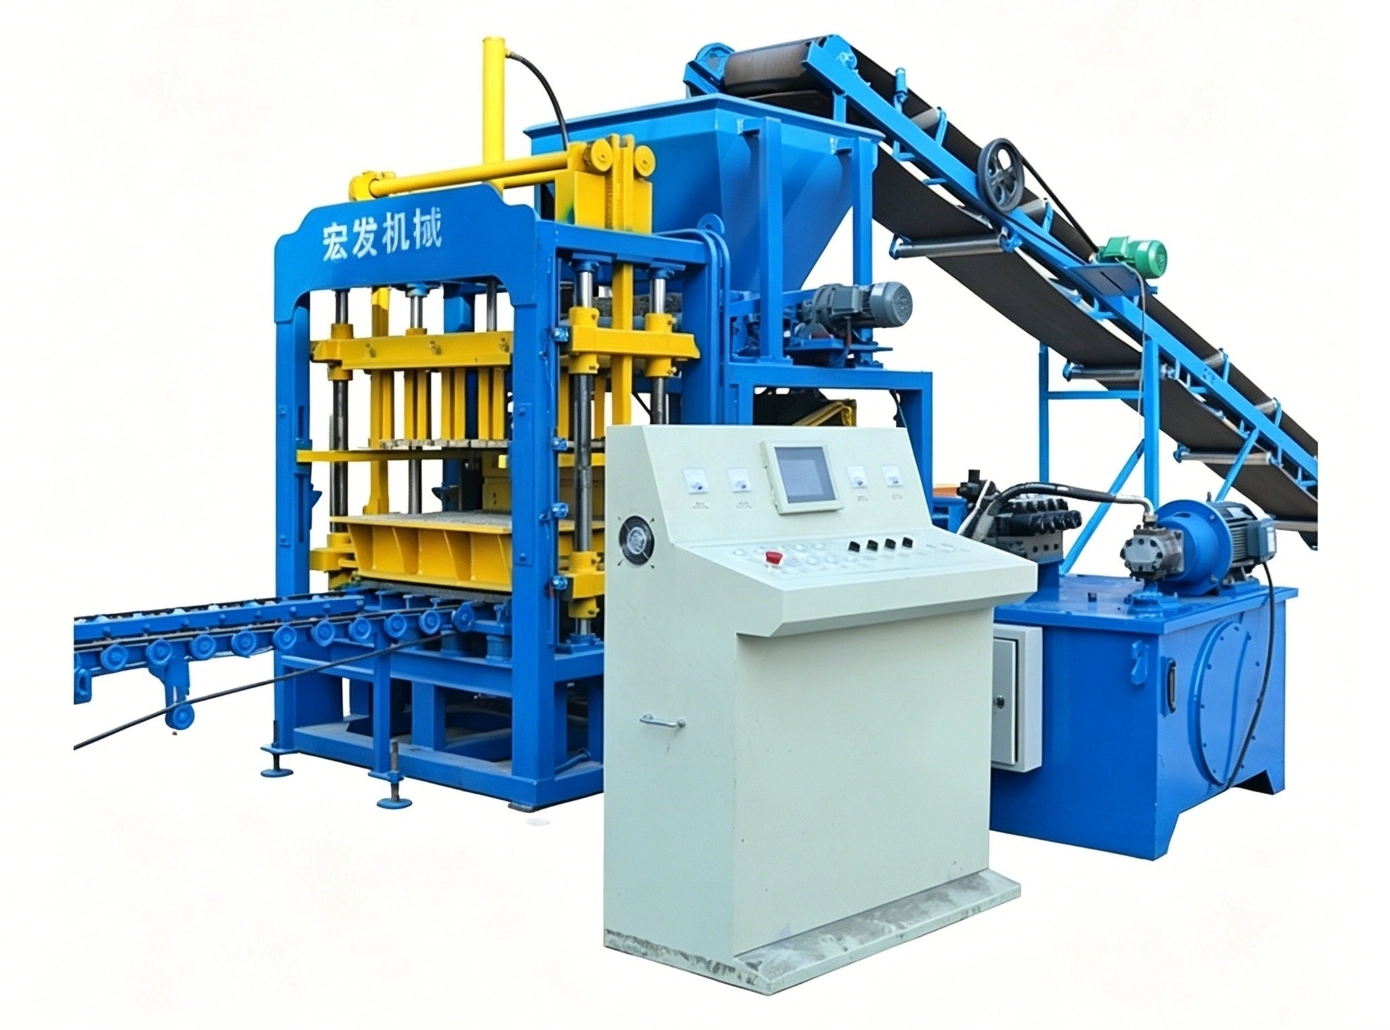
Many small overseas brick factories are restricted by workshop size. Large‑pallet brick machines demand bigger buildings and bring high ongoing pallet‑replacement expense, since pallets are wearing parts. QT4‑15S uses economical 900×550 mm pallets. It delivers 21 standard solid bricks per mould and outputs 35000‑40000 solid bricks per 8‑hour shift without large‑size workshop. Pallet purchasing and replacement cost is kept low, and alternative pallet materials are easier to source locally. You can launch solid‑brick mass‑production inside existing plant space, cutting civil‑work and consumable investment for new or space‑constrained investors.
2. Isolated vibration‑box drive structure, solve high‑frequency motor burnout risk in solid‑brick mass‑production and reduce unplanned‑shutdown loss
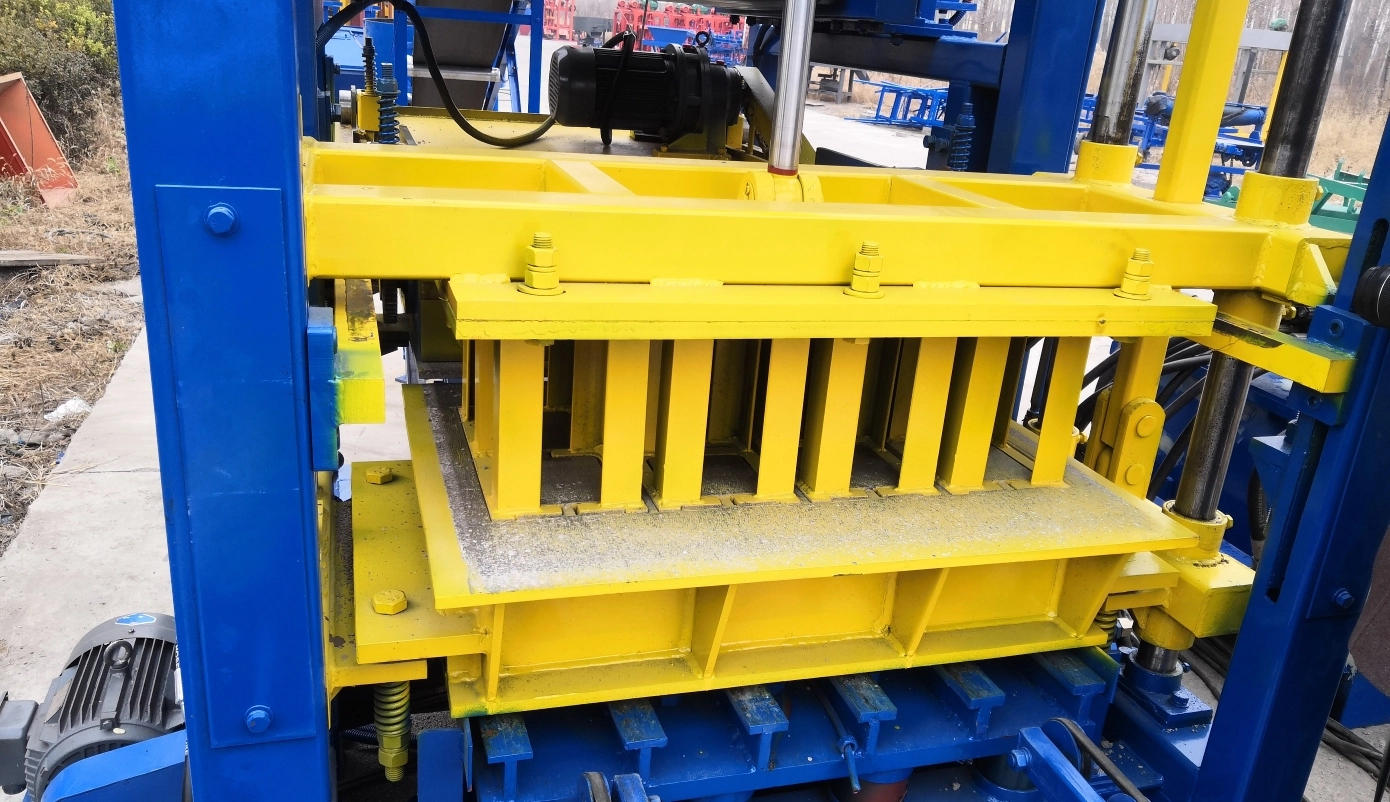
Solid‑brick production runs under continuous heavy vibration. Traditional direct‑motor‑driven machines make motors vibrate together with mould assembly. Motors burn out frequently during long‑hour solid‑brick manufacturing. Once motors fail, the whole line stops. For overseas buyers, spare‑part lead time is long and may cause contract penalties. QT4‑15S applies independent enclosed vibration‑box to transmit exciting force. Motors are physically separated from vibration source and free from heavy oscillation, drastically lowering burnout risk. 16‑MPa hydraulic pressure together with 55‑KN exciting force guarantees thorough compaction for every solid brick. It cuts time‑cost of overseas spare‑part procurement and secures on‑time delivery for large‑volume solid‑brick contracts.
3. Native compatibility with color‑facing system, one line handles main solid‑brick orders plus occasional municipal paver jobs to boost machine utilization
Most brick factories rely heavily on solid‑brick orders while receiving sporadic municipal paver tenders. Without built‑in support for color facing material, you either reject those orders or invest in a second idle machine. QT4‑15S reserves mechanical interface for optional color feeder. You can run high‑volume solid‑brick production as core business. When paver orders arrive, enable the color‑facing module without major host modification to produce colored paving blocks. One single production line absorbs two types of business, improves machine running rate and avoids extra heavy equipment investment for small‑batch paver demands.
4. High green‑brick strength after molding, permit direct multi‑layer stacking, less brick breakage and lower manual stacking workload
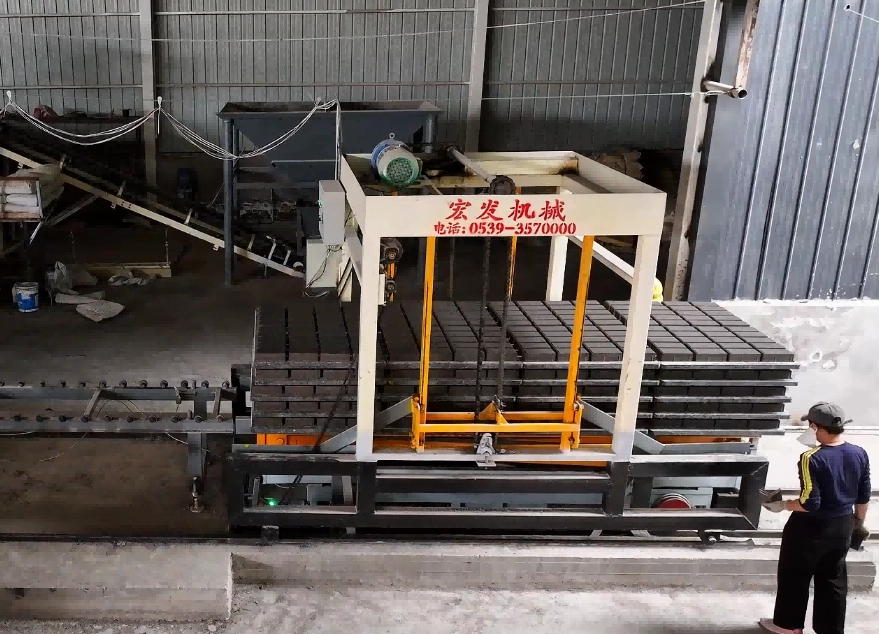
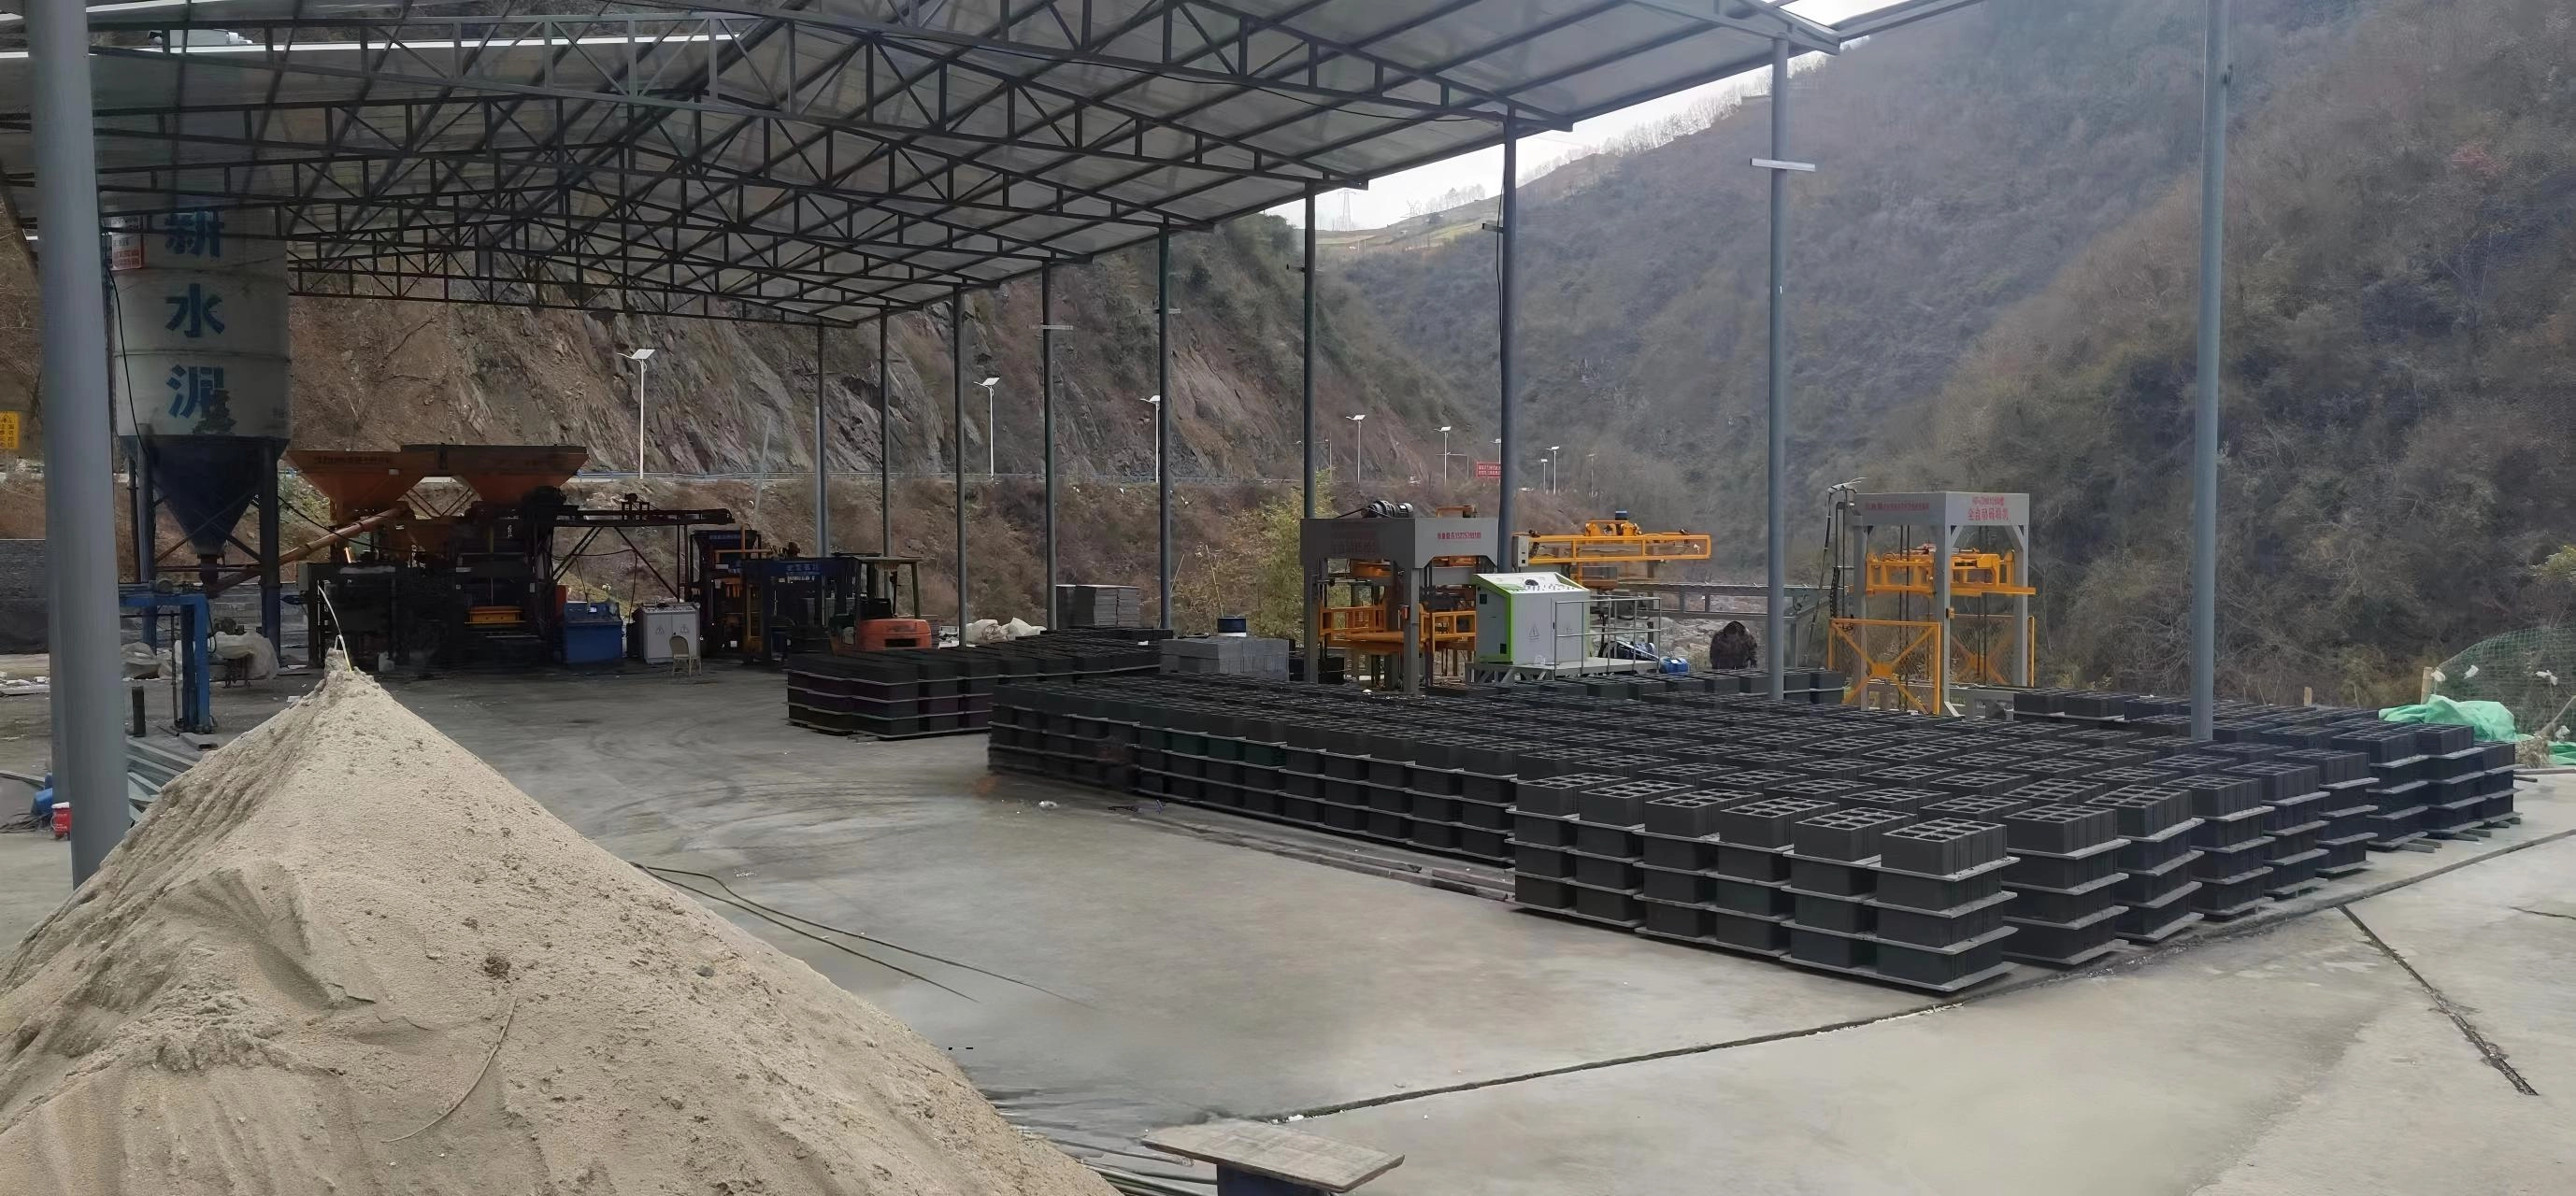
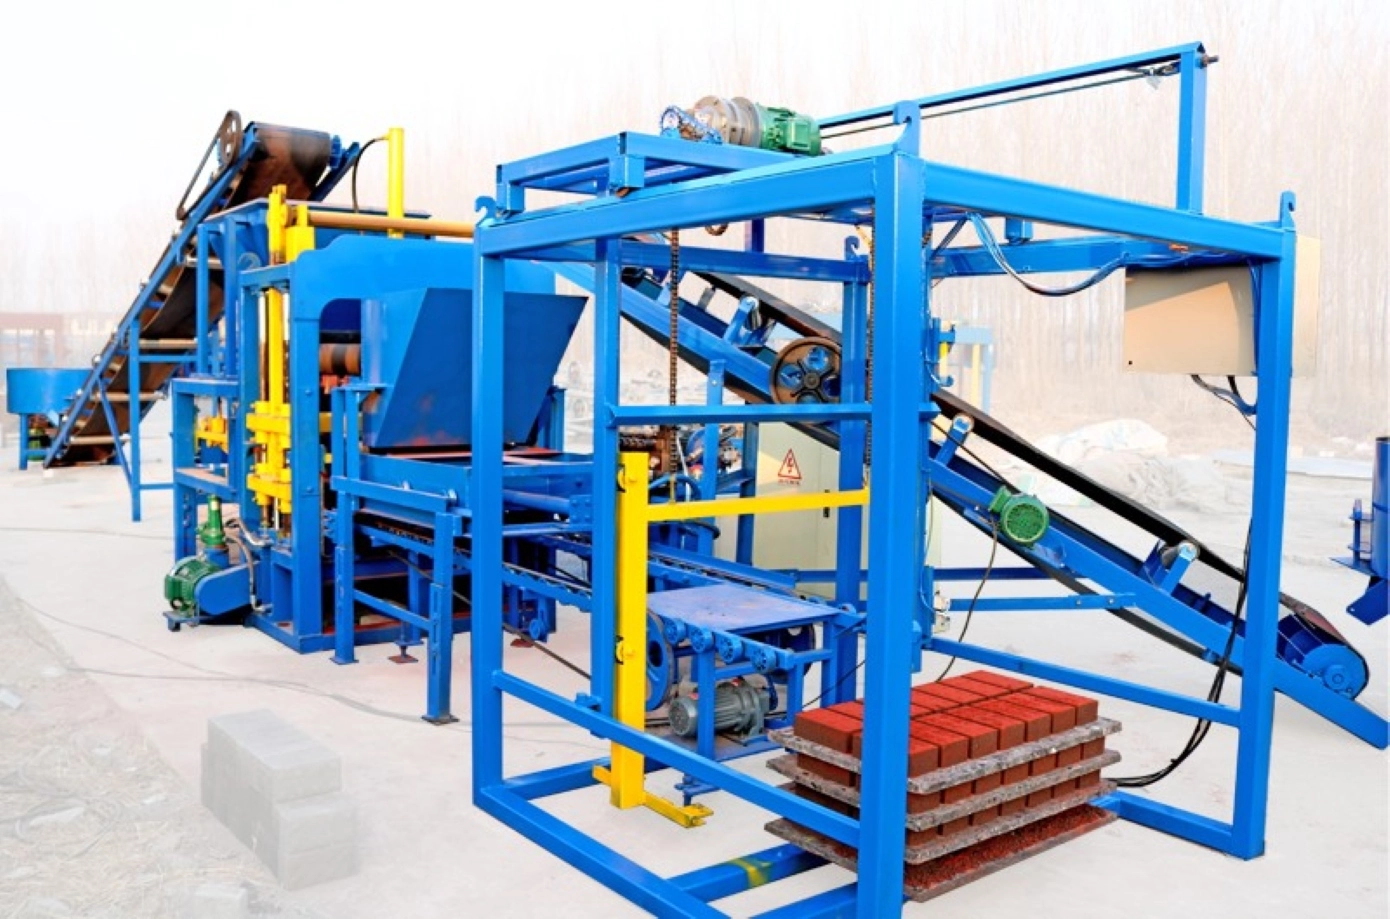
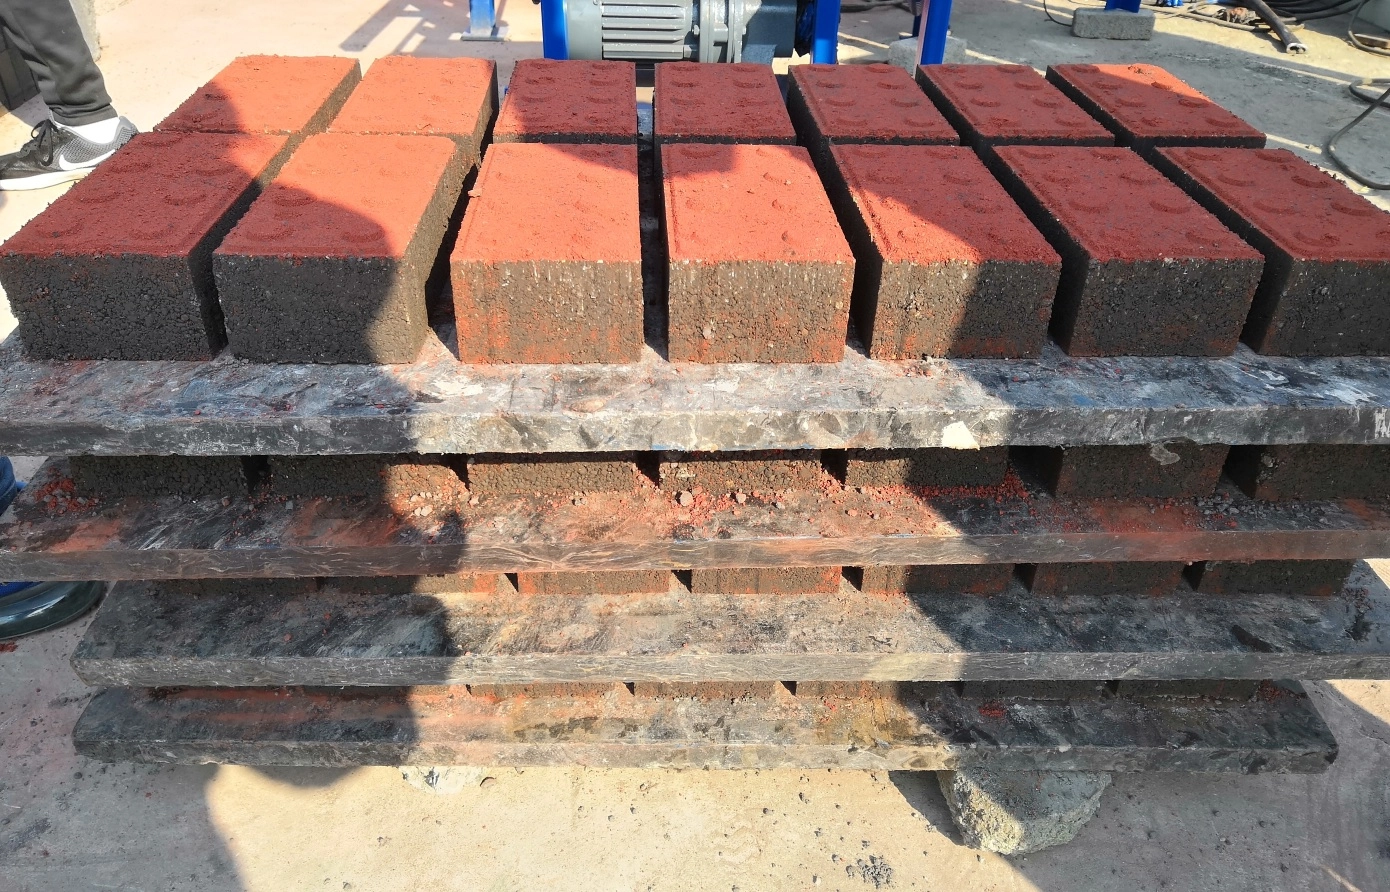
Green bricks from some brick machines are too weak for stacking. They must be laid in single layers, requiring large number of workers for handling and transporting. Breakage happens frequently during manual transfer and wastes raw materials. QT4‑15S combines table vibration and hydraulic compression. Fresh demoulded green solid bricks obtain good compactness and hardness, which allows direct multi‑layer stacking instead of single‑layer placement. When matched with automatic block stacker, bricks get stacked automatically right after demoulding. Manual brick‑handling positions are largely reduced, labor cost drops and reject rate caused by transportation collision goes down.
5. Broad raw‑material adaptability, utilize local industrial residues, get free from high‑cost aggregate shortage and flexibly control per‑brick profit
In some regions high‑quality sand and gravel are expensive, squeezing profit margin if you only use virgin aggregates for solid bricks. QT4‑15S accepts diversified feedstock. Besides standard cement‑sand‑stone formula, fly ash, steel slag, tailings sand and crushed construction waste can be properly blended for solid‑brick manufacturing. You can make use of locally‑available industrial residues, some of which can be obtained at zero or low cost. Your dependence on pricey commercial aggregates decreases. You can adjust recipes according to local material prices and preserve profit even under volatile building‑material market conditions.
6. Modular component solution, host‑only purchase available for phased plant expansion, fit multi‑stage capital budget
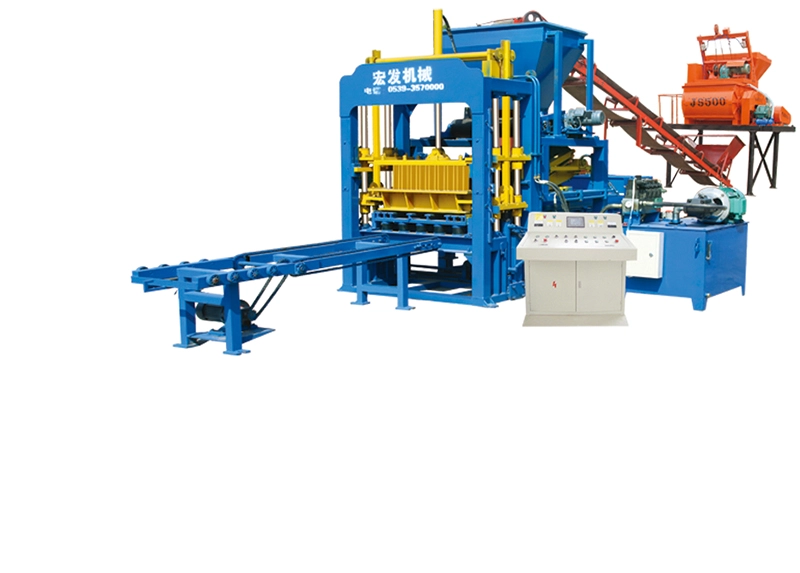
Many overseas investors build brick factories step‑by‑step. They want to start production with main forming unit first and add mixers, batching units and stackers later after generating revenue. However, many suppliers force full‑set purchase only. QT4‑15S supports modular configuration. The core forming host can be delivered and operated independently. Later you may add JS500 twin‑shaft mixer, PLD800 batching machine, color feeder, automatic stacker, cement silo and other accessories as budget allows. Investors can upgrade their plant progressively without paying full‑set cost upfront. It lowers initial capital pressure and enables new entrants to start solid‑brick business with limited funds.
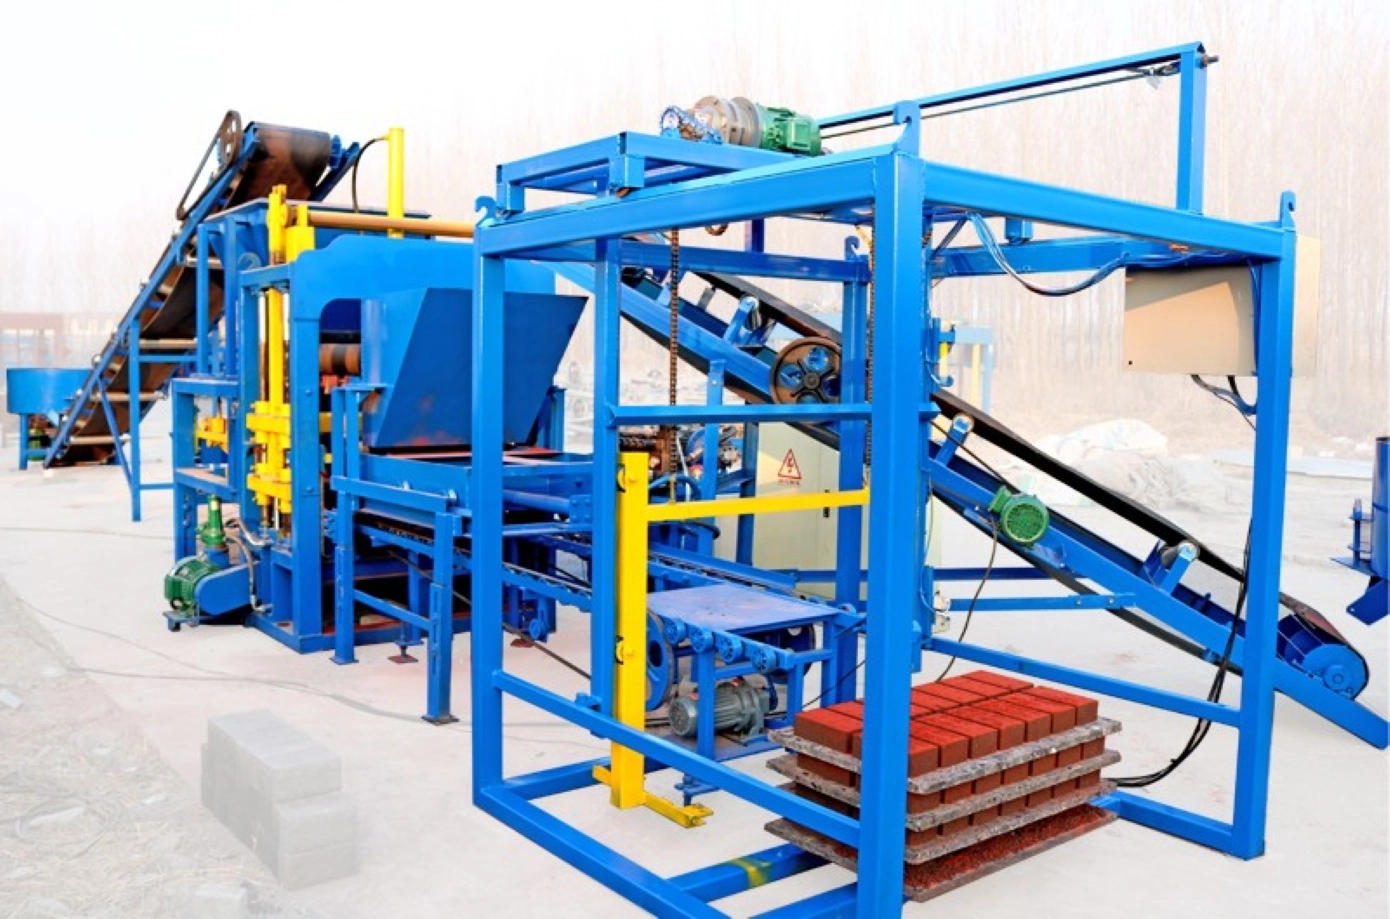
1. Compact small‑pallet design, lower consumable cost for solid‑brick production in space‑limited workshops
Many small overseas brick factories are restricted by workshop size. Large‑pallet brick machines demand bigger buildings and bring high ongoing pallet‑replacement expense, since pallets are wearing parts. QT4‑15S uses economical 900×550 mm pallets. It delivers 21 standard solid bricks per mould and outputs 35000‑40000 solid bricks per 8‑hour shift without large‑size workshop. Pallet purchasing and replacement cost is kept low, and alternative pallet materials are easier to source locally. You can launch solid‑brick mass‑production inside existing plant space, cutting civil‑work and consumable investment for new or space‑constrained investors.
2. Isolated vibration‑box drive structure, solve high‑frequency motor burnout risk in solid‑brick mass‑production and reduce unplanned‑shutdown loss
Solid‑brick production runs under continuous heavy vibration. Traditional direct‑motor‑driven machines make motors vibrate together with mould assembly. Motors burn out frequently during long‑hour solid‑brick manufacturing. Once motors fail, the whole line stops. For overseas buyers, spare‑part lead time is long and may cause contract penalties. QT4‑15S applies independent enclosed vibration‑box to transmit exciting force. Motors are physically separated from vibration source and free from heavy oscillation, drastically lowering burnout risk. 16‑MPa hydraulic pressure together with 55‑KN exciting force guarantees thorough compaction for every solid brick. It cuts time‑cost of overseas spare‑part procurement and secures on‑time delivery for large‑volume solid‑brick contracts.
3. Native compatibility with color‑facing system, one line handles main solid‑brick orders plus occasional municipal paver jobs to boost machine utilization
Most brick factories rely heavily on solid‑brick orders while receiving sporadic municipal paver tenders. Without built‑in support for color facing material, you either reject those orders or invest in a second idle machine. QT4‑15S reserves mechanical interface for optional color feeder. You can run high‑volume solid‑brick production as core business. When paver orders arrive, enable the color‑facing module without major host modification to produce colored paving blocks. One single production line absorbs two types of business, improves machine running rate and avoids extra heavy equipment investment for small‑batch paver demands.
4. High green‑brick strength after molding, permit direct multi‑layer stacking, less brick breakage and lower manual stacking workload
Green bricks from some brick machines are too weak for stacking. They must be laid in single layers, requiring large number of workers for handling and transporting. Breakage happens frequently during manual transfer and wastes raw materials. QT4‑15S combines table vibration and hydraulic compression. Fresh demoulded green solid bricks obtain good compactness and hardness, which allows direct multi‑layer stacking instead of single‑layer placement. When matched with automatic block stacker, bricks get stacked automatically right after demoulding. Manual brick‑handling positions are largely reduced, labor cost drops and reject rate caused by transportation collision goes down.
5. Broad raw‑material adaptability, utilize local industrial residues, get free from high‑cost aggregate shortage and flexibly control per‑brick profit
In some regions high‑quality sand and gravel are expensive, squeezing profit margin if you only use virgin aggregates for solid bricks. QT4‑15S accepts diversified feedstock. Besides standard cement‑sand‑stone formula, fly ash, steel slag, tailings sand and crushed construction waste can be properly blended for solid‑brick manufacturing. You can make use of locally‑available industrial residues, some of which can be obtained at zero or low cost. Your dependence on pricey commercial aggregates decreases. You can adjust recipes according to local material prices and preserve profit even under volatile building‑material market conditions.
6. Modular component solution, host‑only purchase available for phased plant expansion, fit multi‑stage capital budget
Many overseas investors build brick factories step‑by‑step. They want to start production with main forming unit first and add mixers, batching units and stackers later after generating revenue. However, many suppliers force full‑set purchase only. QT4‑15S supports modular configuration. The core forming host can be delivered and operated independently. Later you may add JS500 twin‑shaft mixer, PLD800 batching machine, color feeder, automatic stacker, cement silo and other accessories as budget allows. Investors can upgrade their plant progressively without paying full‑set cost upfront. It lowers initial capital pressure and enables new entrants to start solid‑brick business with limited funds.
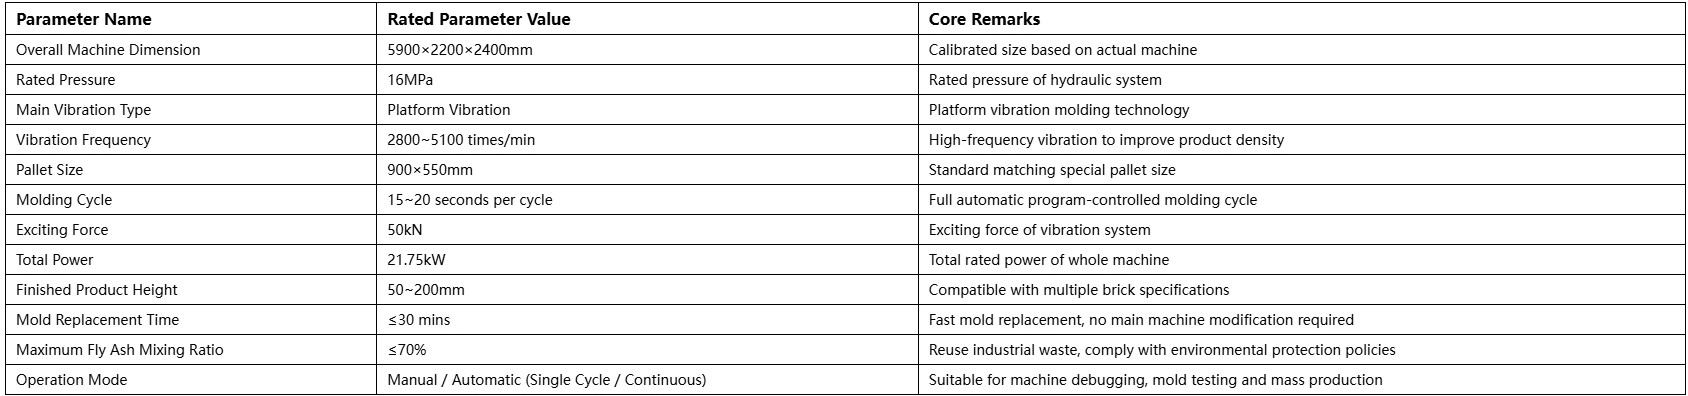
 QT4‑25 Fully‑Automatic Paving Brick Making Machine | Table‑Mold Resonance Line for Color Paver
Hongfa QT4‑25 fully‑automatic paving brick forming machine adopts table‑mold resonance and dual‑side compression, specia...
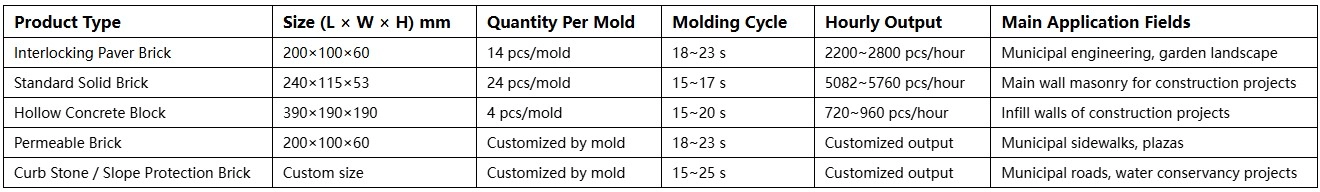
 QT4‑25C Automatic Brick Making Machine | High‑output Forming Equipment For Concrete Hollow Blocks
QT4‑25C automatic brick making main machine is optimized for mass‑production of standard 390×190×190 mm hollow blocks. I...
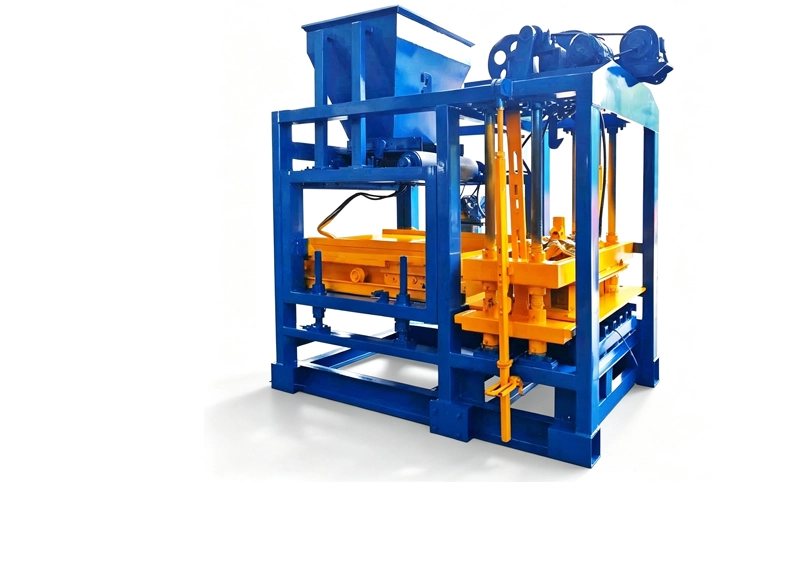
QT4‑25C Automatic Concrete Brick Making Machine
QT4‑25C automatic concrete brick making main machine adopts combined table‑and‑mold vibration with 25‑second molding cyc...
Shandong Hongfa Scientific Industrial&Trading Co.,Ltd ©️2026Copyright © LU ICP B 16041216-4