1. Frequency‑synchronized table‑vibration forming delivers high‑density load‑bearing blocks for stable third‑party sampling‑test pass for key projects
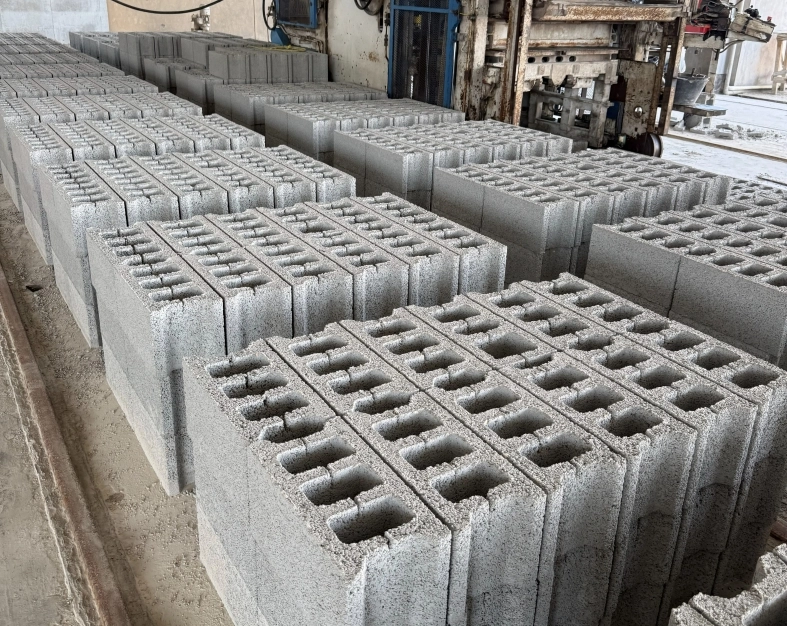
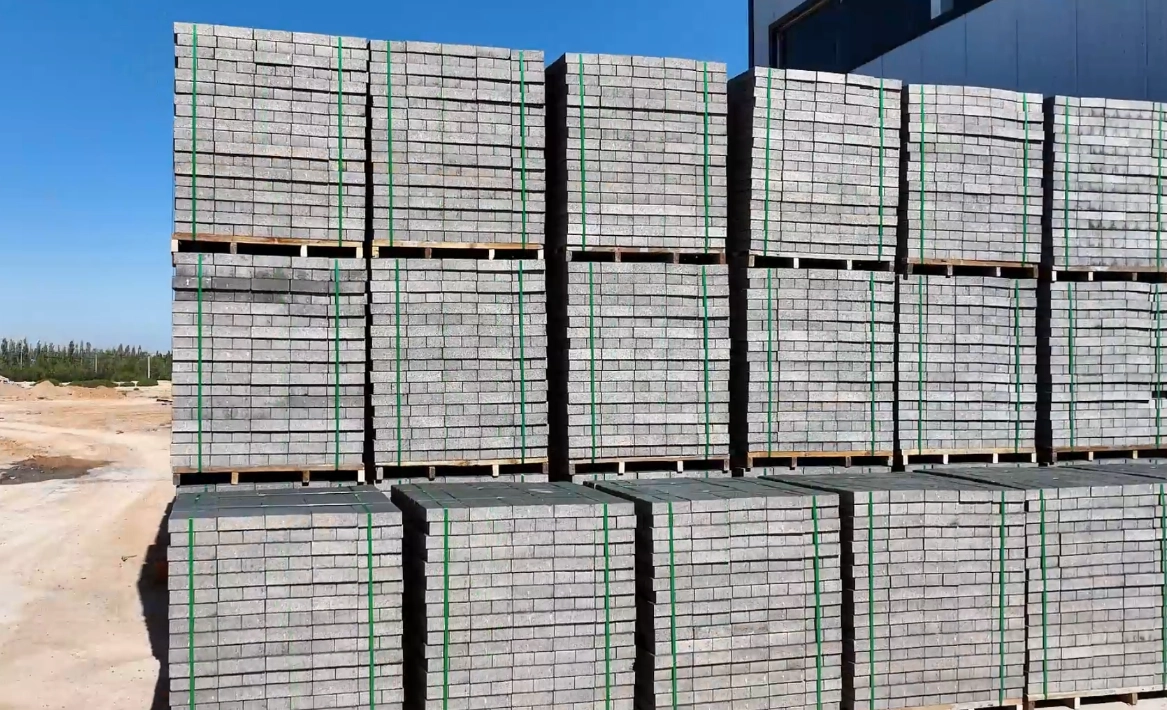
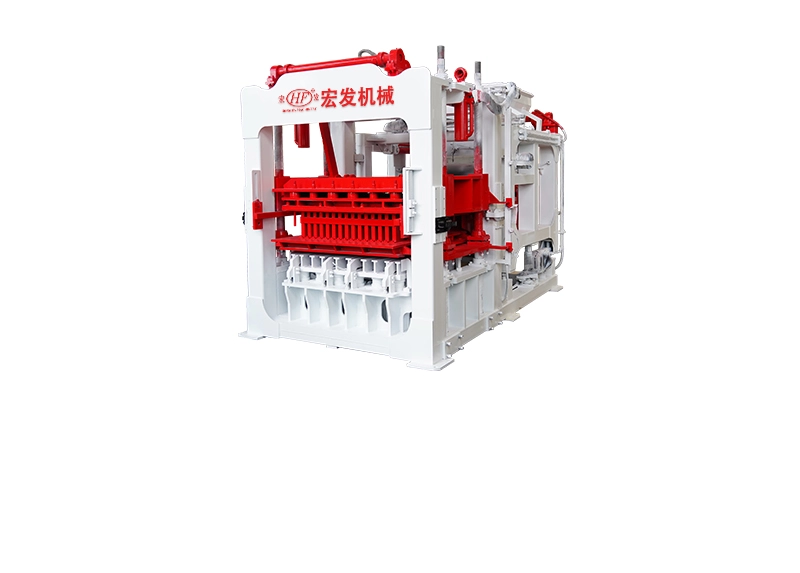
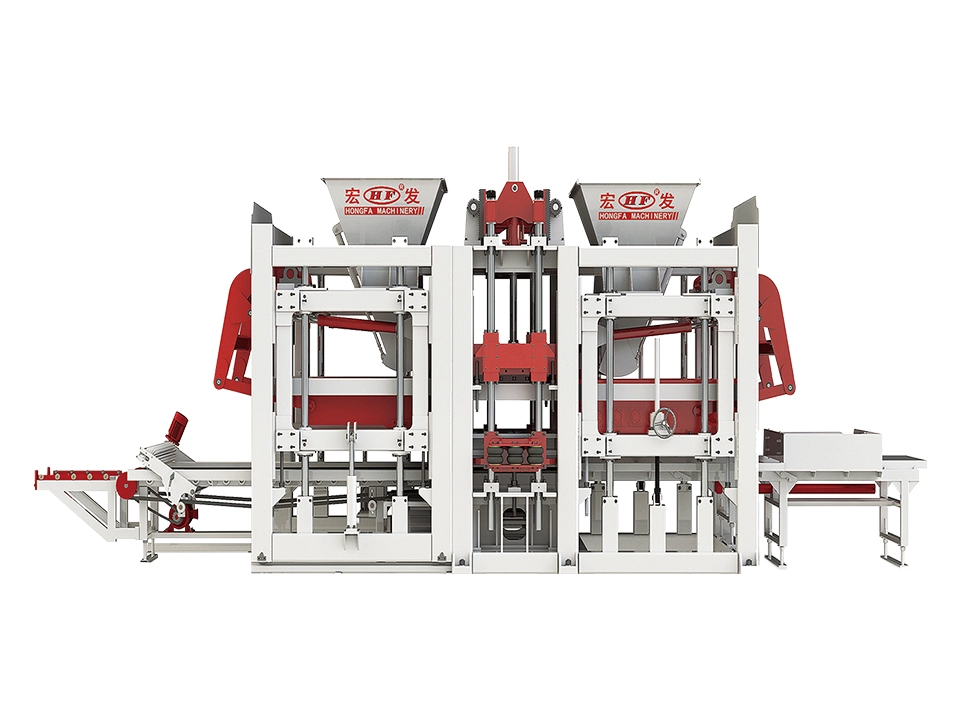
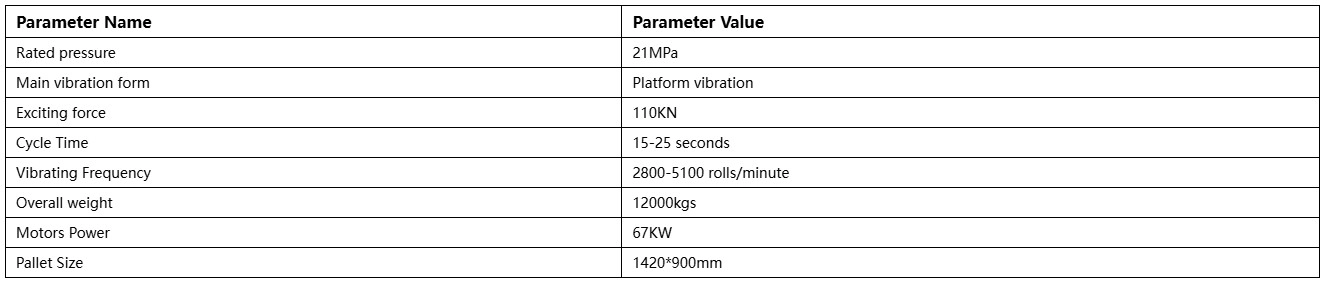
QT12‑15F forming main machine adopts adjustable frequency‑synchronized table‑vibration system, applying low‑frequency for material feeding and high‑frequency for pressing vibration. Vibration parameters can be adjusted flexibly according to sand‑stone, fly ash, mineral slag and other raw‑material conditions. Aggregate particles interlock sufficiently and internal air voids are fully expelled to eliminate inner defects such as interlayer and partial looseness. Finished blocks feature high compactness and compressive performance meeting hard indicators for high‑rise housing and large‑scale infrastructure projects. Many brick suppliers bidding for large‑scale projects encounter that lab‑test samples pass inspection but compressive strength drifts in mass‑produced goods, resulting in removal from approved‑vendor lists and loss of high‑value large‑volume supply orders. Benefiting from electro‑mechanical‑hydraulic coordinated control of QT12‑15F, quality deviation among batches stays at a very low level. Test samples maintain high performance consistency with bulk blocks delivered to construction sites. Whether for super high‑rise residential buildings, main load‑bearing walls of large industrial parks or provincial‑level and national municipal infrastructure wall projects, it enables you to pass strict sampling inspections smoothly and obtain long‑term high‑volume supply qualification. No repeated material‑consuming sample modification is required, material loss from trial‑production gets reduced, and your core competitiveness for high‑rise project bidding gets greatly improved.
2. Heavy‑duty reinforced frame with imported Rexroth hydraulics guarantees dimensional uniformity under long‑hour full‑load production and mitigates compensation risks for mega‑volume orders
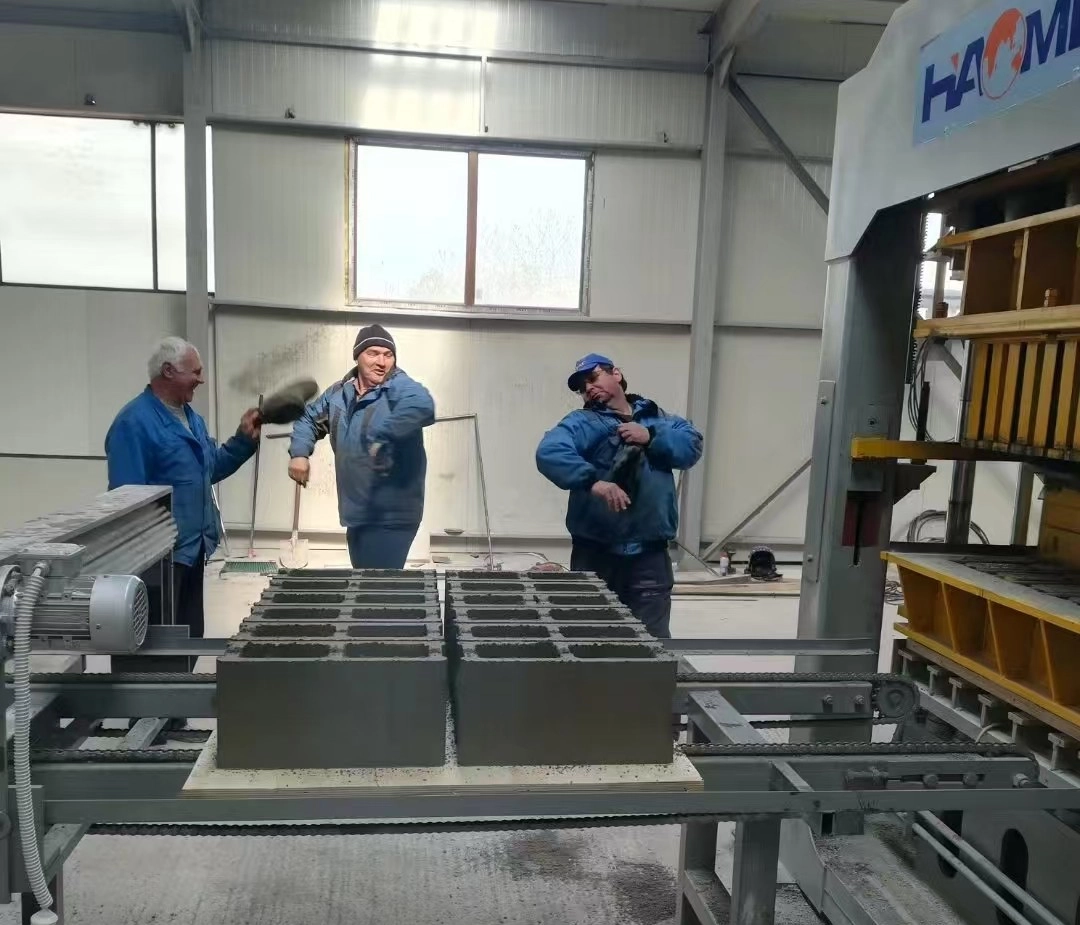
The main machine is built with heavy‑duty thickened frame welded from high‑quality section steel supplied by Laigang and Jigang, equipped with Germany Rexroth hydraulic unit for high integral rigidity. It adapts to long‑term non‑stop full‑load continuous production. Even under sustained heavy‑load operation, every block on each pallet maintains uniform thickness and outer dimension. It minimizes defective products with chipped edges, inner looseness, insufficient strength or dimensional deviation from entering supply chains. Supply contracts for high‑rise and national key‑infrastructure contain binding quality‑liability clauses. Once delivered blocks fail random inspection, on‑site wall construction will be fully suspended, resulting in shipment rejection, heavy payment deduction and even contractual compensation. A single quality incident may wipe out full‑project profit and leave negative reputation across national engineering supplier circles, making it hard to win benchmark projects afterwards. Reliable heavy‑duty forming performance of QT12‑15F lowers defect rate from source and avoids hidden quality disputes in bulk supply. It protects your project profit margin, sustains long‑term trusted cooperation with large general contractors and clients, and cuts manpower and time cost for after‑sales communication and on‑site rectification.
3. Broad raw‑material compatibility plus fast‑change carburizing manganese‑steel moulds for diversified high‑rise‑grade structural‑block production
This heavy‑duty main machine features excellent raw‑material adaptability. High‑strength structural blocks meeting high‑rise wall standards can be produced with high proportion of industrial waste including fly ash, mineral slag and steel slag mixed with sand and cement. While fully meeting all performance requirements for load‑bearing walls, it helps extra‑large‑scale brick plants cut comprehensive raw‑material procurement cost under mass‑production conditions. Carburizing heat‑treated manganese‑steel moulds can be swapped quickly without modifying main‑machine structure to produce various sizes of solid and hollow structural blocks for high‑rise buildings, precisely matching technical procurement terms in tender documents of different high‑rise housing and large infrastructure projects. Many ordinary block machines cannot steadily mass‑produce blocks satisfying strict strength thresholds for high‑rise walls. With QT12‑15F forming machine, brick plants can step into high‑threshold high‑margin high‑rise and large‑infrastructure wall‑supply market, escape fierce low‑price competition of ordinary building materials, serve large general contractors with rigid compression requirements and capture mega‑volume wall‑supply business opportunities to lift upper limit of engineering‑oriented revenue.
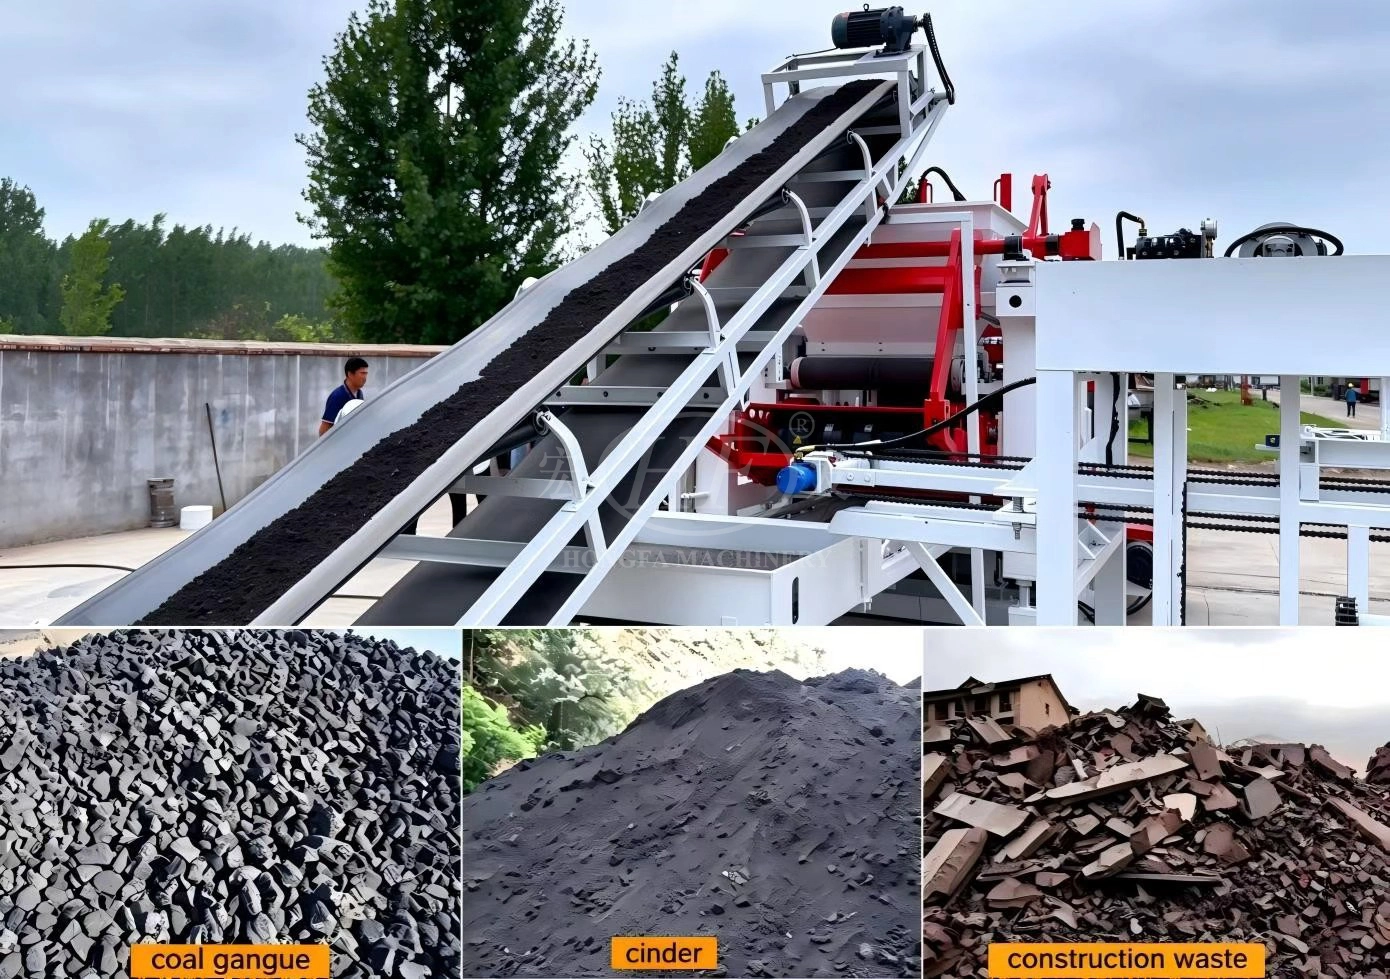
4. Complete SIEMENS intelligent electric control for energy‑saving full‑automatic closed‑loop workflow meets urgent mega‑volume supply demands during high‑rise project rush‑construction phase
Equipped with SIEMENS PLC and touch‑screen HMI, the full workflow including pallet feeding, material distributing, frequency‑conversion pre‑vibration, main vibration‑pressing, demolding and block discharging runs fully‑automatically in closed‑loop mode. Frequency‑conversion motors realize notable energy saving compared with peer equipment, together with interlock logic for heavy‑load working conditions. It supports round‑the‑clock non‑stop full‑load mass‑production and steadily outputs high‑compressive structural blocks complying with high‑rise engineering standards. High‑rise housing and large‑scale infrastructure projects have tight construction cycles, and urgent mega‑volume procurement demands often occur during rush‑construction windows. Some block machines suffer quality degradation and delivery delay after long‑hour heavy‑load operation, which leads to contract breach and lost orders. QT12‑15F main machine handles emergency mega‑volume supply orders from general contractors efficiently. Stable full‑load large‑scale production guarantees on‑time full‑quantity delivery without delaying on‑site wall construction progress. Superior block quality together with stable delivery performance makes you a preferred tender candidate for new projects from large construction clients. You can continuously accumulate high‑value benchmark engineering clients.
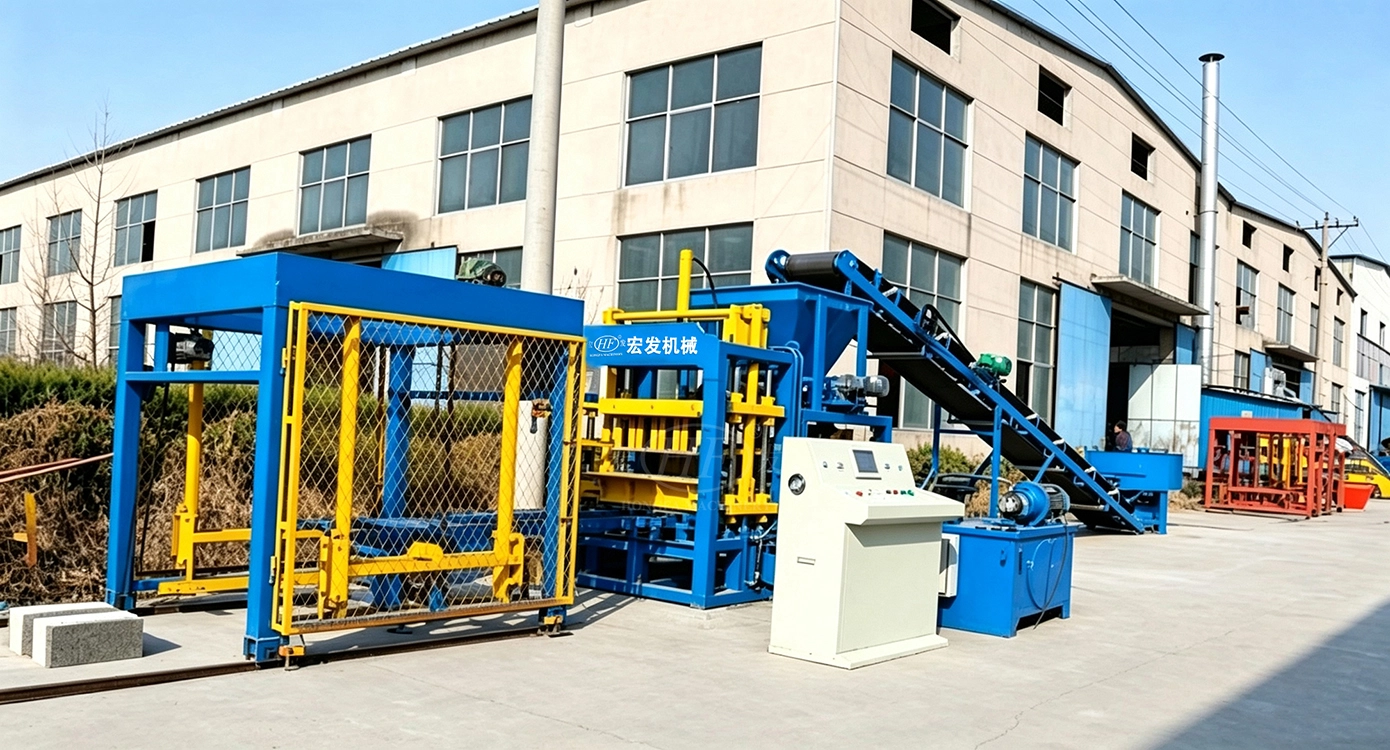
5. Synchronized multi‑block full‑pallet demolding optimizes palletizing workflow and enables parallel supply for multiple super‑large projects
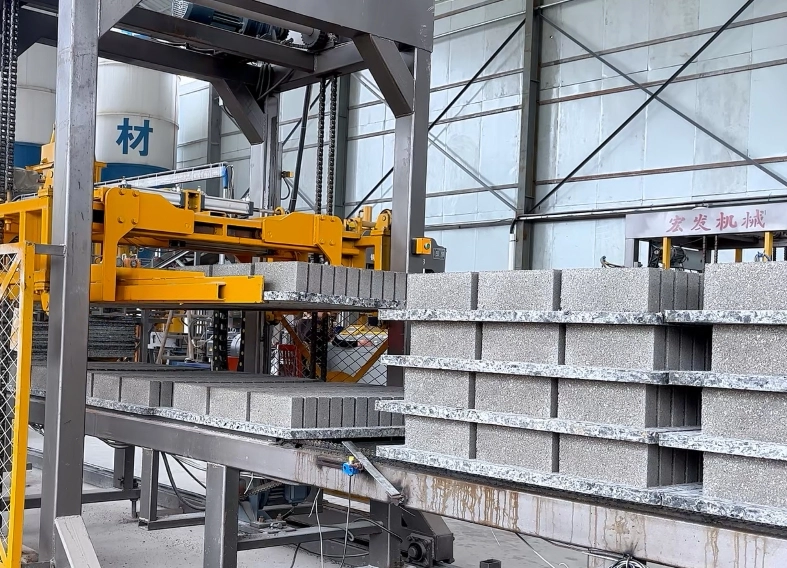
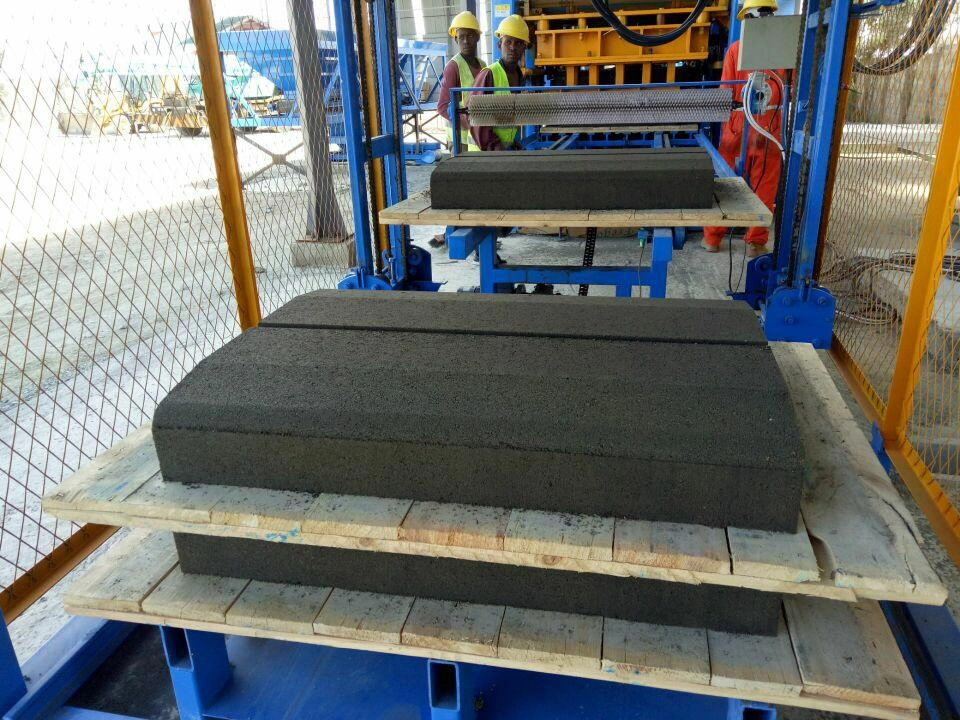
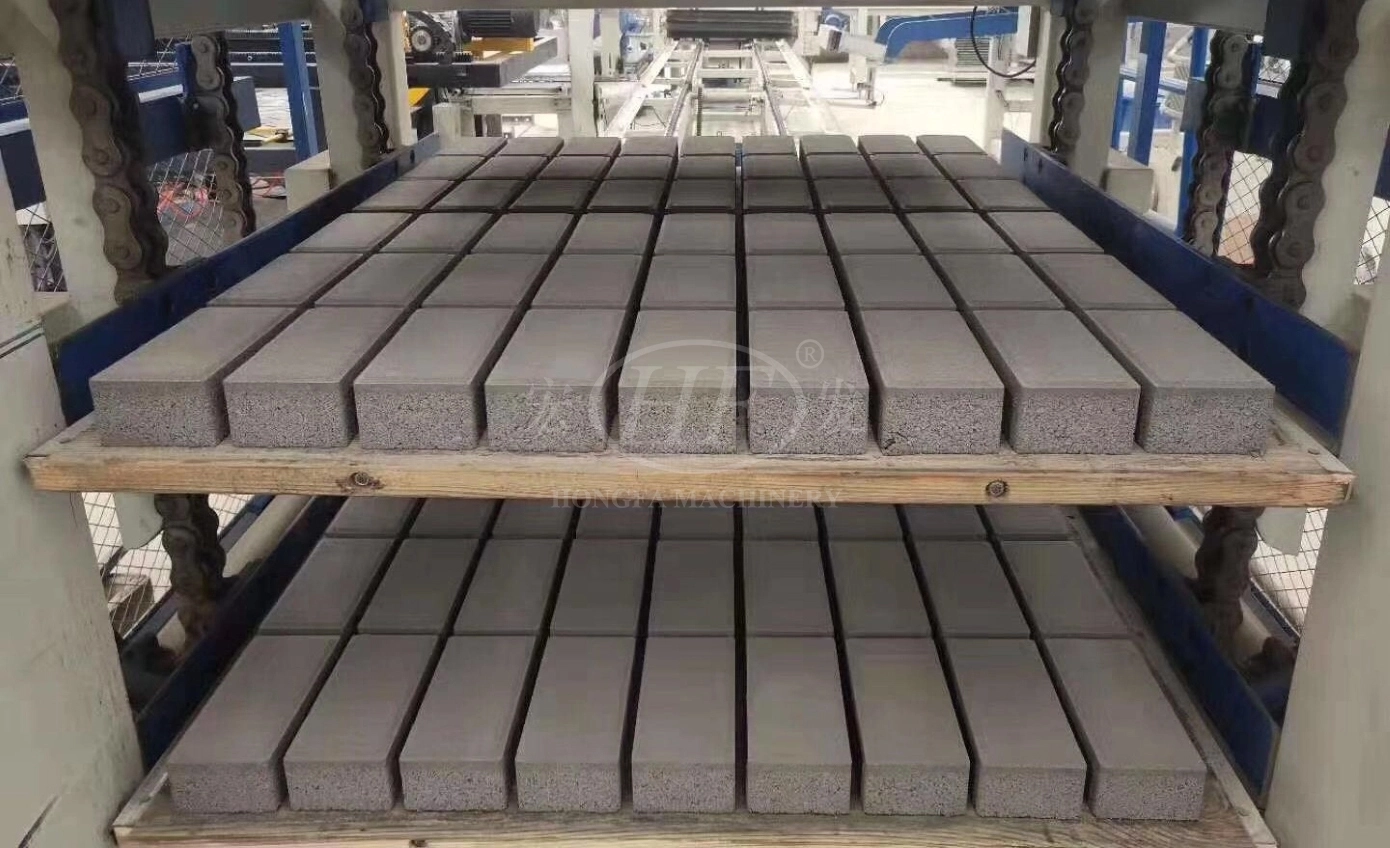
Multiple blocks get demolded simultaneously in one cycle to realize full‑pallet output. Fresh‑formed blocks are discharged with pallets for centralized handling and palletizing, lowering collision damage during transfer and improving overall production turnover efficiency. When undertaking several mega‑volume high‑rise wall‑supply contracts at the same time, higher turnover allows you to produce more qualified high‑rise‑grade structural blocks within the same cycle and accelerates stock preparation for concurrent super‑large projects. Efficient full‑pallet output connects seamlessly with downstream palletizing, transferring and loading procedures and improves intact rate of blocks delivered to various large construction sites. When handling multiple mega‑volume supply contracts, you gain stronger business flexibility and further enhance comprehensive competitiveness of extra‑large‑scale brick plants in high‑rise engineering‑material supply market.
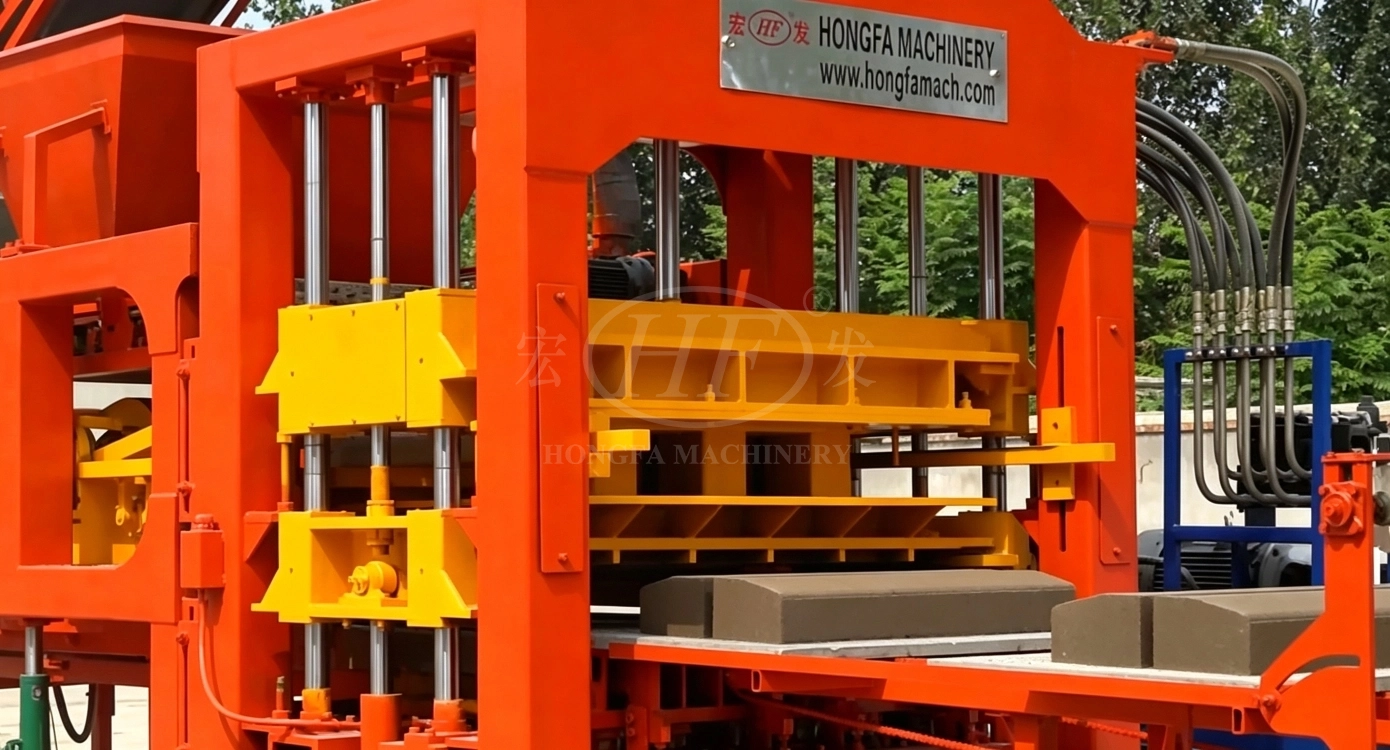
1. Frequency‑synchronized table‑vibration forming delivers high‑density load‑bearing blocks for stable third‑party sampling‑test pass for key projects
QT12‑15F forming main machine adopts adjustable frequency‑synchronized table‑vibration system, applying low‑frequency for material feeding and high‑frequency for pressing vibration. Vibration parameters can be adjusted flexibly according to sand‑stone, fly ash, mineral slag and other raw‑material conditions. Aggregate particles interlock sufficiently and internal air voids are fully expelled to eliminate inner defects such as interlayer and partial looseness. Finished blocks feature high compactness and compressive performance meeting hard indicators for high‑rise housing and large‑scale infrastructure projects. Many brick suppliers bidding for large‑scale projects encounter that lab‑test samples pass inspection but compressive strength drifts in mass‑produced goods, resulting in removal from approved‑vendor lists and loss of high‑value large‑volume supply orders. Benefiting from electro‑mechanical‑hydraulic coordinated control of QT12‑15F, quality deviation among batches stays at a very low level. Test samples maintain high performance consistency with bulk blocks delivered to construction sites. Whether for super high‑rise residential buildings, main load‑bearing walls of large industrial parks or provincial‑level and national municipal infrastructure wall projects, it enables you to pass strict sampling inspections smoothly and obtain long‑term high‑volume supply qualification. No repeated material‑consuming sample modification is required, material loss from trial‑production gets reduced, and your core competitiveness for high‑rise project bidding gets greatly improved.
2. Heavy‑duty reinforced frame with imported Rexroth hydraulics guarantees dimensional uniformity under long‑hour full‑load production and mitigates compensation risks for mega‑volume orders
The main machine is built with heavy‑duty thickened frame welded from high‑quality section steel supplied by Laigang and Jigang, equipped with Germany Rexroth hydraulic unit for high integral rigidity. It adapts to long‑term non‑stop full‑load continuous production. Even under sustained heavy‑load operation, every block on each pallet maintains uniform thickness and outer dimension. It minimizes defective products with chipped edges, inner looseness, insufficient strength or dimensional deviation from entering supply chains. Supply contracts for high‑rise and national key‑infrastructure contain binding quality‑liability clauses. Once delivered blocks fail random inspection, on‑site wall construction will be fully suspended, resulting in shipment rejection, heavy payment deduction and even contractual compensation. A single quality incident may wipe out full‑project profit and leave negative reputation across national engineering supplier circles, making it hard to win benchmark projects afterwards. Reliable heavy‑duty forming performance of QT12‑15F lowers defect rate from source and avoids hidden quality disputes in bulk supply. It protects your project profit margin, sustains long‑term trusted cooperation with large general contractors and clients, and cuts manpower and time cost for after‑sales communication and on‑site rectification.
3. Broad raw‑material compatibility plus fast‑change carburizing manganese‑steel moulds for diversified high‑rise‑grade structural‑block production
This heavy‑duty main machine features excellent raw‑material adaptability. High‑strength structural blocks meeting high‑rise wall standards can be produced with high proportion of industrial waste including fly ash, mineral slag and steel slag mixed with sand and cement. While fully meeting all performance requirements for load‑bearing walls, it helps extra‑large‑scale brick plants cut comprehensive raw‑material procurement cost under mass‑production conditions. Carburizing heat‑treated manganese‑steel moulds can be swapped quickly without modifying main‑machine structure to produce various sizes of solid and hollow structural blocks for high‑rise buildings, precisely matching technical procurement terms in tender documents of different high‑rise housing and large infrastructure projects. Many ordinary block machines cannot steadily mass‑produce blocks satisfying strict strength thresholds for high‑rise walls. With QT12‑15F forming machine, brick plants can step into high‑threshold high‑margin high‑rise and large‑infrastructure wall‑supply market, escape fierce low‑price competition of ordinary building materials, serve large general contractors with rigid compression requirements and capture mega‑volume wall‑supply business opportunities to lift upper limit of engineering‑oriented revenue.
4. Complete SIEMENS intelligent electric control for energy‑saving full‑automatic closed‑loop workflow meets urgent mega‑volume supply demands during high‑rise project rush‑construction phase
Equipped with SIEMENS PLC and touch‑screen HMI, the full workflow including pallet feeding, material distributing, frequency‑conversion pre‑vibration, main vibration‑pressing, demolding and block discharging runs fully‑automatically in closed‑loop mode. Frequency‑conversion motors realize notable energy saving compared with peer equipment, together with interlock logic for heavy‑load working conditions. It supports round‑the‑clock non‑stop full‑load mass‑production and steadily outputs high‑compressive structural blocks complying with high‑rise engineering standards. High‑rise housing and large‑scale infrastructure projects have tight construction cycles, and urgent mega‑volume procurement demands often occur during rush‑construction windows. Some block machines suffer quality degradation and delivery delay after long‑hour heavy‑load operation, which leads to contract breach and lost orders. QT12‑15F main machine handles emergency mega‑volume supply orders from general contractors efficiently. Stable full‑load large‑scale production guarantees on‑time full‑quantity delivery without delaying on‑site wall construction progress. Superior block quality together with stable delivery performance makes you a preferred tender candidate for new projects from large construction clients. You can continuously accumulate high‑value benchmark engineering clients.
5. Synchronized multi‑block full‑pallet demolding optimizes palletizing workflow and enables parallel supply for multiple super‑large projects
Multiple blocks get demolded simultaneously in one cycle to realize full‑pallet output. Fresh‑formed blocks are discharged with pallets for centralized handling and palletizing, lowering collision damage during transfer and improving overall production turnover efficiency. When undertaking several mega‑volume high‑rise wall‑supply contracts at the same time, higher turnover allows you to produce more qualified high‑rise‑grade structural blocks within the same cycle and accelerates stock preparation for concurrent super‑large projects. Efficient full‑pallet output connects seamlessly with downstream palletizing, transferring and loading procedures and improves intact rate of blocks delivered to various large construction sites. When handling multiple mega‑volume supply contracts, you gain stronger business flexibility and further enhance comprehensive competitiveness of extra‑large‑scale brick plants in high‑rise engineering‑material supply market.
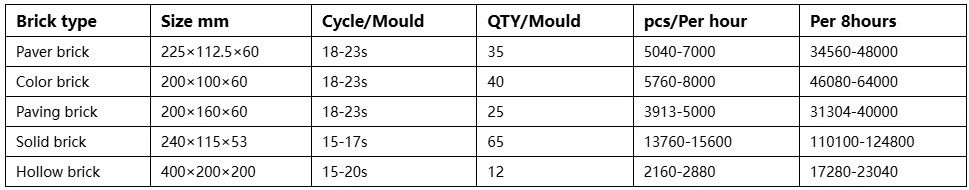
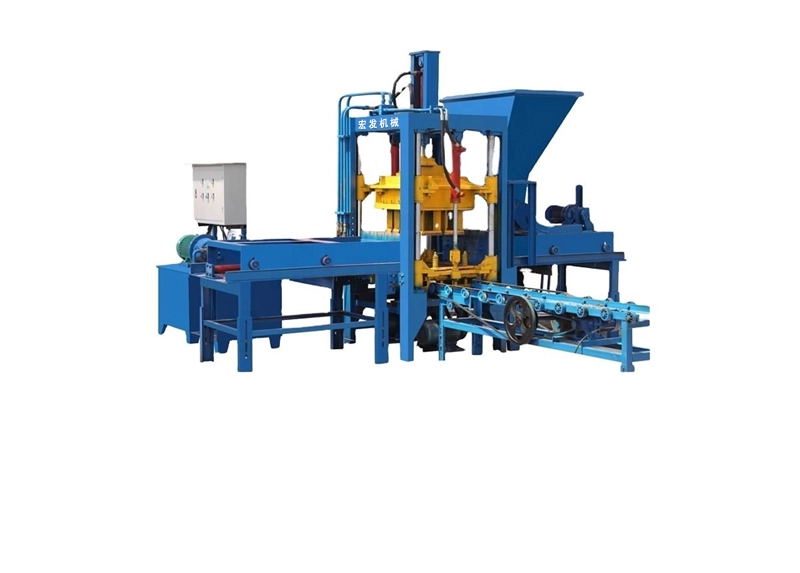 QTF3‑20 Full-automatic Brick Forming Machine | Load‑bearing Wall Brick Equipment For Medium‑small Brick Plants
QTF3‑20 automatic table‑vibration block forming main machine adopts box‑type table‑vibration excitation structure, Taiwa...

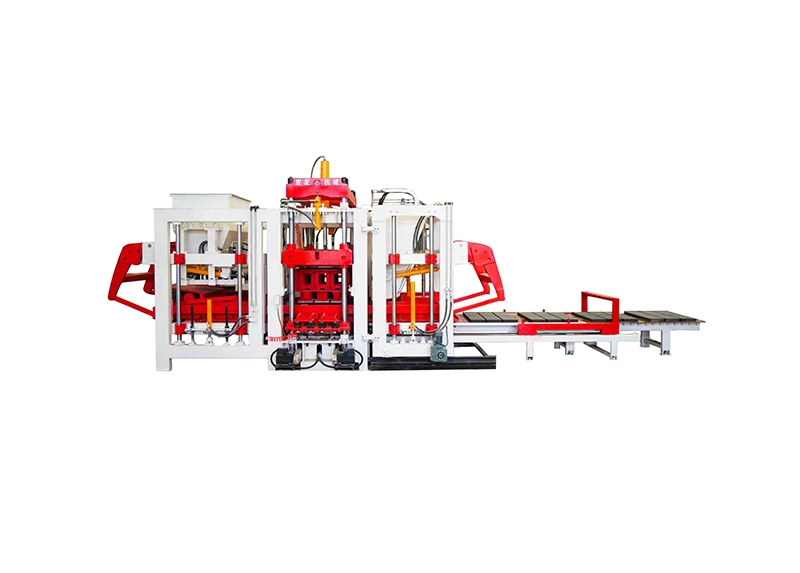 HF18 Brick Forming Machine | Extra‑large‑scale High‑compressive Structural‑wall Brick Manufacturing Equipment
HF18 full‑intelligent servo block forming main machine adopts servo‑driven vibration system, Vitos servo proportional hy...
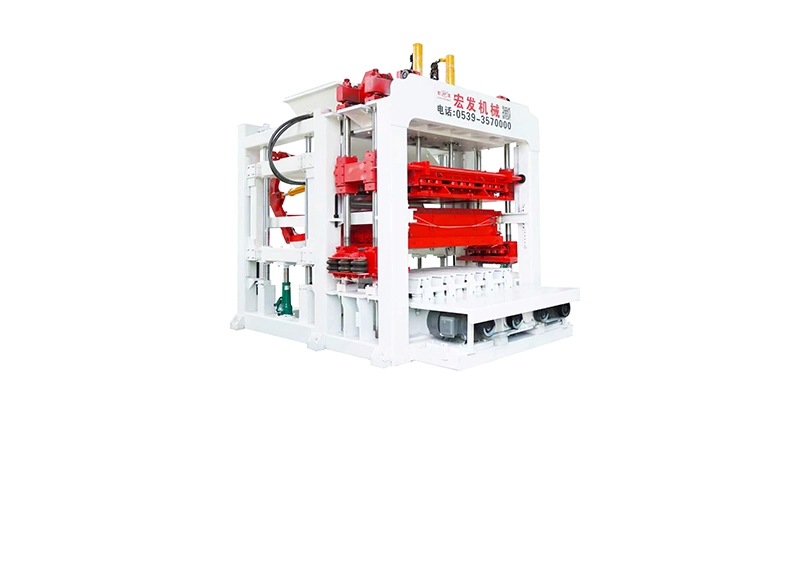 QT12‑15C Platform‑vibration Brick Machine | Engineering‑grade High‑compressive Structural‑wall Brick Equipment
QT12‑15C automatic platform‑vibration block forming main machine is equipped with frequency‑adjustable synchronized plat...
Shandong Hongfa Scientific Industrial&Trading Co.,Ltd ©️2026Copyright © LU ICP B 16041216-4