1. Non‑fired Forming for Large‑scale Solid‑waste Recycling With High‑spec Configuration
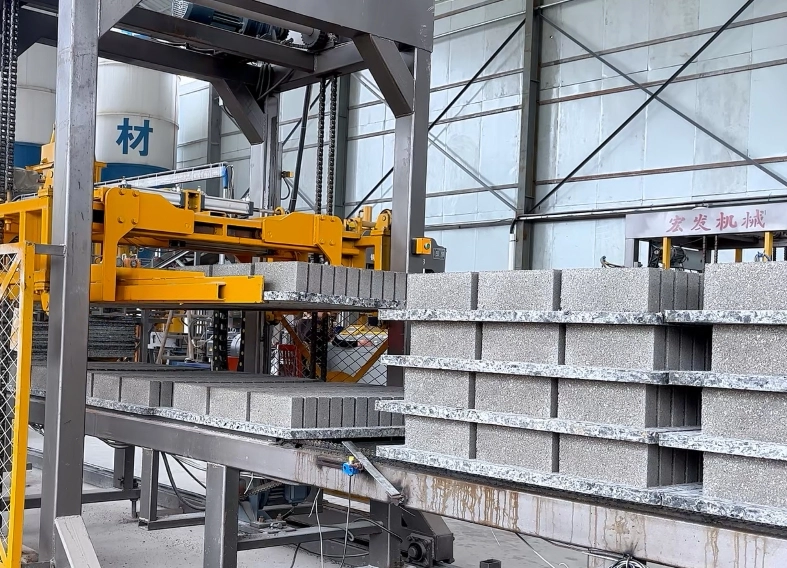
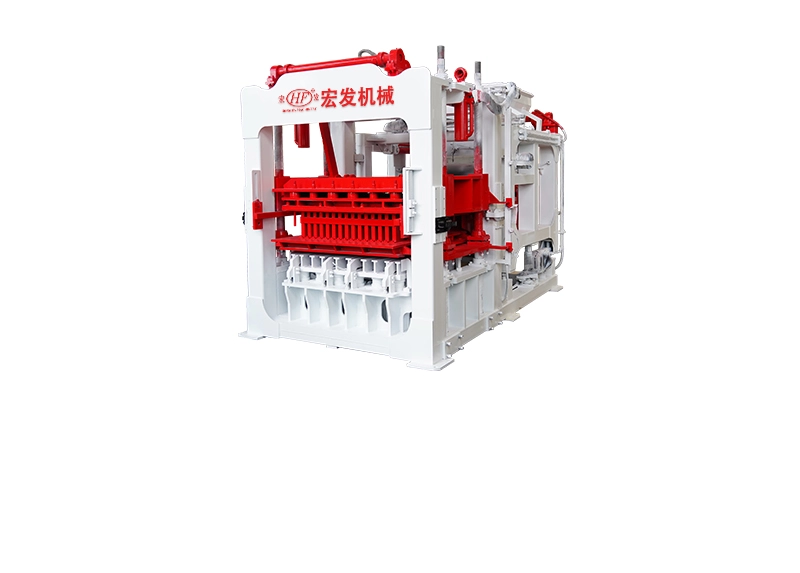
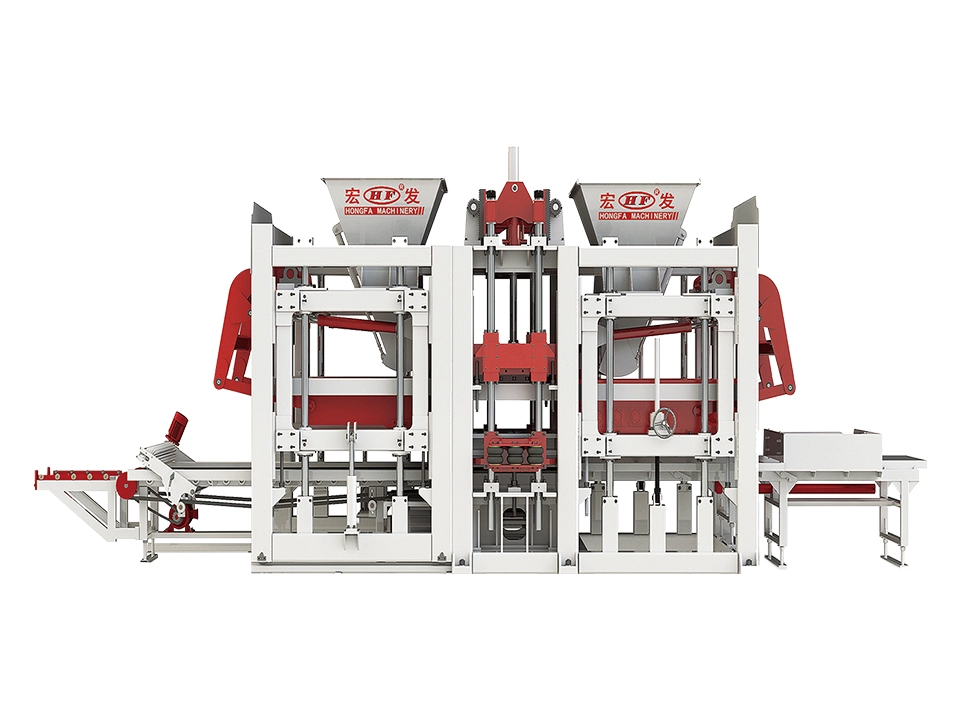
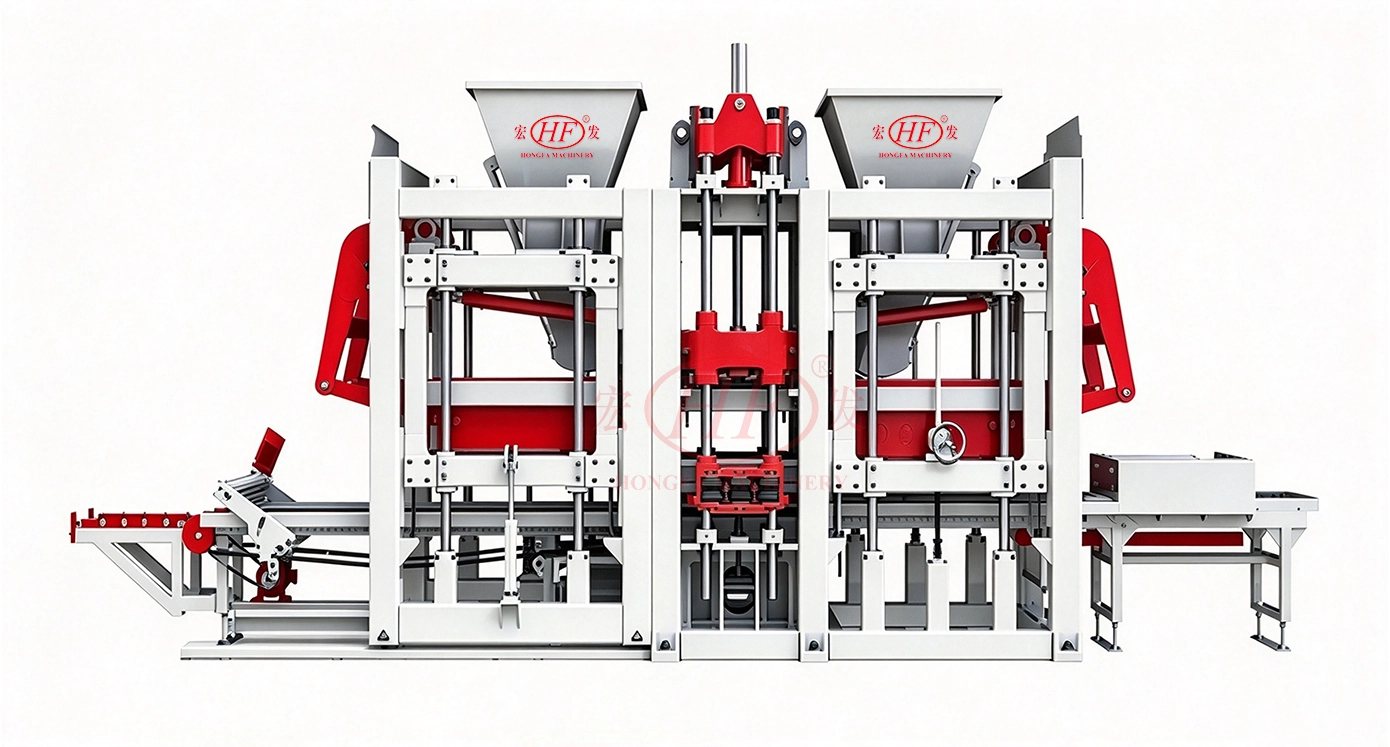
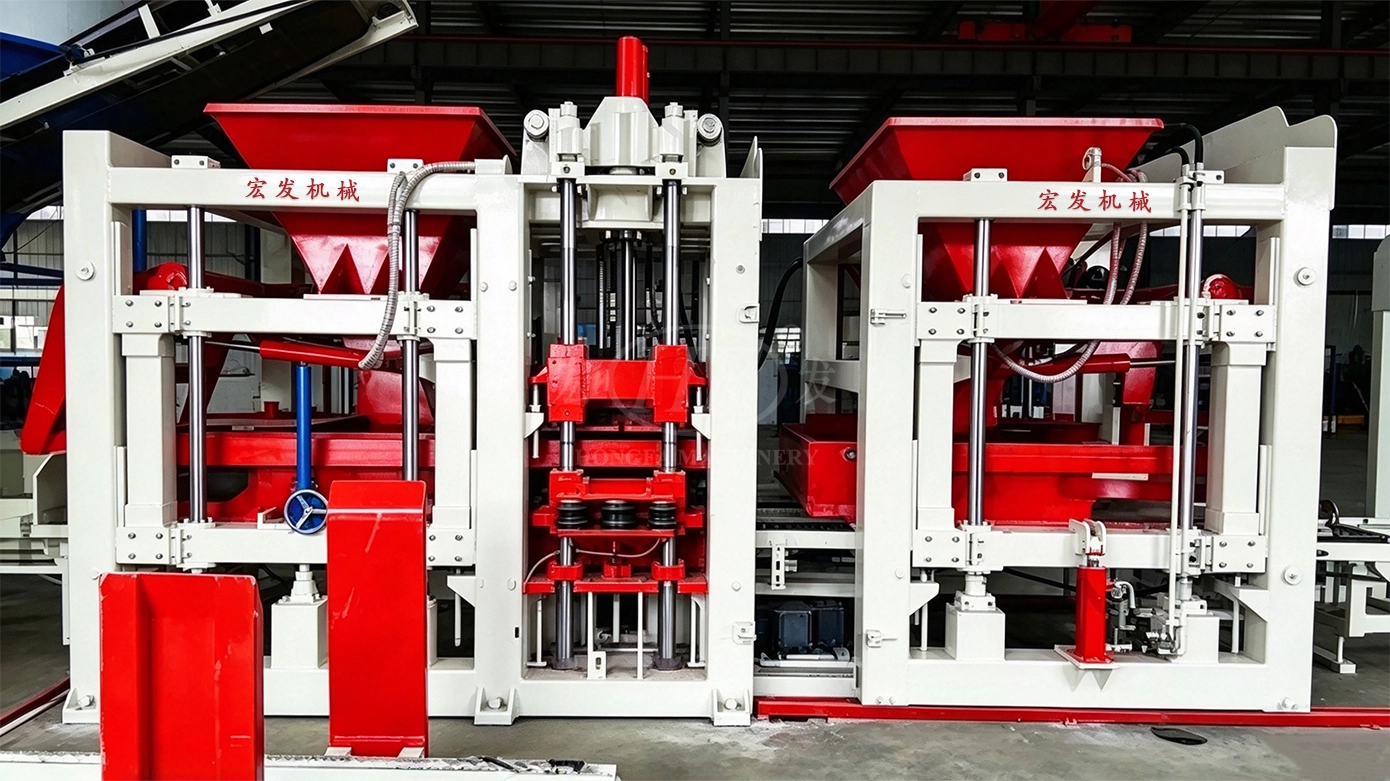
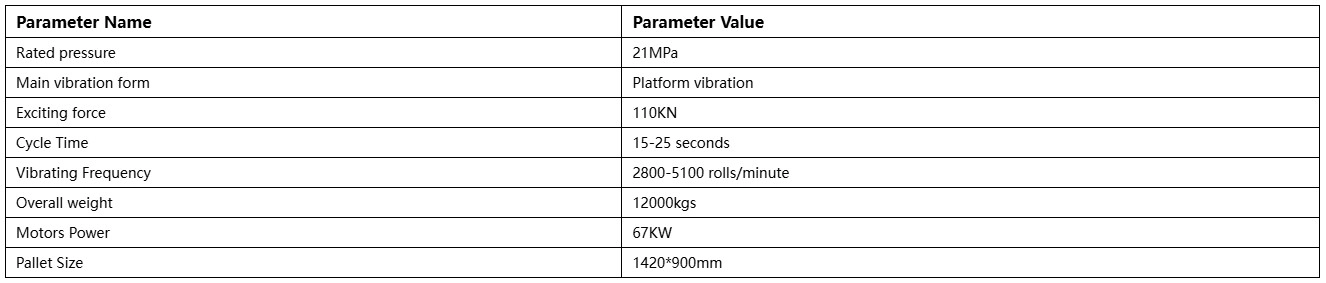
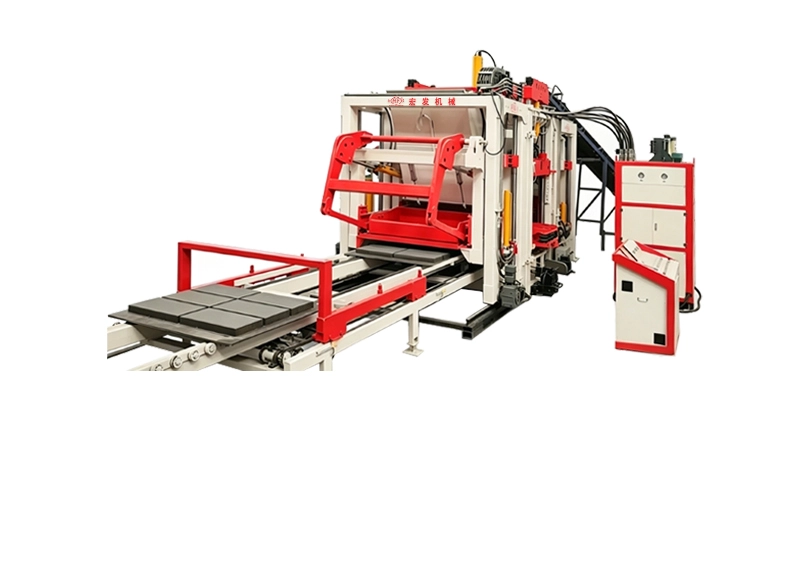
QT12‑15F is a high‑grade automatic non‑fired block‑making main unit integrated with color‑facing system, adopting platform‑vibration non‑fired forming technology. It completely abandons high‑temperature sintering kilns essential for traditional fired brick production. There is no high‑temperature burning procedure in production, generating no continuous smoke or kiln exhaust. Root‑level environmental risks including flue‑gas leakage and excessive dust that easily trigger penalties are eliminated. Boasting wide raw‑material compatibility, local bulk industrial residues like fly ash, coal gangue, slag and crushed stone waste can serve as major feedstock. It converts waste with high landfill costs into high‑standard engineering‑grade concrete blocks in large quantities. You do not need extra investment for complete flue‑gas‑treatment hardware including desulfurization towers, dust collectors and online emission monitoring devices, cutting hardware expenditure and recurring consumable costs. Zero‑flue‑gas production and large‑volume waste recycling are realized simultaneously, complying with overseas circular‑economy policies and helping large‑scale brick plants stay away from policy‑related business risks of fired brick processes.
2. Solid‑waste‑recycling Project Profile, Global‑regulation Compatible, Simplify EIA Approval for Large Plants
Developed for overseas large‑scale investors requiring mass production of colored paving products, QT12‑15F gives full play to its strength in processing large quantities of diversified solid waste to adapt to differentiated environmental legislations, pollutant limits and solid‑waste recycling rules in different countries and regions. Projects equipped with this machine are classified as high‑grade low‑pollution automatic building‑material manufacturing with bulk solid‑waste‑recycling highlights. Your factory registration and EIA application documents gain easier recognition from local regulatory authorities. It reduces risks of EIA rejection, project suspension and document revision and shortens commissioning cycles for large automatic brick plants. Investors do not need to repeatedly adjust full‑set machine layout, inject large‑sum environmental rectification funds or submit supplementary assessment papers many times. Factory construction can be advanced steadily according to original business plans, reducing hidden losses including long‑term capital tie‑up and missed large municipal‑project opportunities caused by prolonged approval procedures. It fits overseas large‑scale brick‑making investment projects that need to produce both standard blocks and colored paving bricks.
3. Zero‑flue‑gas Operation Against Frequent Environmental Audits
Benefiting from zero flue‑gas emission of QT12‑15F during machine operation, your brick plant will not face emission over‑limit alarms, site sealing or mandatory shutdown orders during unscheduled spot checks, regular online pollution monitoring and regional special environmental rectification campaigns. Heavy administrative fines caused by sudden environmental inspections are avoided. The brick plant can maintain non‑stop high‑volume production empowered by this high‑end integrated machine for both standard blocks and colored bricks, guaranteeing on‑time delivery for bulk construction and municipal orders. It prevents chain‑reaction negative outcomes such as contract breach, loss of key major customers and corporate reputational damage triggered by unplanned shutdown. Amid tightening overseas environmental supervision, this machine minimizes operational uncertainties brought by environmental inspections and stabilizes plant revenue. Combined economic losses from penalties, forced shutdowns and lost large‑value orders are effectively prevented, and automatic production rhythm will not be disturbed by shifting environmental policies.
4. Built‑in Color‑facing System for Premium Recycled Building Materials for Large‑scale Municipal Tenders
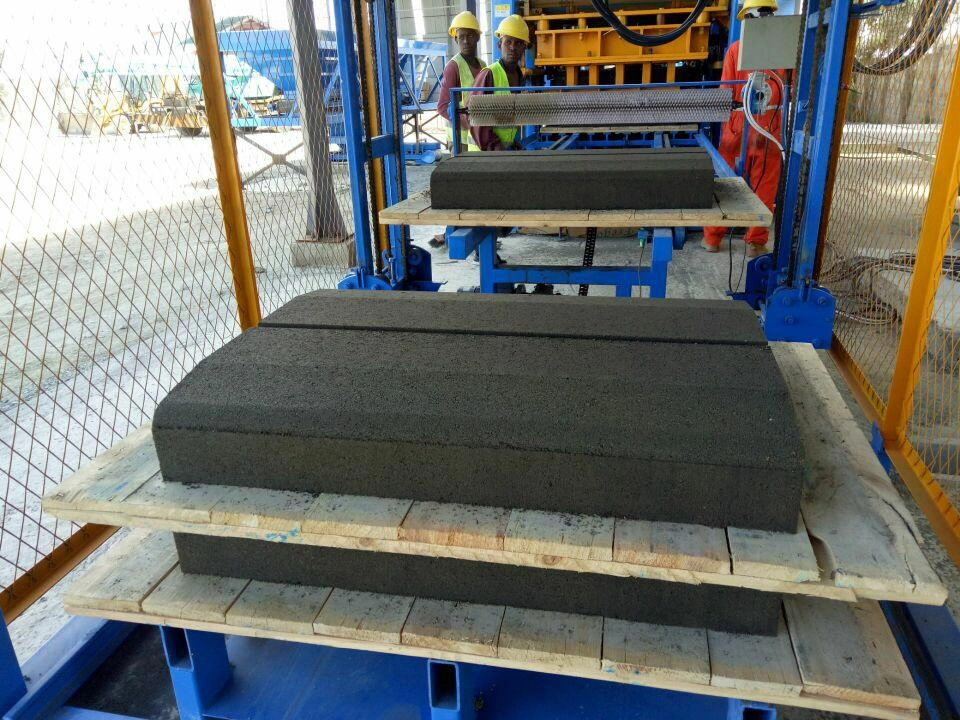
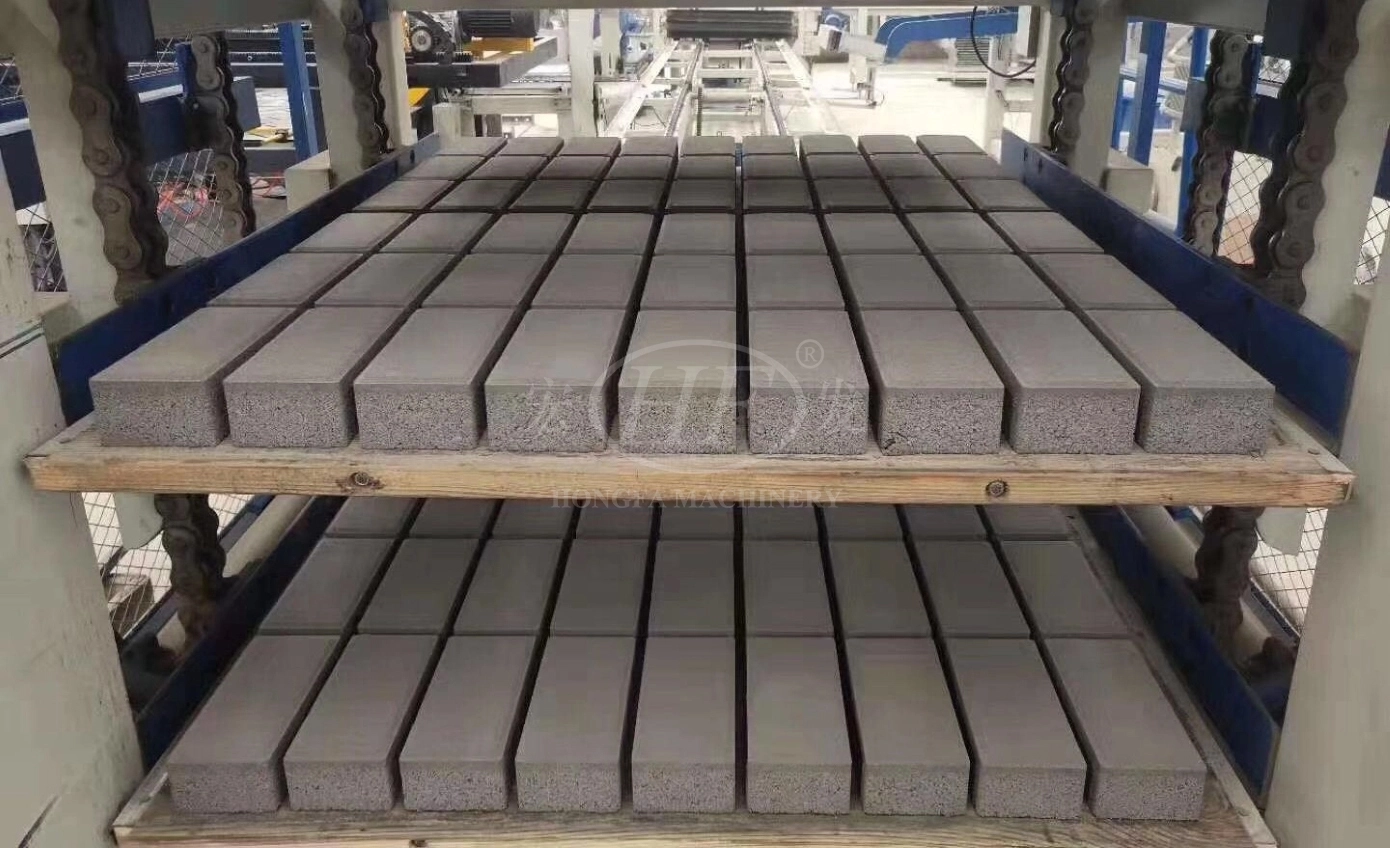
QT12‑15F comes with integrated independent color‑facing production unit, it can mass‑produce high‑value solid‑waste recycled products including colored facing paving bricks, interlocking blocks, curbstones, grass‑planting bricks and ecological slope‑protection blocks. All finished goods are compliant green building materials. Its strength in consuming large volumes of local solid waste fully satisfies bid‑entry standards for government green‑procurement projects such as municipal arterial roads, sponge‑city construction, landscape gardening and river ecological restoration. Many overseas official green projects explicitly restrict fired‑brick suppliers from tender participation, while non‑fired recycled blocks from this machine can smoothly enter candidate bidding lists. Brick plants gain access to large official engineering channels unreachable for traditional fired‑brick manufacturers and secure long‑term municipal projects with reliable payment and huge order volume. You can step out of low‑price retail‑oriented competition, develop high‑added‑value bulk business sources and improve overall order quality and profit margin of the factory.
5. No Kiln‑required Infrastructure, Cut Up‑front Setup Cost for High‑end Automatic Large‑size Plants
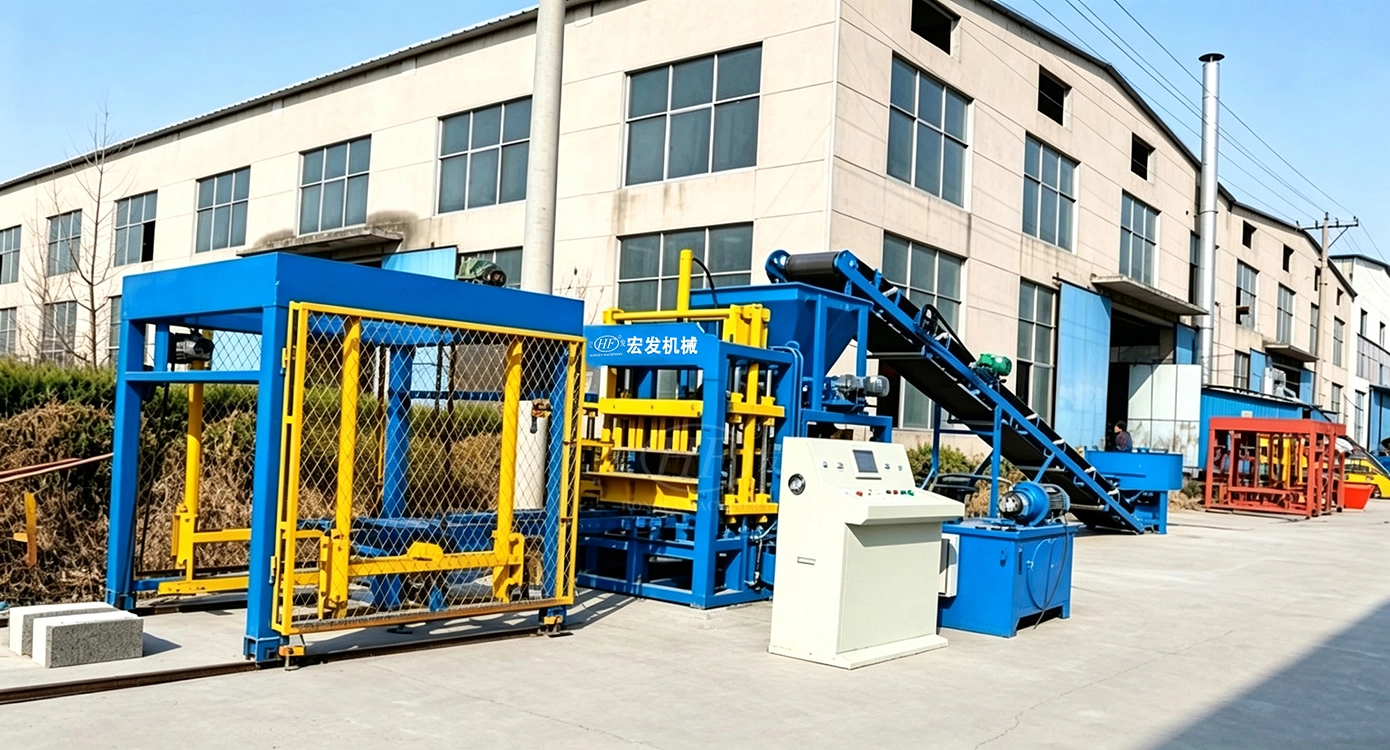
QT12‑15F non‑fired block‑making machine removes requirements for large‑scale sintering‑related infrastructure such as kiln workshops, long flue ducts, kiln‑residue storage yards and independent waste‑gas treatment rooms. Designed as a full‑automatic high‑grade integrated unit with built‑in color‑facing system, the main machine features neat and compact layout and requires no extra land reserved for flue‑gas treatment. One‑time upfront costs for land rental, civil engineering and environmental auxiliary facilities are substantially reduced. Startup capital will no longer be heavily consumed on kiln construction and flue‑gas‑treatment infrastructure. Saved funds can be prioritized for revenue‑generating activities including raw‑material yard expansion, local key‑customer development and bulk‑order preparation. It works well for first‑time overseas investors purchasing high‑end automatic brick‑making machines, as well as existing large fired‑brick plants undertaking automatic environmental upgrades to avoid policy‑driven phase‑out risks, matching diverse capital budgets and transformation demands.
6. Quick‑change Molds for Mass‑production of Diversified High‑quality Products
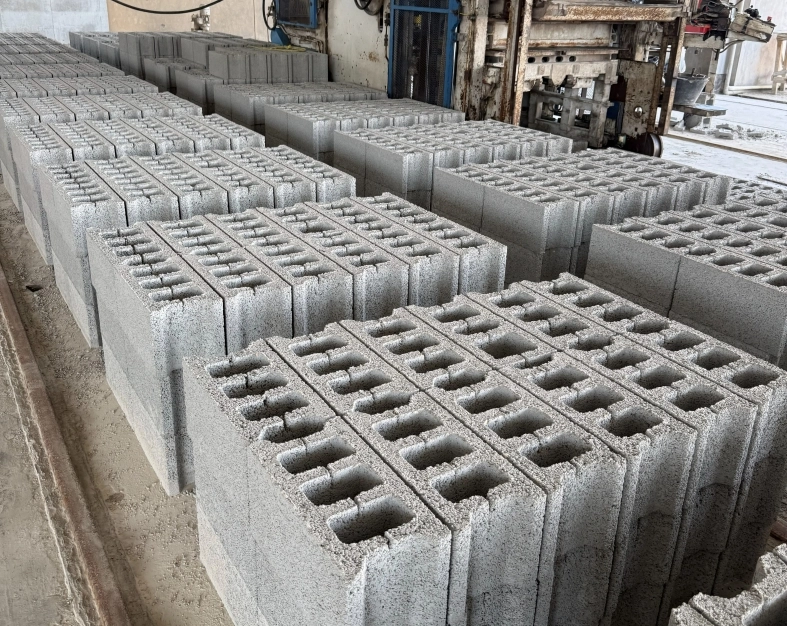
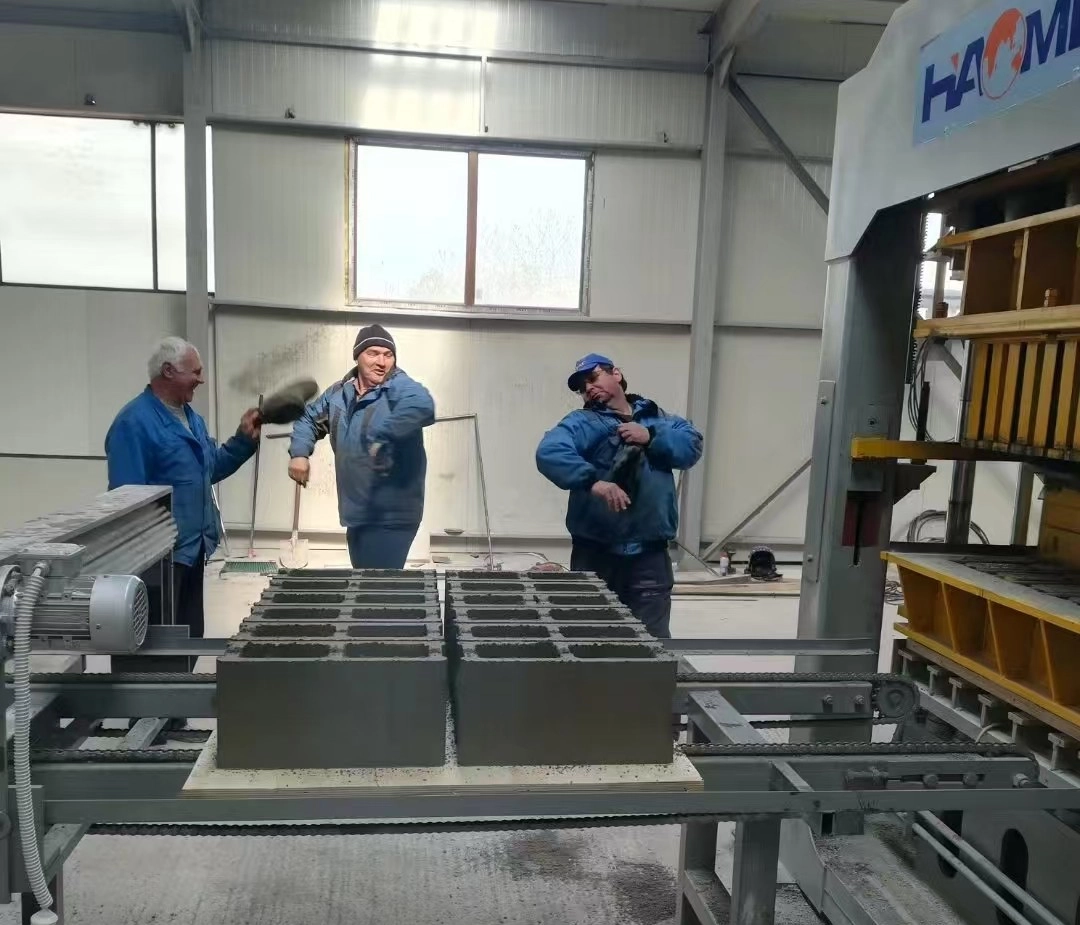
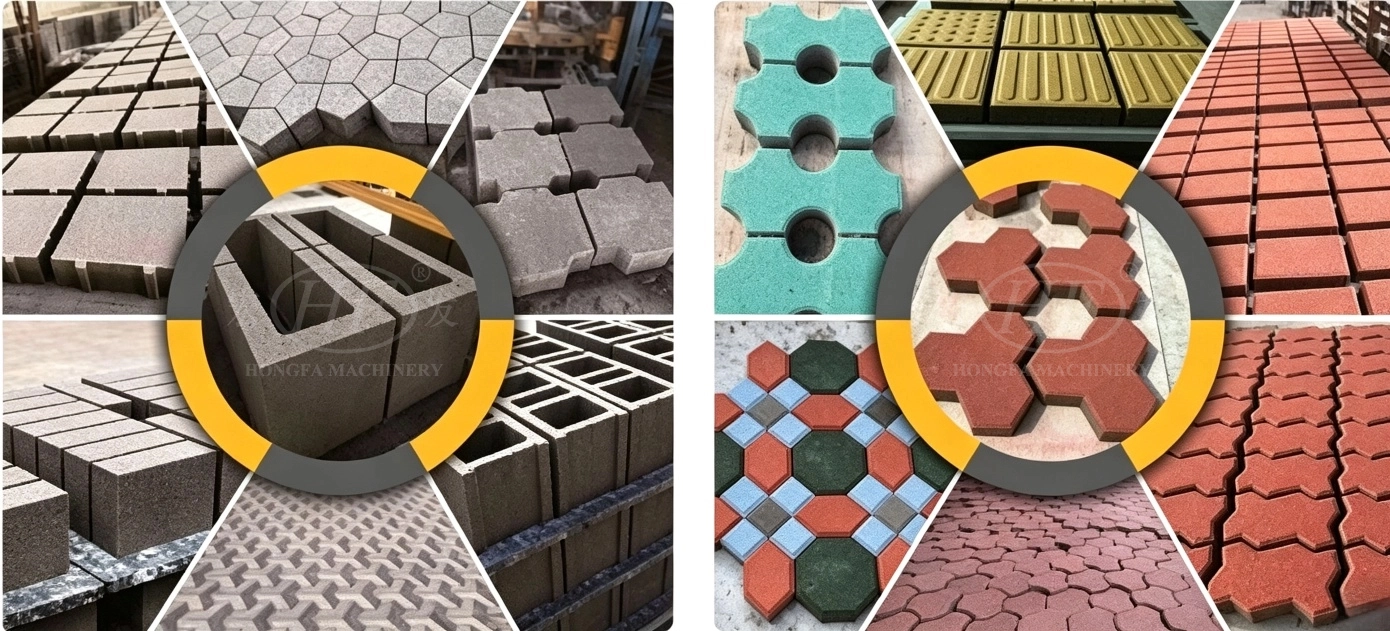
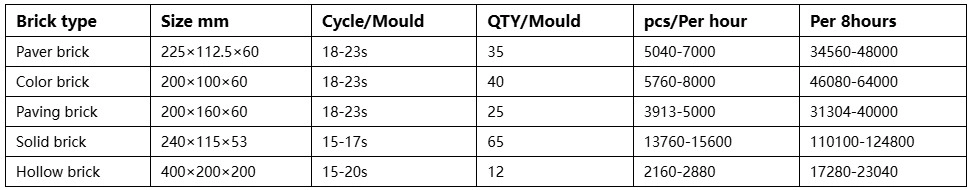
By simply replacing molds on QT12‑15F automatic block machine, you can mass‑produce various non‑fired concrete products including hollow blocks, perforated bricks, standard bricks, colored facing paving bricks, interlocking blocks, grass‑planting bricks, slope‑protection blocks and curbstones. All finished goods are zero‑emission compliant recycled building materials and are exempt from local smoke‑emission control policies. The diversified product portfolio covers multiple downstream markets including residential construction, large‑park paving, water‑conservancy slope stabilization and urban arterial road renovation. One single high‑grade integrated main machine supports multi‑category bulk customer orders. You can adjust product mix responsively according to local‑market demands without purchasing extra brick‑making main units for new items. It continuously expands market sales coverage of compliant green building materials and strengthens comprehensive competitiveness of large‑scale automatic plants against market‑cycle fluctuations.
1. Non‑fired Forming for Large‑scale Solid‑waste Recycling With High‑spec Configuration
QT12‑15F is a high‑grade automatic non‑fired block‑making main unit integrated with color‑facing system, adopting platform‑vibration non‑fired forming technology. It completely abandons high‑temperature sintering kilns essential for traditional fired brick production. There is no high‑temperature burning procedure in production, generating no continuous smoke or kiln exhaust. Root‑level environmental risks including flue‑gas leakage and excessive dust that easily trigger penalties are eliminated. Boasting wide raw‑material compatibility, local bulk industrial residues like fly ash, coal gangue, slag and crushed stone waste can serve as major feedstock. It converts waste with high landfill costs into high‑standard engineering‑grade concrete blocks in large quantities. You do not need extra investment for complete flue‑gas‑treatment hardware including desulfurization towers, dust collectors and online emission monitoring devices, cutting hardware expenditure and recurring consumable costs. Zero‑flue‑gas production and large‑volume waste recycling are realized simultaneously, complying with overseas circular‑economy policies and helping large‑scale brick plants stay away from policy‑related business risks of fired brick processes.
2. Solid‑waste‑recycling Project Profile, Global‑regulation Compatible, Simplify EIA Approval for Large Plants
Developed for overseas large‑scale investors requiring mass production of colored paving products, QT12‑15F gives full play to its strength in processing large quantities of diversified solid waste to adapt to differentiated environmental legislations, pollutant limits and solid‑waste recycling rules in different countries and regions. Projects equipped with this machine are classified as high‑grade low‑pollution automatic building‑material manufacturing with bulk solid‑waste‑recycling highlights. Your factory registration and EIA application documents gain easier recognition from local regulatory authorities. It reduces risks of EIA rejection, project suspension and document revision and shortens commissioning cycles for large automatic brick plants. Investors do not need to repeatedly adjust full‑set machine layout, inject large‑sum environmental rectification funds or submit supplementary assessment papers many times. Factory construction can be advanced steadily according to original business plans, reducing hidden losses including long‑term capital tie‑up and missed large municipal‑project opportunities caused by prolonged approval procedures. It fits overseas large‑scale brick‑making investment projects that need to produce both standard blocks and colored paving bricks.
3. Zero‑flue‑gas Operation Against Frequent Environmental Audits
Benefiting from zero flue‑gas emission of QT12‑15F during machine operation, your brick plant will not face emission over‑limit alarms, site sealing or mandatory shutdown orders during unscheduled spot checks, regular online pollution monitoring and regional special environmental rectification campaigns. Heavy administrative fines caused by sudden environmental inspections are avoided. The brick plant can maintain non‑stop high‑volume production empowered by this high‑end integrated machine for both standard blocks and colored bricks, guaranteeing on‑time delivery for bulk construction and municipal orders. It prevents chain‑reaction negative outcomes such as contract breach, loss of key major customers and corporate reputational damage triggered by unplanned shutdown. Amid tightening overseas environmental supervision, this machine minimizes operational uncertainties brought by environmental inspections and stabilizes plant revenue. Combined economic losses from penalties, forced shutdowns and lost large‑value orders are effectively prevented, and automatic production rhythm will not be disturbed by shifting environmental policies.
4. Built‑in Color‑facing System for Premium Recycled Building Materials for Large‑scale Municipal Tenders
QT12‑15F comes with integrated independent color‑facing production unit, it can mass‑produce high‑value solid‑waste recycled products including colored facing paving bricks, interlocking blocks, curbstones, grass‑planting bricks and ecological slope‑protection blocks. All finished goods are compliant green building materials. Its strength in consuming large volumes of local solid waste fully satisfies bid‑entry standards for government green‑procurement projects such as municipal arterial roads, sponge‑city construction, landscape gardening and river ecological restoration. Many overseas official green projects explicitly restrict fired‑brick suppliers from tender participation, while non‑fired recycled blocks from this machine can smoothly enter candidate bidding lists. Brick plants gain access to large official engineering channels unreachable for traditional fired‑brick manufacturers and secure long‑term municipal projects with reliable payment and huge order volume. You can step out of low‑price retail‑oriented competition, develop high‑added‑value bulk business sources and improve overall order quality and profit margin of the factory.
5. No Kiln‑required Infrastructure, Cut Up‑front Setup Cost for High‑end Automatic Large‑size Plants
QT12‑15F non‑fired block‑making machine removes requirements for large‑scale sintering‑related infrastructure such as kiln workshops, long flue ducts, kiln‑residue storage yards and independent waste‑gas treatment rooms. Designed as a full‑automatic high‑grade integrated unit with built‑in color‑facing system, the main machine features neat and compact layout and requires no extra land reserved for flue‑gas treatment. One‑time upfront costs for land rental, civil engineering and environmental auxiliary facilities are substantially reduced. Startup capital will no longer be heavily consumed on kiln construction and flue‑gas‑treatment infrastructure. Saved funds can be prioritized for revenue‑generating activities including raw‑material yard expansion, local key‑customer development and bulk‑order preparation. It works well for first‑time overseas investors purchasing high‑end automatic brick‑making machines, as well as existing large fired‑brick plants undertaking automatic environmental upgrades to avoid policy‑driven phase‑out risks, matching diverse capital budgets and transformation demands.
6. Quick‑change Molds for Mass‑production of Diversified High‑quality Products
By simply replacing molds on QT12‑15F automatic block machine, you can mass‑produce various non‑fired concrete products including hollow blocks, perforated bricks, standard bricks, colored facing paving bricks, interlocking blocks, grass‑planting bricks, slope‑protection blocks and curbstones. All finished goods are zero‑emission compliant recycled building materials and are exempt from local smoke‑emission control policies. The diversified product portfolio covers multiple downstream markets including residential construction, large‑park paving, water‑conservancy slope stabilization and urban arterial road renovation. One single high‑grade integrated main machine supports multi‑category bulk customer orders. You can adjust product mix responsively according to local‑market demands without purchasing extra brick‑making main units for new items. It continuously expands market sales coverage of compliant green building materials and strengthens comprehensive competitiveness of large‑scale automatic plants against market‑cycle fluctuations.
 HF18 Pallet‑free Automatic Non‑fired Brick Machine | Zero Flue‑gas, Large‑output Waste‑recycling Eco‑friendly Brick Equipment
HF18 pallet‑free automatic non‑fired block machine features pallet‑free automatic operation. It requires no sintering ki...
 QT12‑15F Automatic Non‑fired Brick Machine | Zero Flue‑gas, High‑capacity Color‑paver Waste‑recycling Eco‑friendly Brick Equipment
QT12‑15F automatic non‑fired block machine is integrated with independent color‑facing feeding unit. It requires no sint...
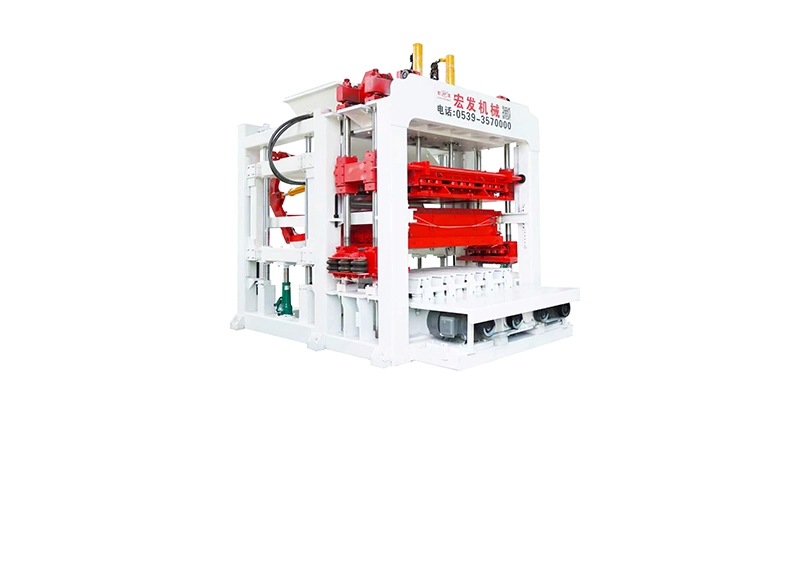 QT12‑15C Automatic Non‑fired Brick Machine | Zero Flue‑gas, High‑spec Waste‑recycling Eco‑friendly Brick Equipment
QT12‑15C automatic non‑fired block machine is a high‑spec integrated main unit. It requires no sintering kiln and achiev...
Shandong Hongfa Scientific Industrial&Trading Co.,Ltd ©️2026Copyright © LU ICP B 16041216-4