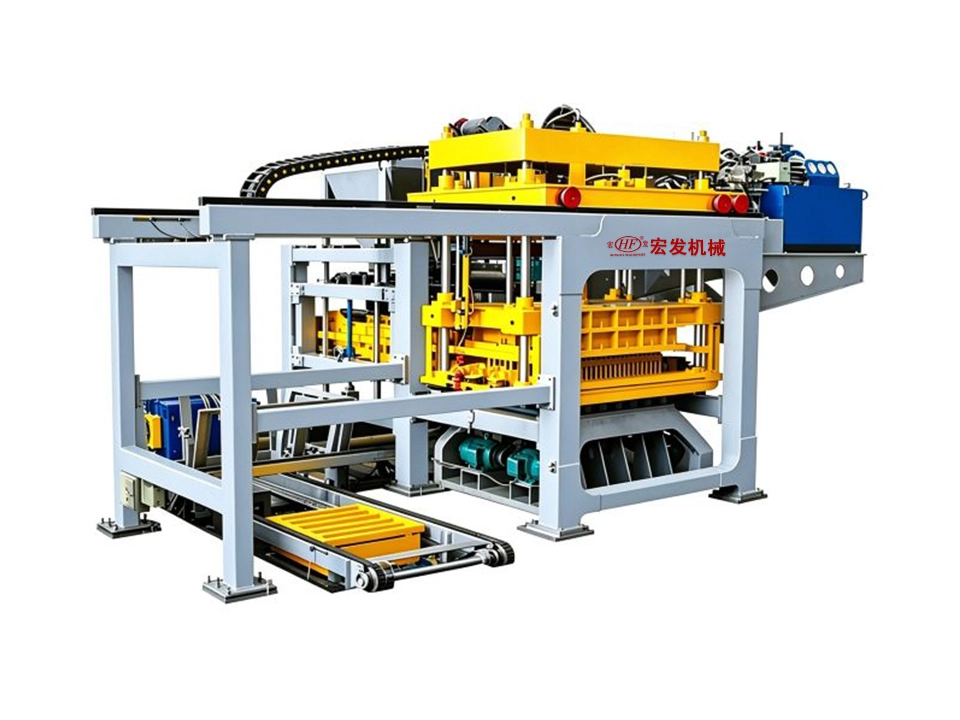
1. Pallet‑Free High‑Capacity Main‑Machine Output to Support Super‑Large General‑Contract Project Bulk Supply
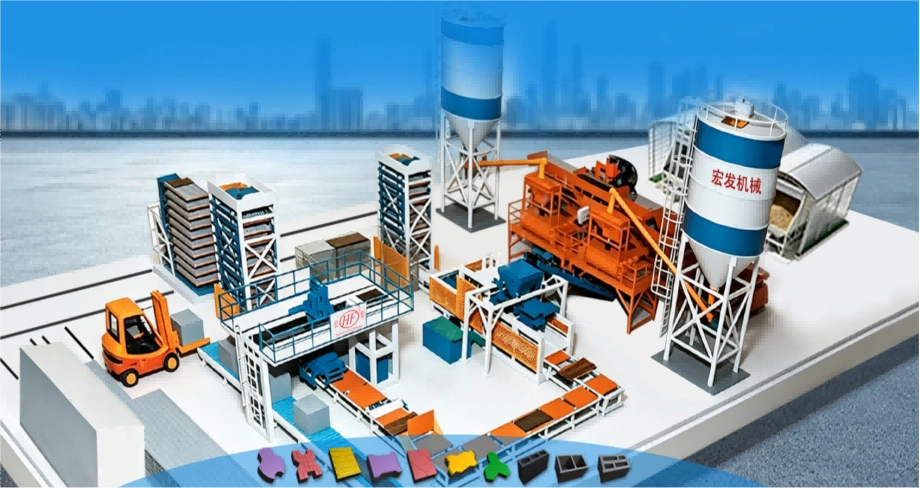
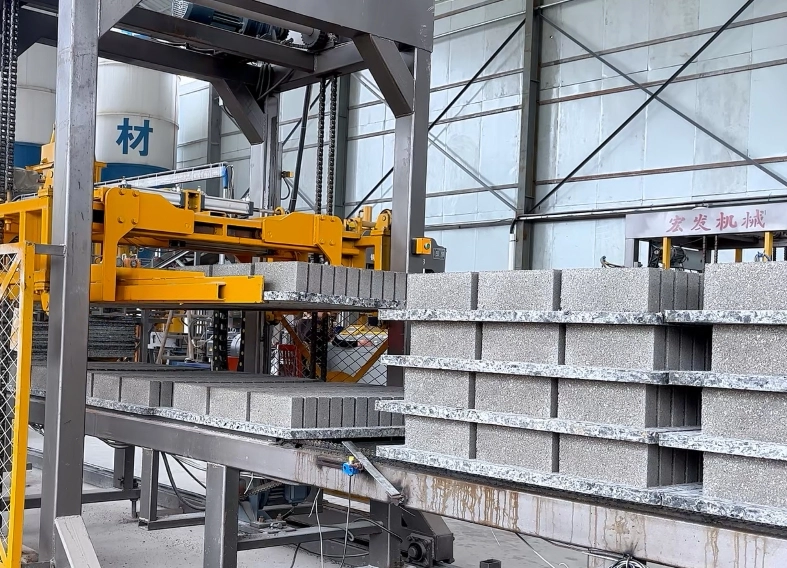
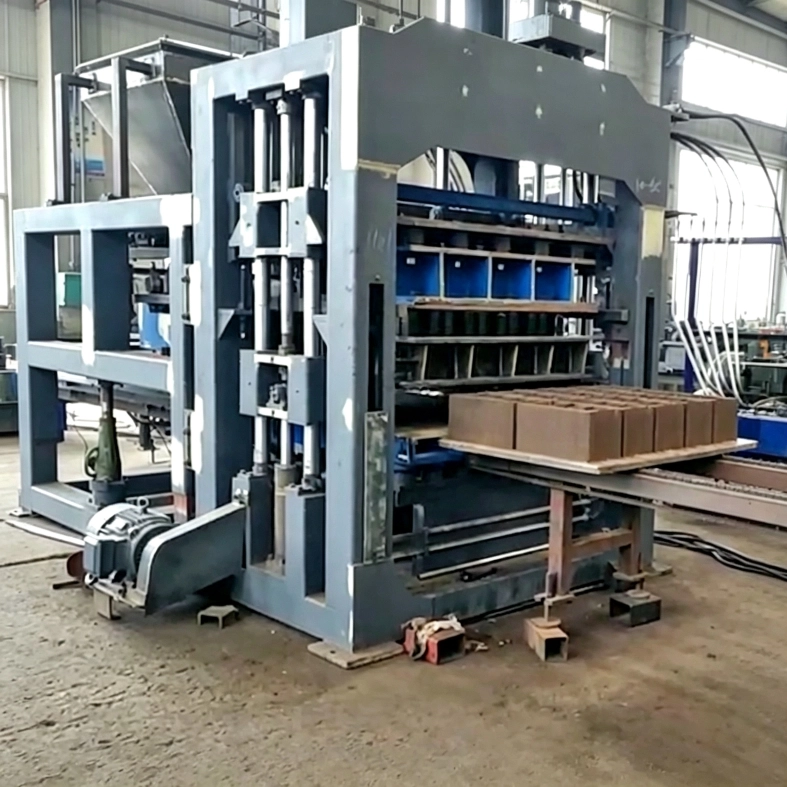
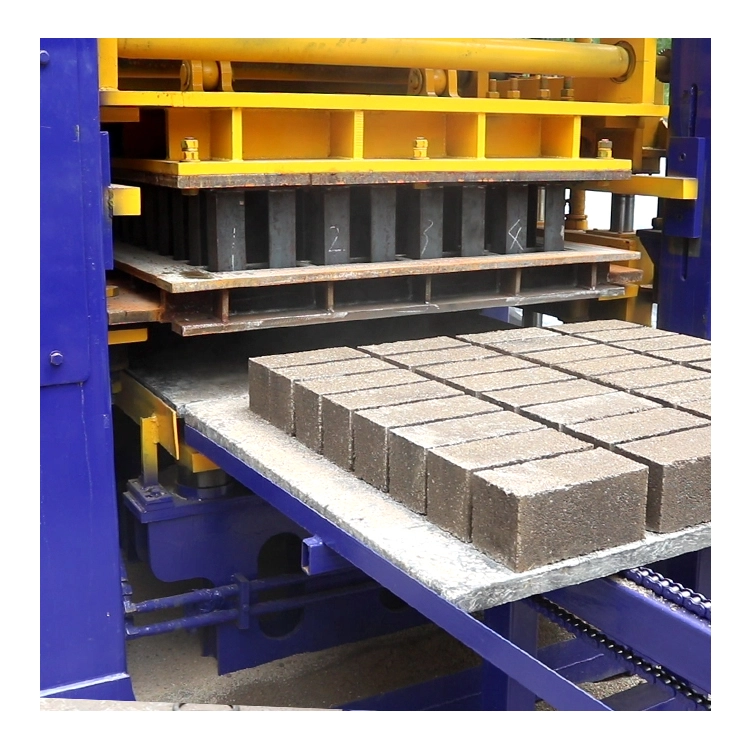
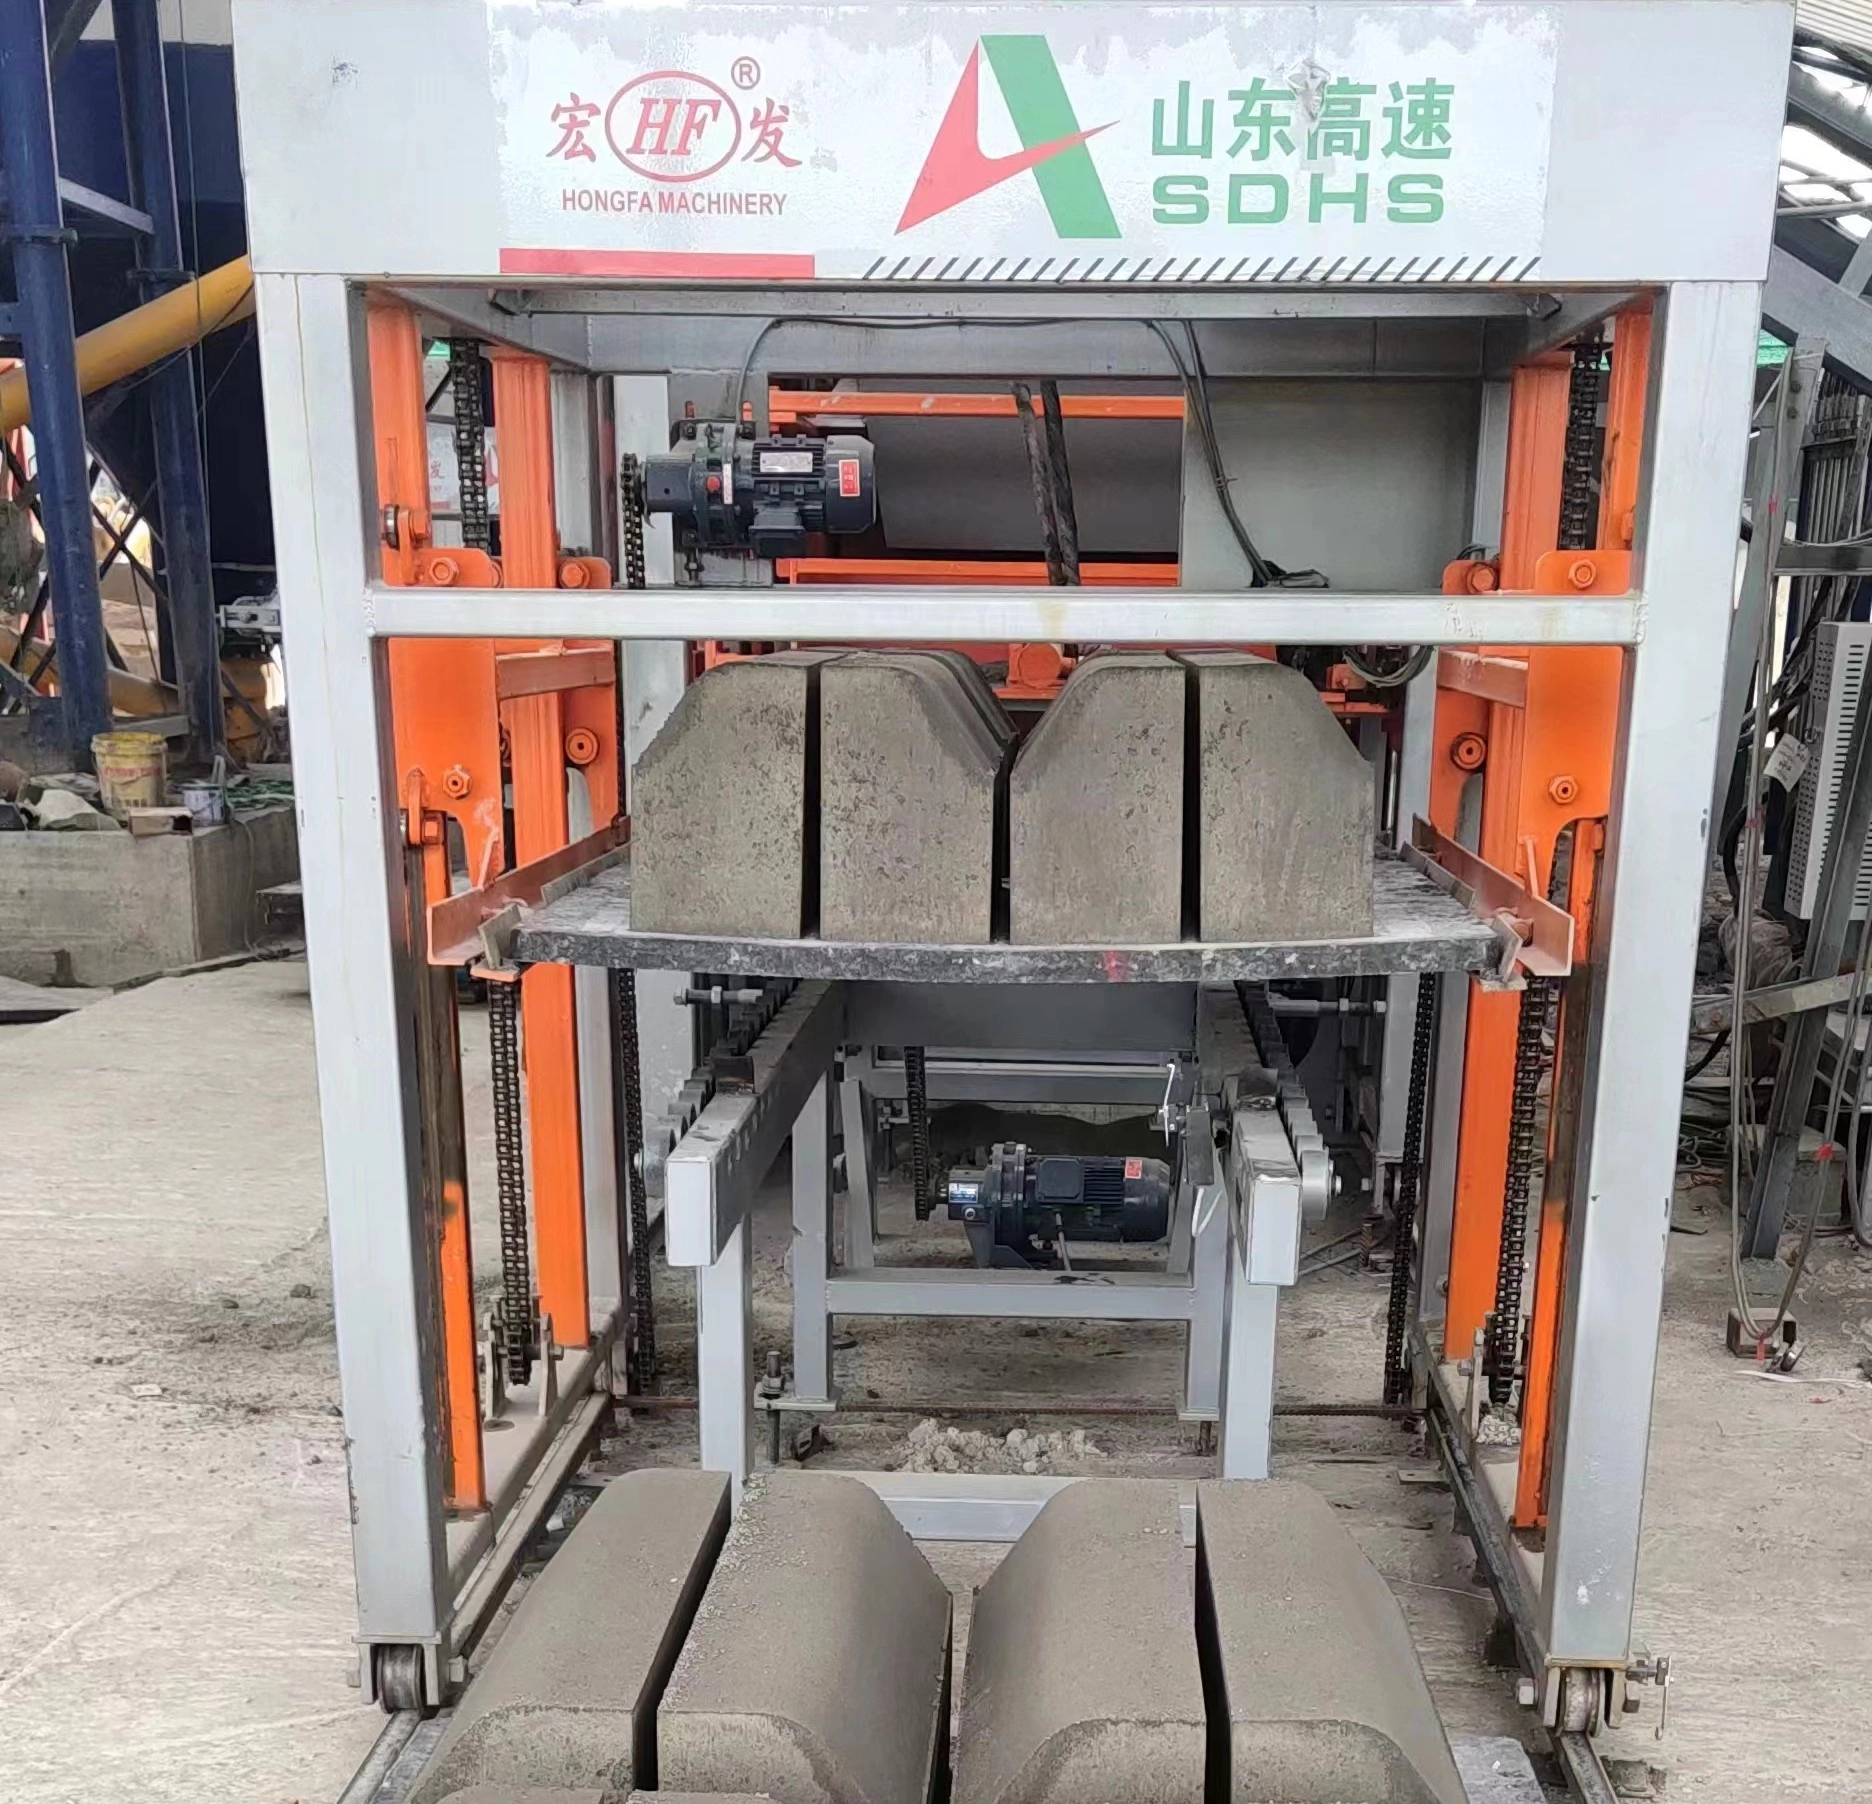
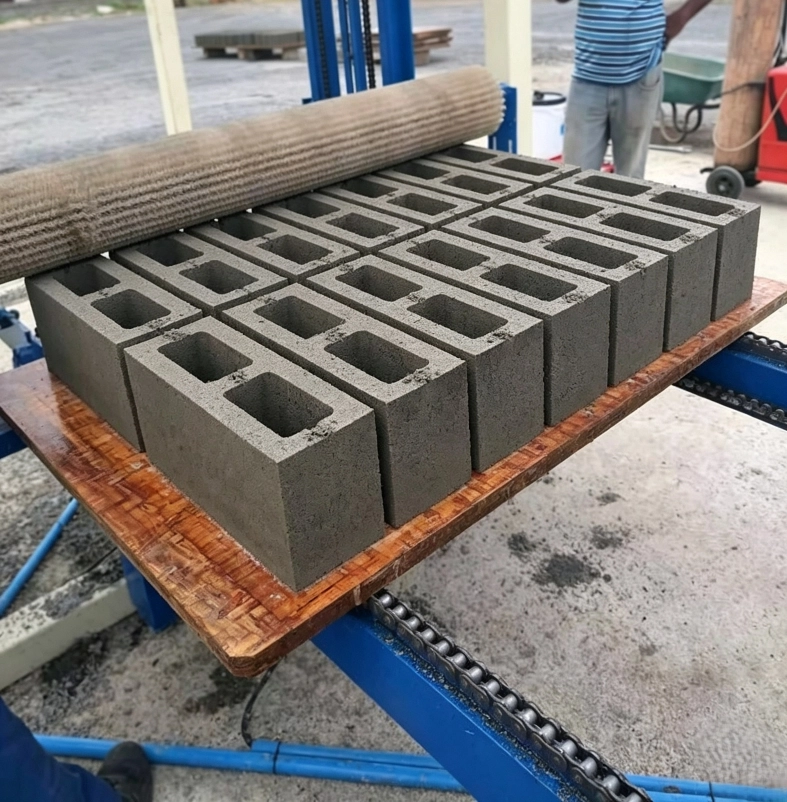
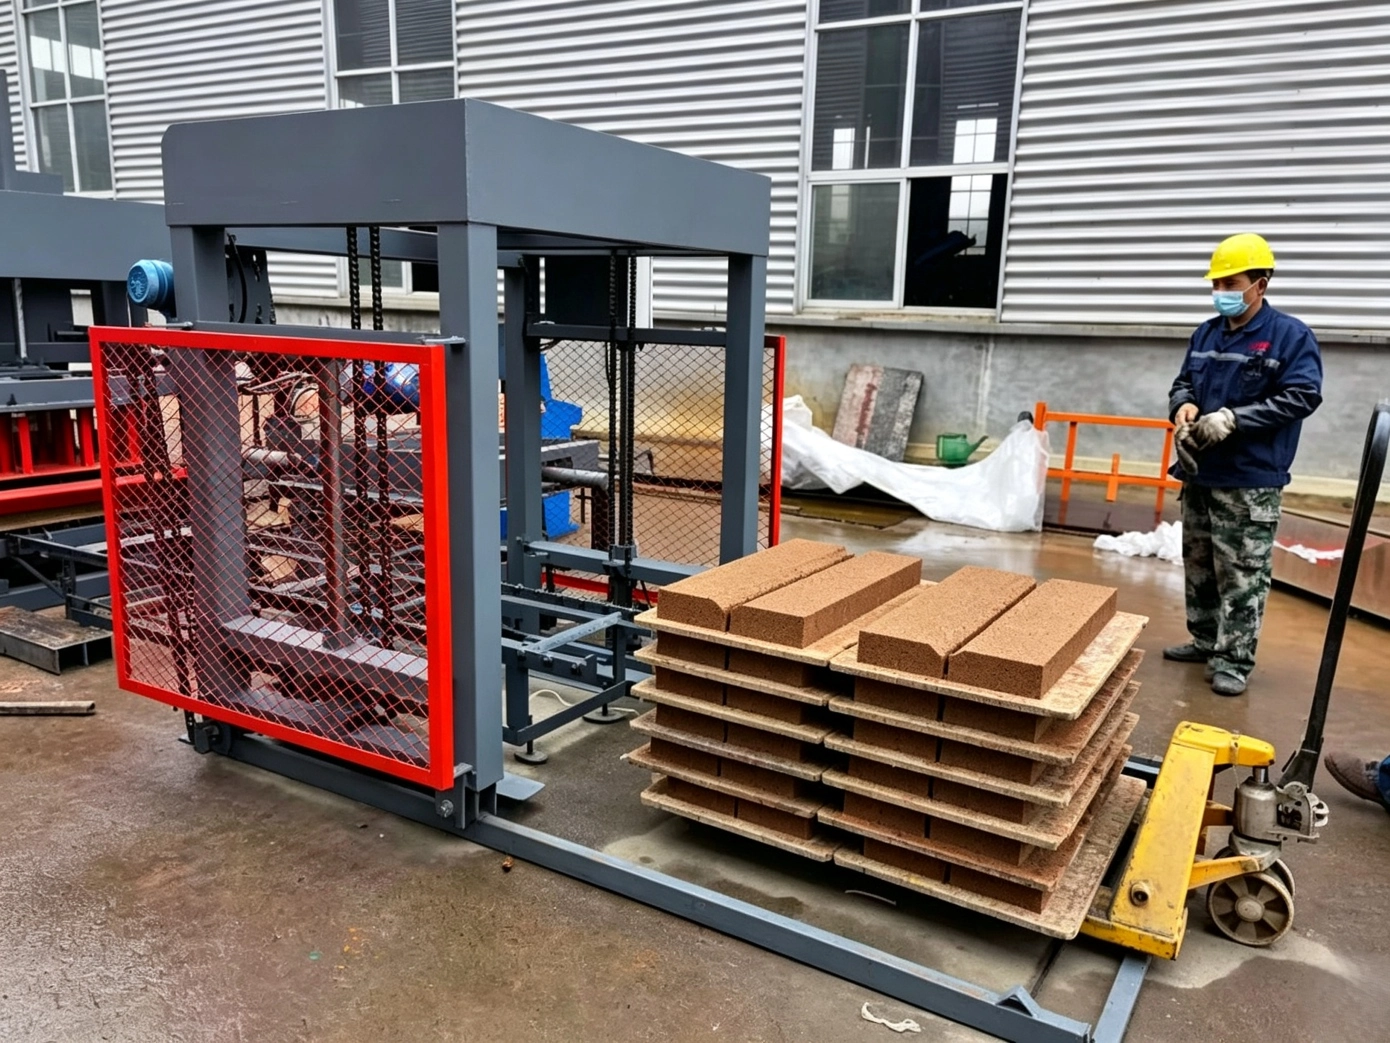
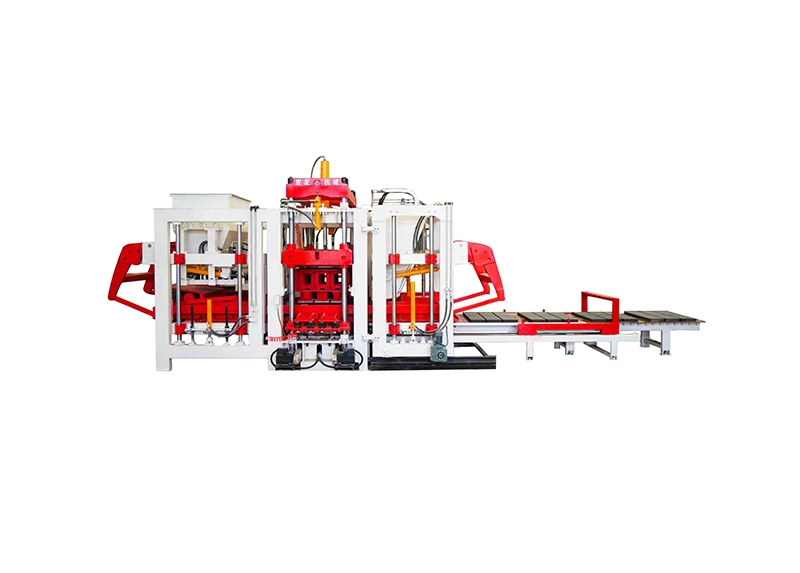
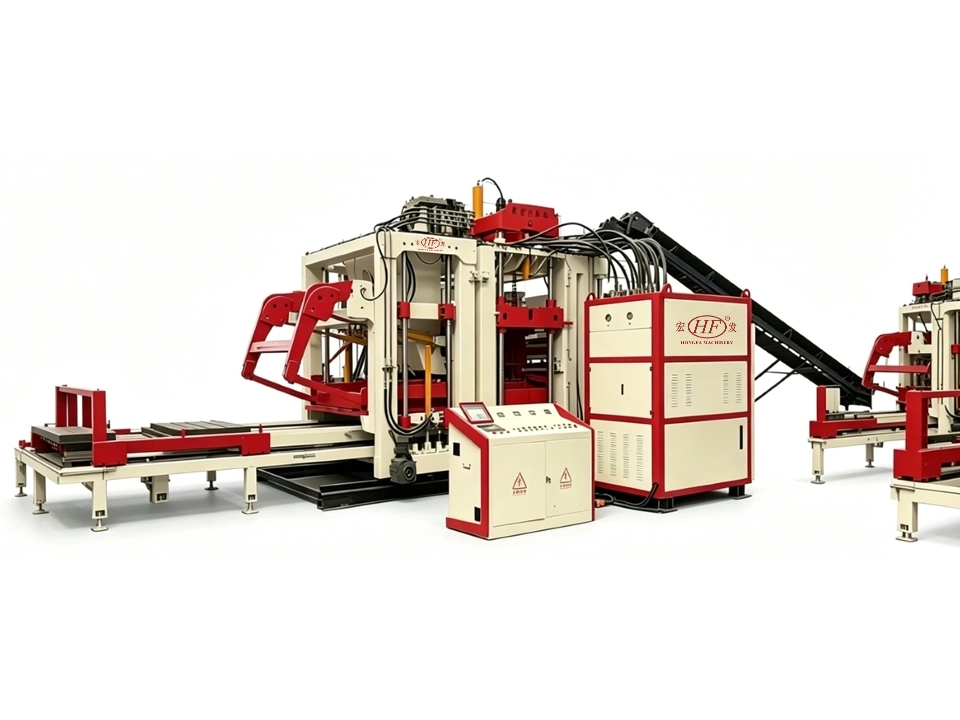
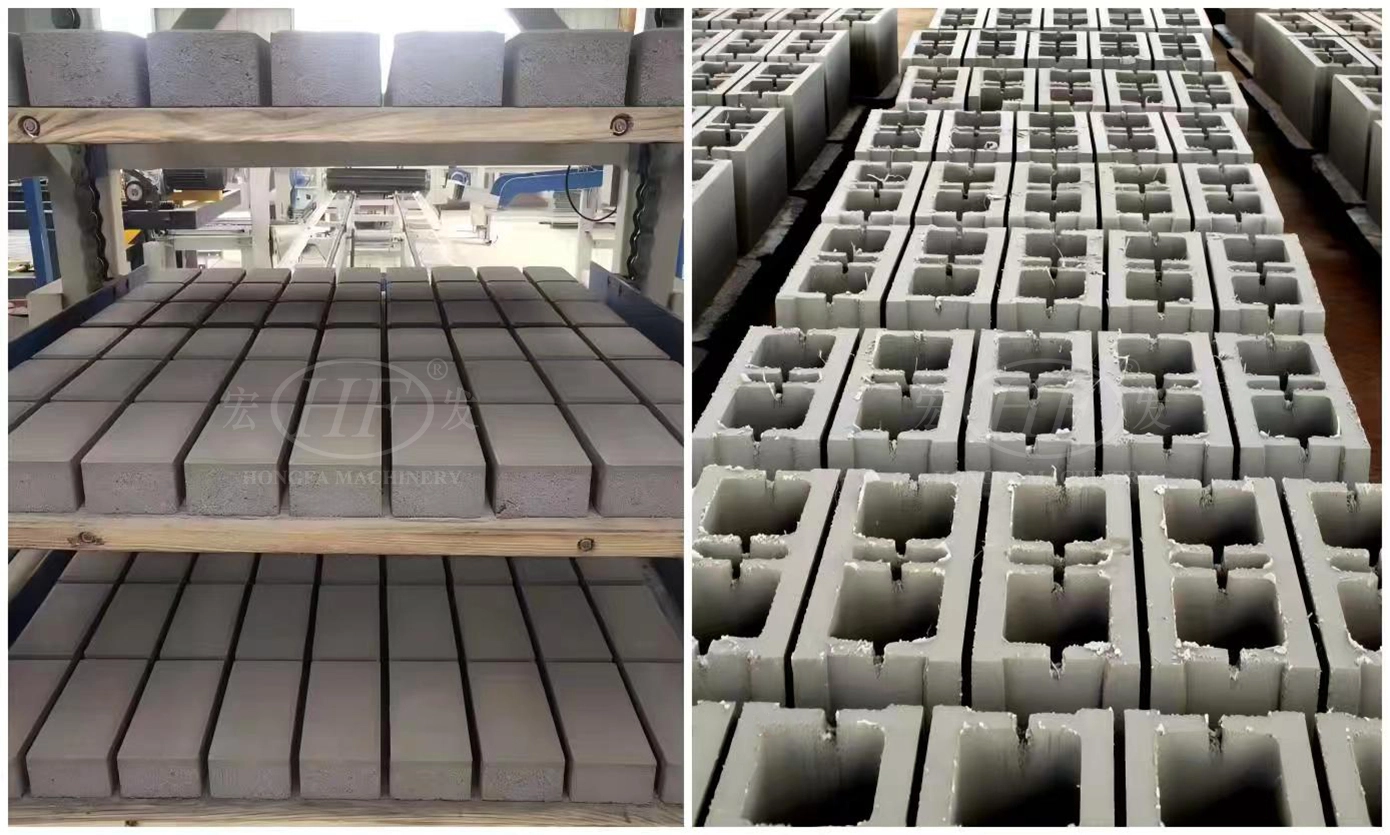
Many well‑established large brick plants have rich engineering client resources, yet they are restricted by output limits of conventional pallet‑based forming machines. When facing huge‑volume tenders for urban renewal and large residential clusters, they dare not accept massive‑supply contracts due to insufficient single‑machine output and miss lucrative long‑term projects. Conventional machines also generate recurring costs for pallet procurement and regular replacement caused by wear. As a pallet‑free automatic block forming main unit, HF18 adopts built‑in demolding and stacking mechanism, which removes reliance on large quantities of circulating pallets. It enables intensive continuous mass production of standard bricks, hollow blocks, slope‑protection blocks, colored paving bricks and full‑range engineering products. For capacity expansion of existing brick plants equipped with batching and mixing systems, adding this main machine does not require complete pallet‑flow auxiliary accessories and directly lifts overall plant capacity ceiling. After upgrade, your factory gains solid capability for concentrated delivery of super‑large projects. You become eligible to bid for heavy‑weight engineering projects that were previously unreachable, converting huge potential orders into steady annual revenue and capturing high‑value regional engineering‑supply resources.
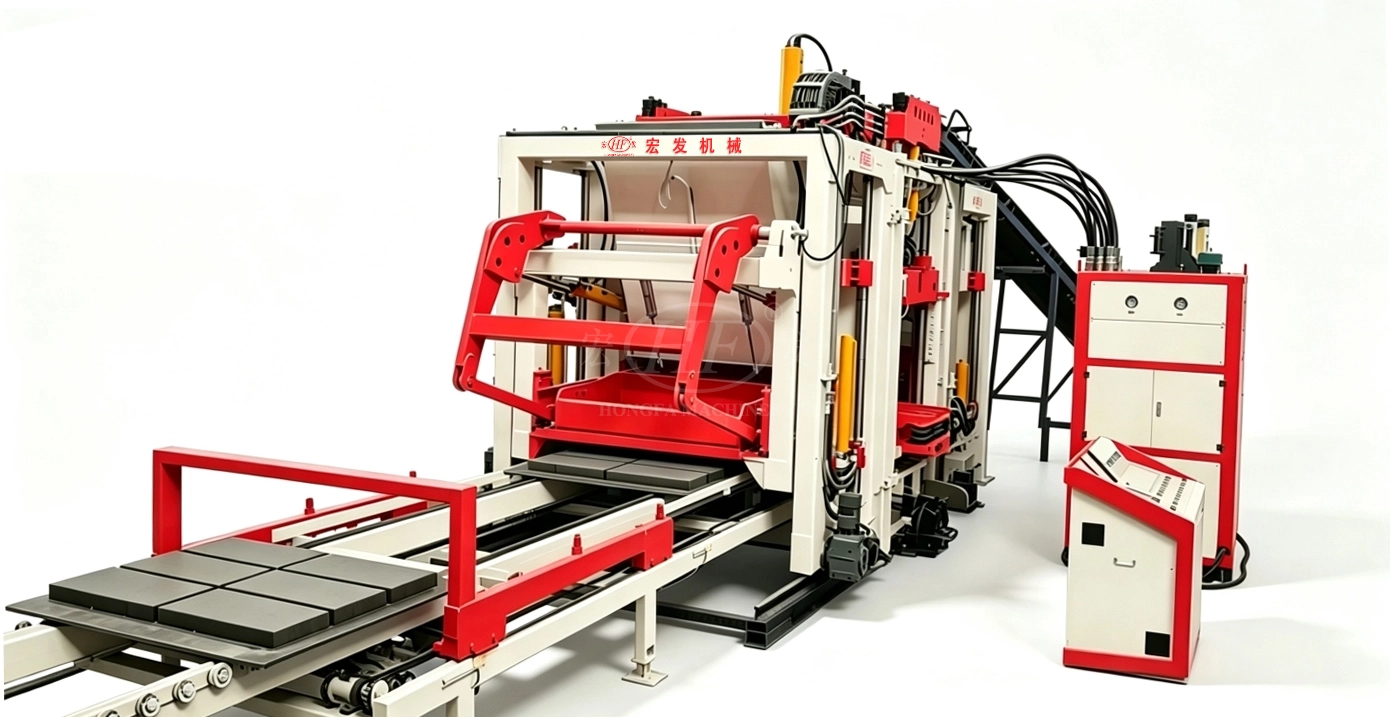
2. Remove Pallet Consumable Expenses & Cut On‑Site Labor to Lower Comprehensive Block Costs From Two Dimensions
Besides machine procurement, traditional pallet‑based block forming machines require continuous annual investment for purchasing and replacing worn pallets. Plenty of operators are also needed for pallet transfer and material docking, leading to high labor expenditure. Even when output rises, consumable and labor costs will eat up substantial profit margins. HF18 pallet‑free forming main unit completes demolding and stacking inside the machine. Pallet circulation is eliminated in production process, completely getting rid of ongoing costs for pallet procurement, maintenance and replacement. Thanks to high automation level, only a small number of on‑site staff are required for machine monitoring and finished‑goods handling, significantly cutting post‑s manpower demand. Both consumable and labor expenses are reduced. Combined with economies of scale brought by high main‑machine capacity, fixed expenditures covering labor, power and site overhead are spread over massive quantities of finished blocks to further lower comprehensive per‑unit production cost. During engineering tender quotation, you obtain enhanced pricing flexibility. You can win huge supply contracts with competitive offers while maintaining decent profit margins, realizing simultaneous growth in order volume and profitability.
3. Built‑In Face‑Mix Unit for Diversified Engineering Products to Expand High‑Value Order Channels
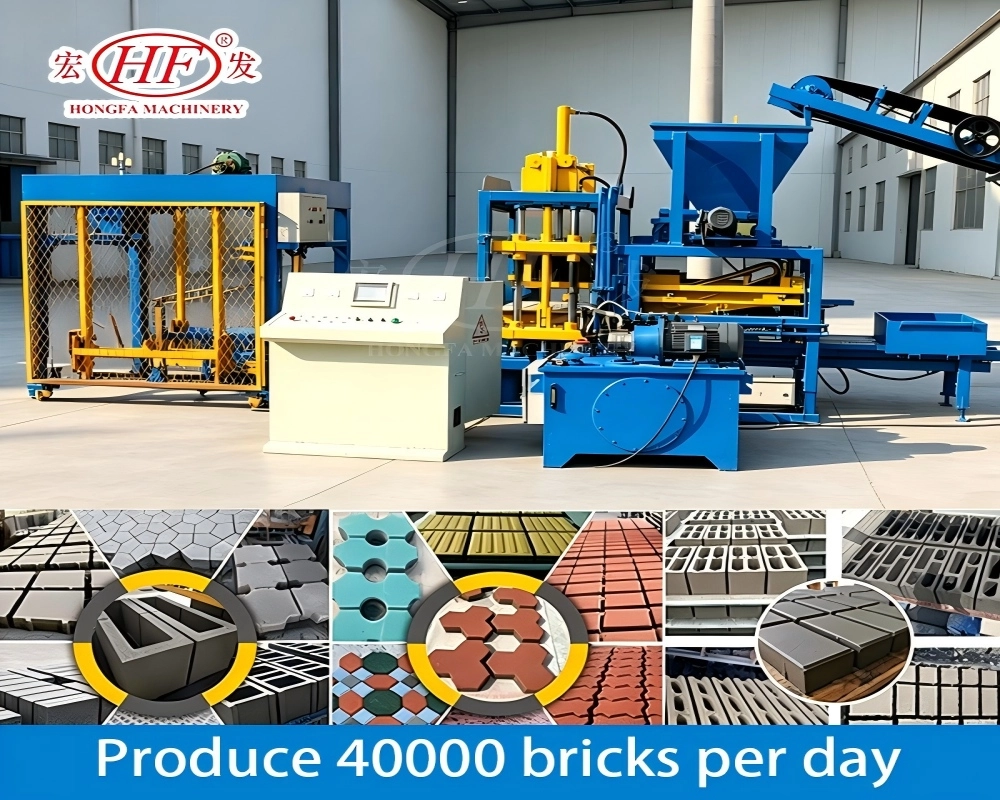
Quite a number of large brick factories mainly produce ordinary grey blocks after capacity expansion. Restricted by machine functions, they cannot take high‑margin municipal colored‑landscape‑brick orders. Although production capacity grows, business structure remains single, bringing high operational risks when market demand fluctuates. HF18 main machine is equipped with integrated automatic face‑mix unit. Without modifying main‑machine structure, it stably produces colored paving bricks, plaza bricks and slope‑protection blocks, as well as standard bricks, various hollow blocks, road curbstones and other mainstream engineering blocks. After main‑machine capacity upgrade, your factory can undertake bulk wall‑block supply for residential complexes and high‑profit municipal landscape projects from urban‑renewal initiatives. There is no need to purchase extra dedicated colored‑brick forming equipment. One single main‑machine covers both high‑volume basic products and high‑value landscape articles. Diversified order sources mitigate operational risks caused by declining demand for single‑product categories and ensure high‑capacity utilization with steady incoming orders.
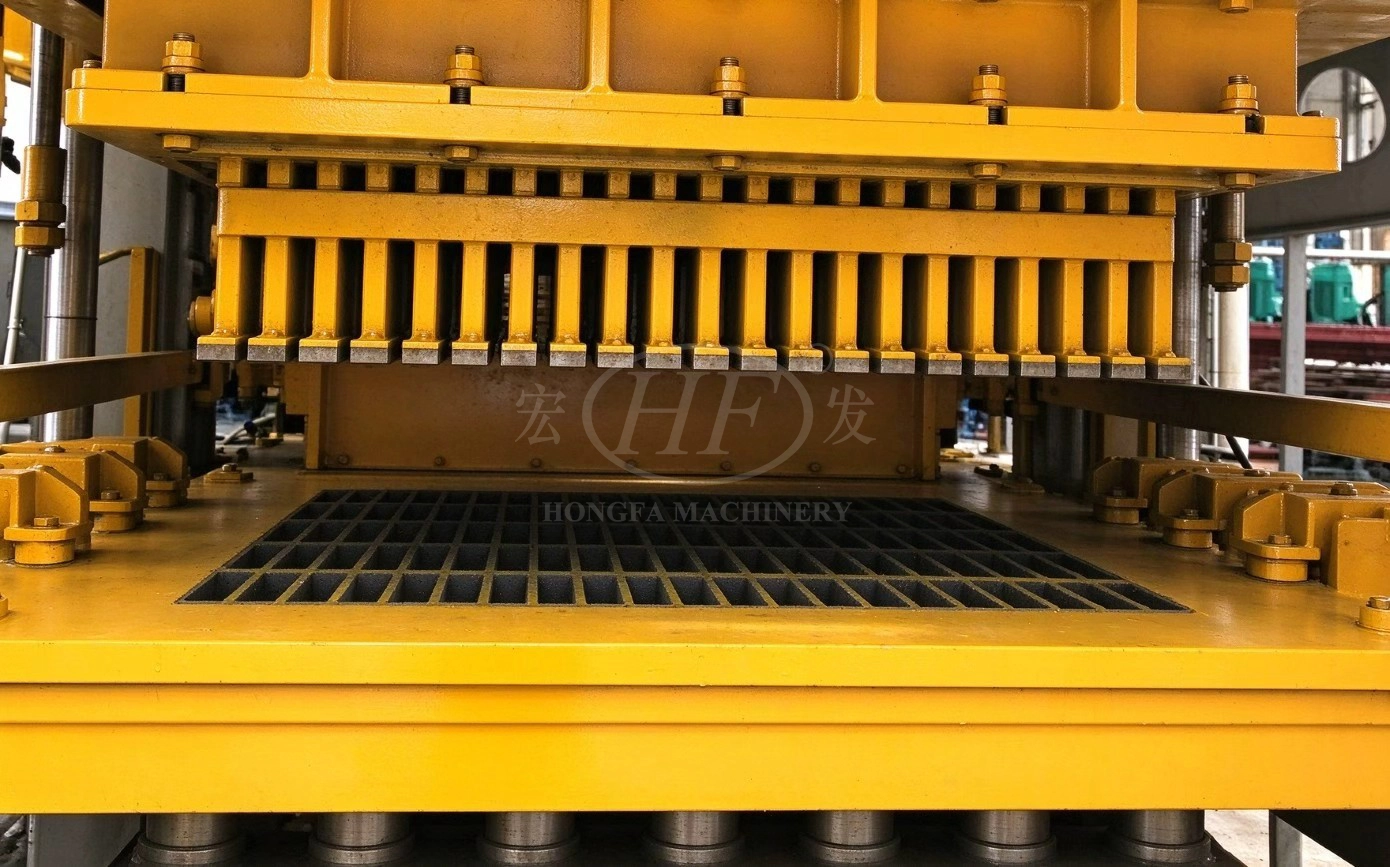
4. Integrated Demolding & Stacking Functions Reduce Auxiliary Equipment Needs and Control Total Expansion Investment
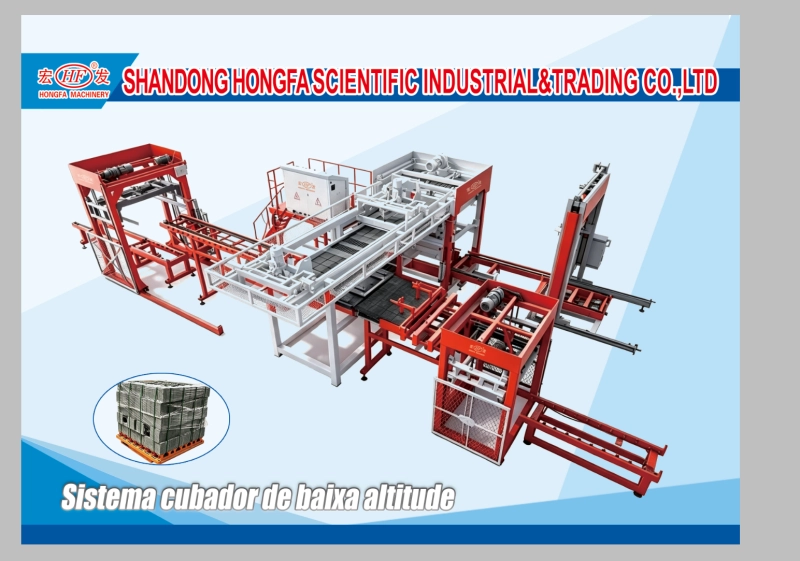
Traditional high‑capacity forming machines demand extra auxiliary devices such as pallet elevators, lowering machines and pallet‑transfer equipment. Procurement and workshop adaptation for these accessories push up total expansion investment and lengthen payback cycles. HF18 integrates demolding and stacking into the main‑machine body. Finished blocks can be stacked directly after demolding, removing requirements for complete sets of pallet‑circulation auxiliary equipment. If your brick plant already has batching and mixing systems, you only need to connect them with HF18 main machine for formal production, without adding numerous complicated intermediate auxiliary devices. Compared with purchasing conventional high‑capacity pallet‑based forming machine plus full set of auxiliaries, this solution effectively controls total expansion budget. Once commissioning is finished, the machine quickly enters full‑load mass‑production state to generate operating income and speed up investment payback, easing capital pressure for high‑level expansion of medium‑large brick plants.
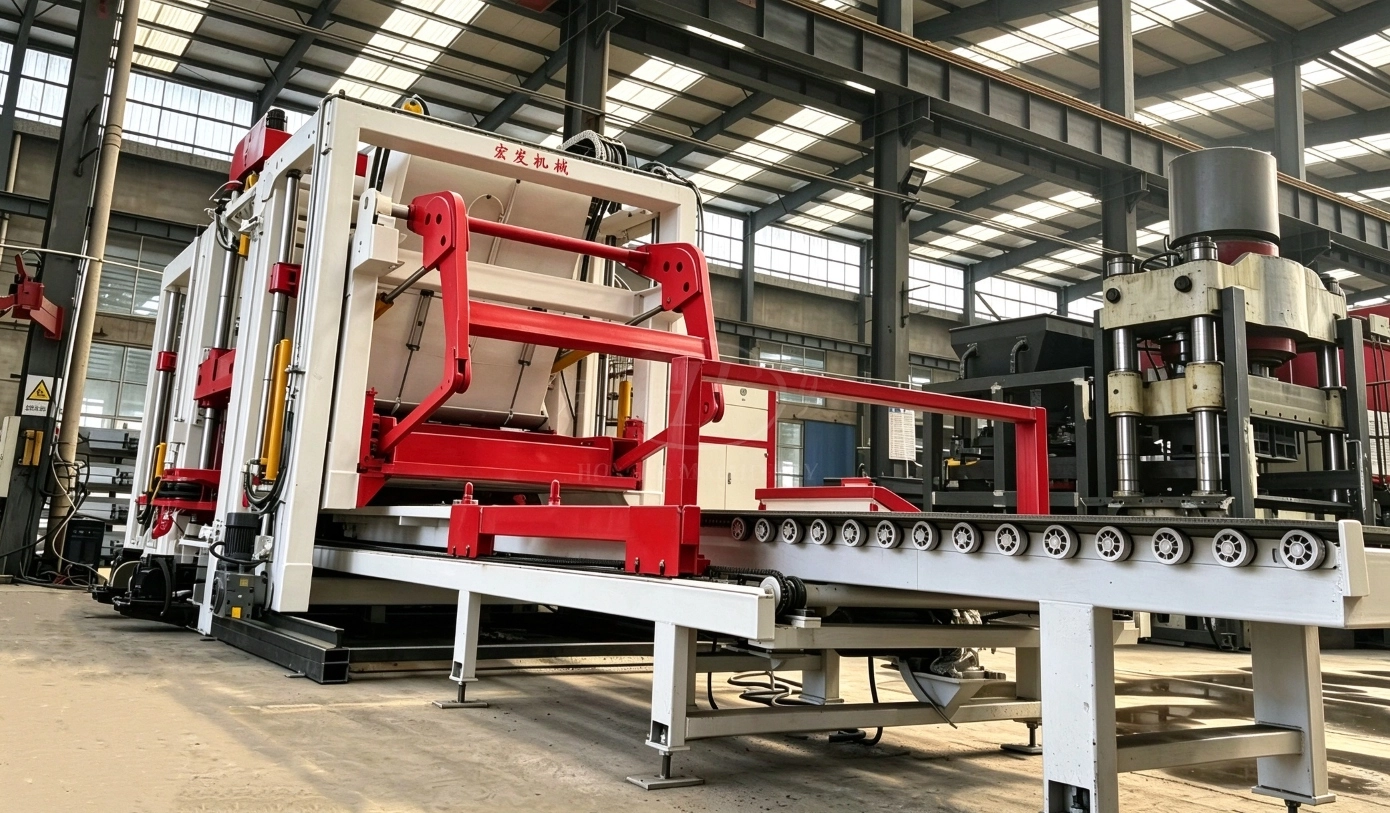
5. Stable Product Quality Under Heavy‑Duty Operation to Secure Large Buyers and Win Renewals & Derivative Supporting Projects
Buyers of super‑large general‑contract projects impose strict requirements on product consistency for continuous bulk supply. Insufficient compaction or dimension deviation during long‑time full‑load production will trigger inspection penalties, delayed payments or even contract termination. You will also lose opportunities for contract renewal and surrounding derivative supporting projects. HF18 adopts multi‑source variable‑frequency vibration forming system. Blocks feature high compaction and are resistant to damage when stacked right after demolding. Even under prolonged non‑stop full‑load operation, both ordinary blocks and colored face‑mix bricks maintain reliable forming quality with uniform dimensions and controlled defect rates. Batches of goods delivered to construction sites can smoothly pass client acceptance and reduce economic losses from rework and product rejection. Reliable bulk‑delivery quality builds deep‑rooted trust with large‑scale engineering buyers. It creates more chances for contract‑renewal invitations and new supply bids for nearby supporting projects, converting one‑time giant supply orders into long‑term stable business cooperation.
1. Pallet‑Free High‑Capacity Main‑Machine Output to Support Super‑Large General‑Contract Project Bulk Supply
Many well‑established large brick plants have rich engineering client resources, yet they are restricted by output limits of conventional pallet‑based forming machines. When facing huge‑volume tenders for urban renewal and large residential clusters, they dare not accept massive‑supply contracts due to insufficient single‑machine output and miss lucrative long‑term projects. Conventional machines also generate recurring costs for pallet procurement and regular replacement caused by wear. As a pallet‑free automatic block forming main unit, HF18 adopts built‑in demolding and stacking mechanism, which removes reliance on large quantities of circulating pallets. It enables intensive continuous mass production of standard bricks, hollow blocks, slope‑protection blocks, colored paving bricks and full‑range engineering products. For capacity expansion of existing brick plants equipped with batching and mixing systems, adding this main machine does not require complete pallet‑flow auxiliary accessories and directly lifts overall plant capacity ceiling. After upgrade, your factory gains solid capability for concentrated delivery of super‑large projects. You become eligible to bid for heavy‑weight engineering projects that were previously unreachable, converting huge potential orders into steady annual revenue and capturing high‑value regional engineering‑supply resources.
2. Remove Pallet Consumable Expenses & Cut On‑Site Labor to Lower Comprehensive Block Costs From Two Dimensions
Besides machine procurement, traditional pallet‑based block forming machines require continuous annual investment for purchasing and replacing worn pallets. Plenty of operators are also needed for pallet transfer and material docking, leading to high labor expenditure. Even when output rises, consumable and labor costs will eat up substantial profit margins. HF18 pallet‑free forming main unit completes demolding and stacking inside the machine. Pallet circulation is eliminated in production process, completely getting rid of ongoing costs for pallet procurement, maintenance and replacement. Thanks to high automation level, only a small number of on‑site staff are required for machine monitoring and finished‑goods handling, significantly cutting post‑s manpower demand. Both consumable and labor expenses are reduced. Combined with economies of scale brought by high main‑machine capacity, fixed expenditures covering labor, power and site overhead are spread over massive quantities of finished blocks to further lower comprehensive per‑unit production cost. During engineering tender quotation, you obtain enhanced pricing flexibility. You can win huge supply contracts with competitive offers while maintaining decent profit margins, realizing simultaneous growth in order volume and profitability.
3. Built‑In Face‑Mix Unit for Diversified Engineering Products to Expand High‑Value Order Channels
Quite a number of large brick factories mainly produce ordinary grey blocks after capacity expansion. Restricted by machine functions, they cannot take high‑margin municipal colored‑landscape‑brick orders. Although production capacity grows, business structure remains single, bringing high operational risks when market demand fluctuates. HF18 main machine is equipped with integrated automatic face‑mix unit. Without modifying main‑machine structure, it stably produces colored paving bricks, plaza bricks and slope‑protection blocks, as well as standard bricks, various hollow blocks, road curbstones and other mainstream engineering blocks. After main‑machine capacity upgrade, your factory can undertake bulk wall‑block supply for residential complexes and high‑profit municipal landscape projects from urban‑renewal initiatives. There is no need to purchase extra dedicated colored‑brick forming equipment. One single main‑machine covers both high‑volume basic products and high‑value landscape articles. Diversified order sources mitigate operational risks caused by declining demand for single‑product categories and ensure high‑capacity utilization with steady incoming orders.
4. Integrated Demolding & Stacking Functions Reduce Auxiliary Equipment Needs and Control Total Expansion Investment
Traditional high‑capacity forming machines demand extra auxiliary devices such as pallet elevators, lowering machines and pallet‑transfer equipment. Procurement and workshop adaptation for these accessories push up total expansion investment and lengthen payback cycles. HF18 integrates demolding and stacking into the main‑machine body. Finished blocks can be stacked directly after demolding, removing requirements for complete sets of pallet‑circulation auxiliary equipment. If your brick plant already has batching and mixing systems, you only need to connect them with HF18 main machine for formal production, without adding numerous complicated intermediate auxiliary devices. Compared with purchasing conventional high‑capacity pallet‑based forming machine plus full set of auxiliaries, this solution effectively controls total expansion budget. Once commissioning is finished, the machine quickly enters full‑load mass‑production state to generate operating income and speed up investment payback, easing capital pressure for high‑level expansion of medium‑large brick plants.
5. Stable Product Quality Under Heavy‑Duty Operation to Secure Large Buyers and Win Renewals & Derivative Supporting Projects
Buyers of super‑large general‑contract projects impose strict requirements on product consistency for continuous bulk supply. Insufficient compaction or dimension deviation during long‑time full‑load production will trigger inspection penalties, delayed payments or even contract termination. You will also lose opportunities for contract renewal and surrounding derivative supporting projects. HF18 adopts multi‑source variable‑frequency vibration forming system. Blocks feature high compaction and are resistant to damage when stacked right after demolding. Even under prolonged non‑stop full‑load operation, both ordinary blocks and colored face‑mix bricks maintain reliable forming quality with uniform dimensions and controlled defect rates. Batches of goods delivered to construction sites can smoothly pass client acceptance and reduce economic losses from rework and product rejection. Reliable bulk‑delivery quality builds deep‑rooted trust with large‑scale engineering buyers. It creates more chances for contract‑renewal invitations and new supply bids for nearby supporting projects, converting one‑time giant supply orders into long‑term stable business cooperation.
 QT6‑15 Automatic Brick Forming Machine | High-output Automatic Line, Single Operator For Bulk Orders
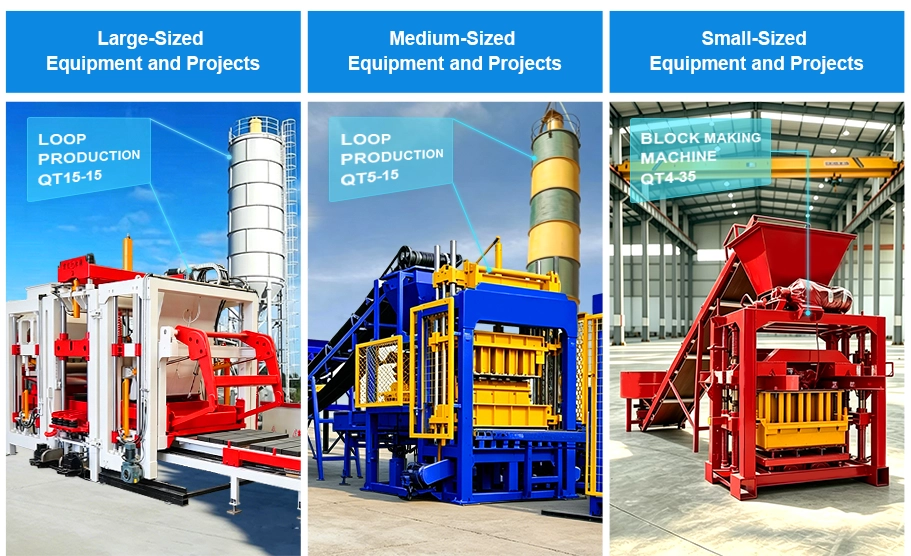
QT6‑15 automatic block forming machine is built for overseas block factories chasing large output. Equipped with complet...

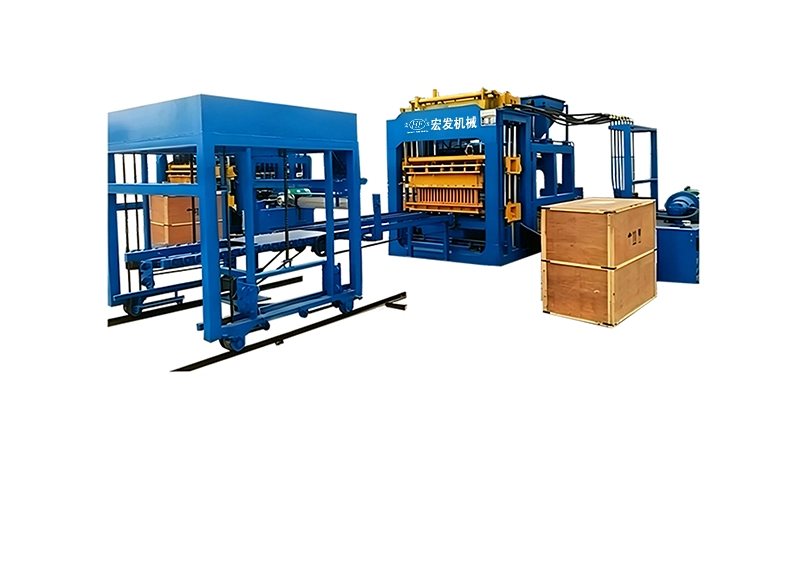 QT5‑15 Automatic Brick Forming Machine | High‑automation Brick Machine, Single Operator Boosts Output Steadily
QT5‑15 automatic block forming machine is designed for medium and large overseas block production lines. Equipped with a...
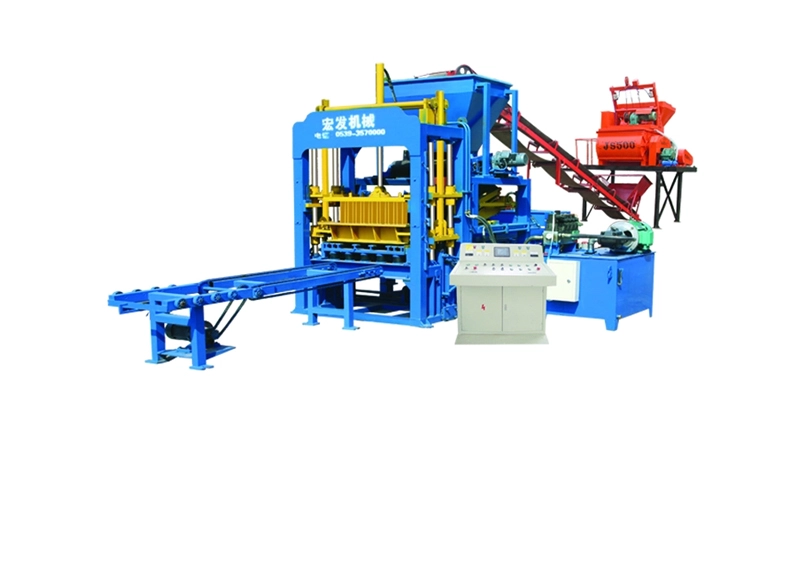 QT4‑15S Automatic Brick Forming Machine | Fully‑automatic Operation, Single‑operator High‑efficient Production
QT4‑15S automatic block forming machine is well‑suited for small‑and‑medium‑sized overseas brick factories. Built‑in ful...
Shandong Hongfa Scientific Industrial&Trading Co.,Ltd ©️2026Copyright © LU ICP B 16041216-4