COMPLETE PROCESS FLOW

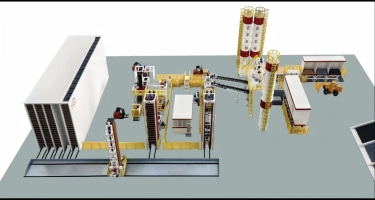

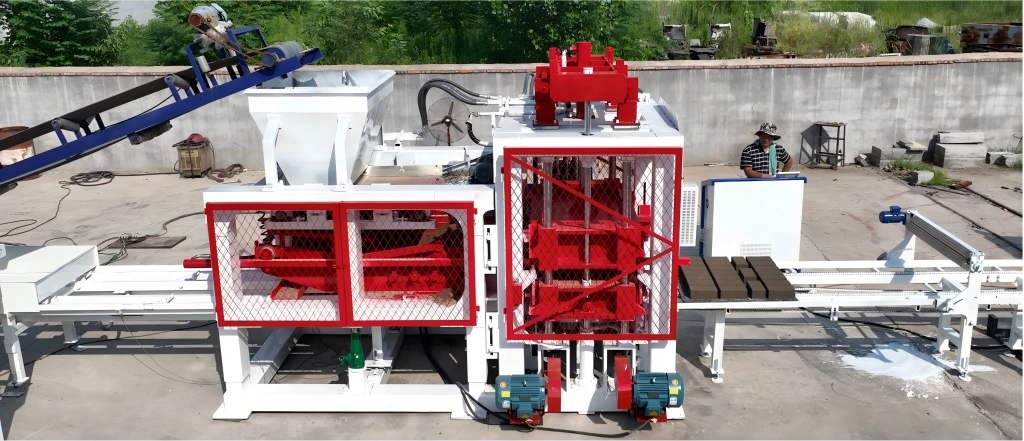
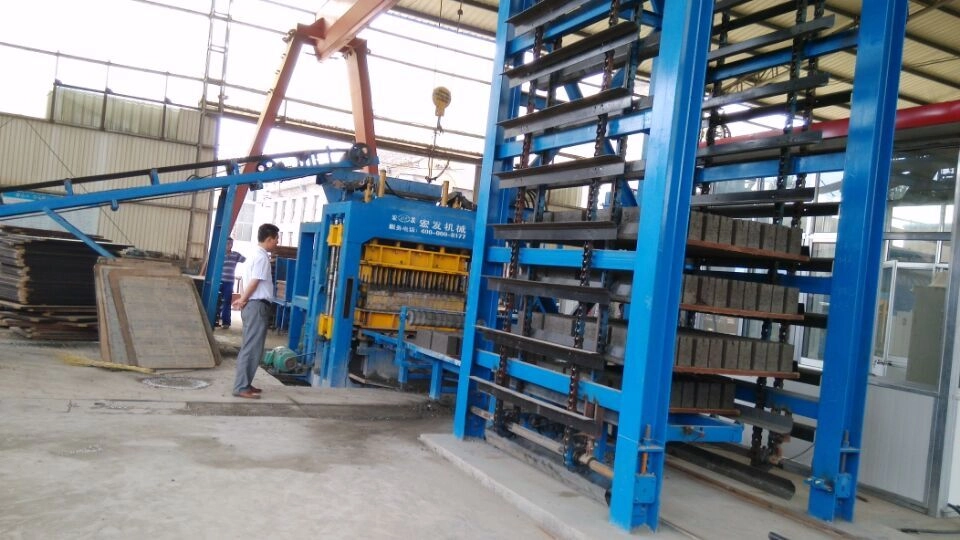
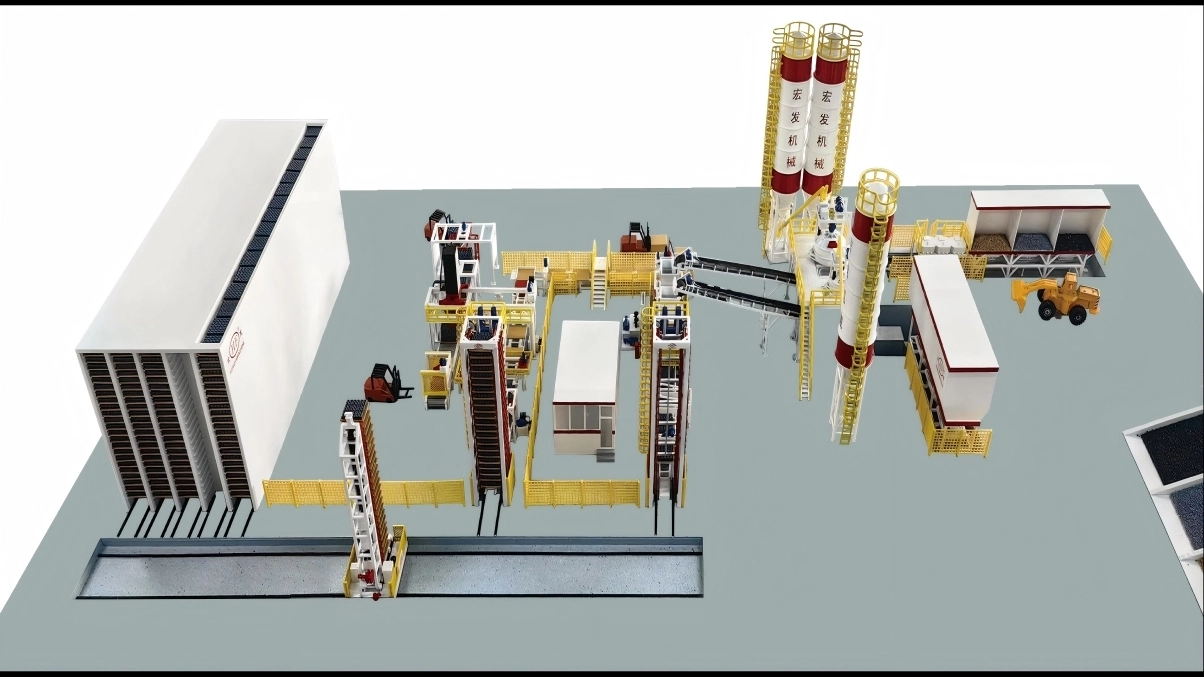
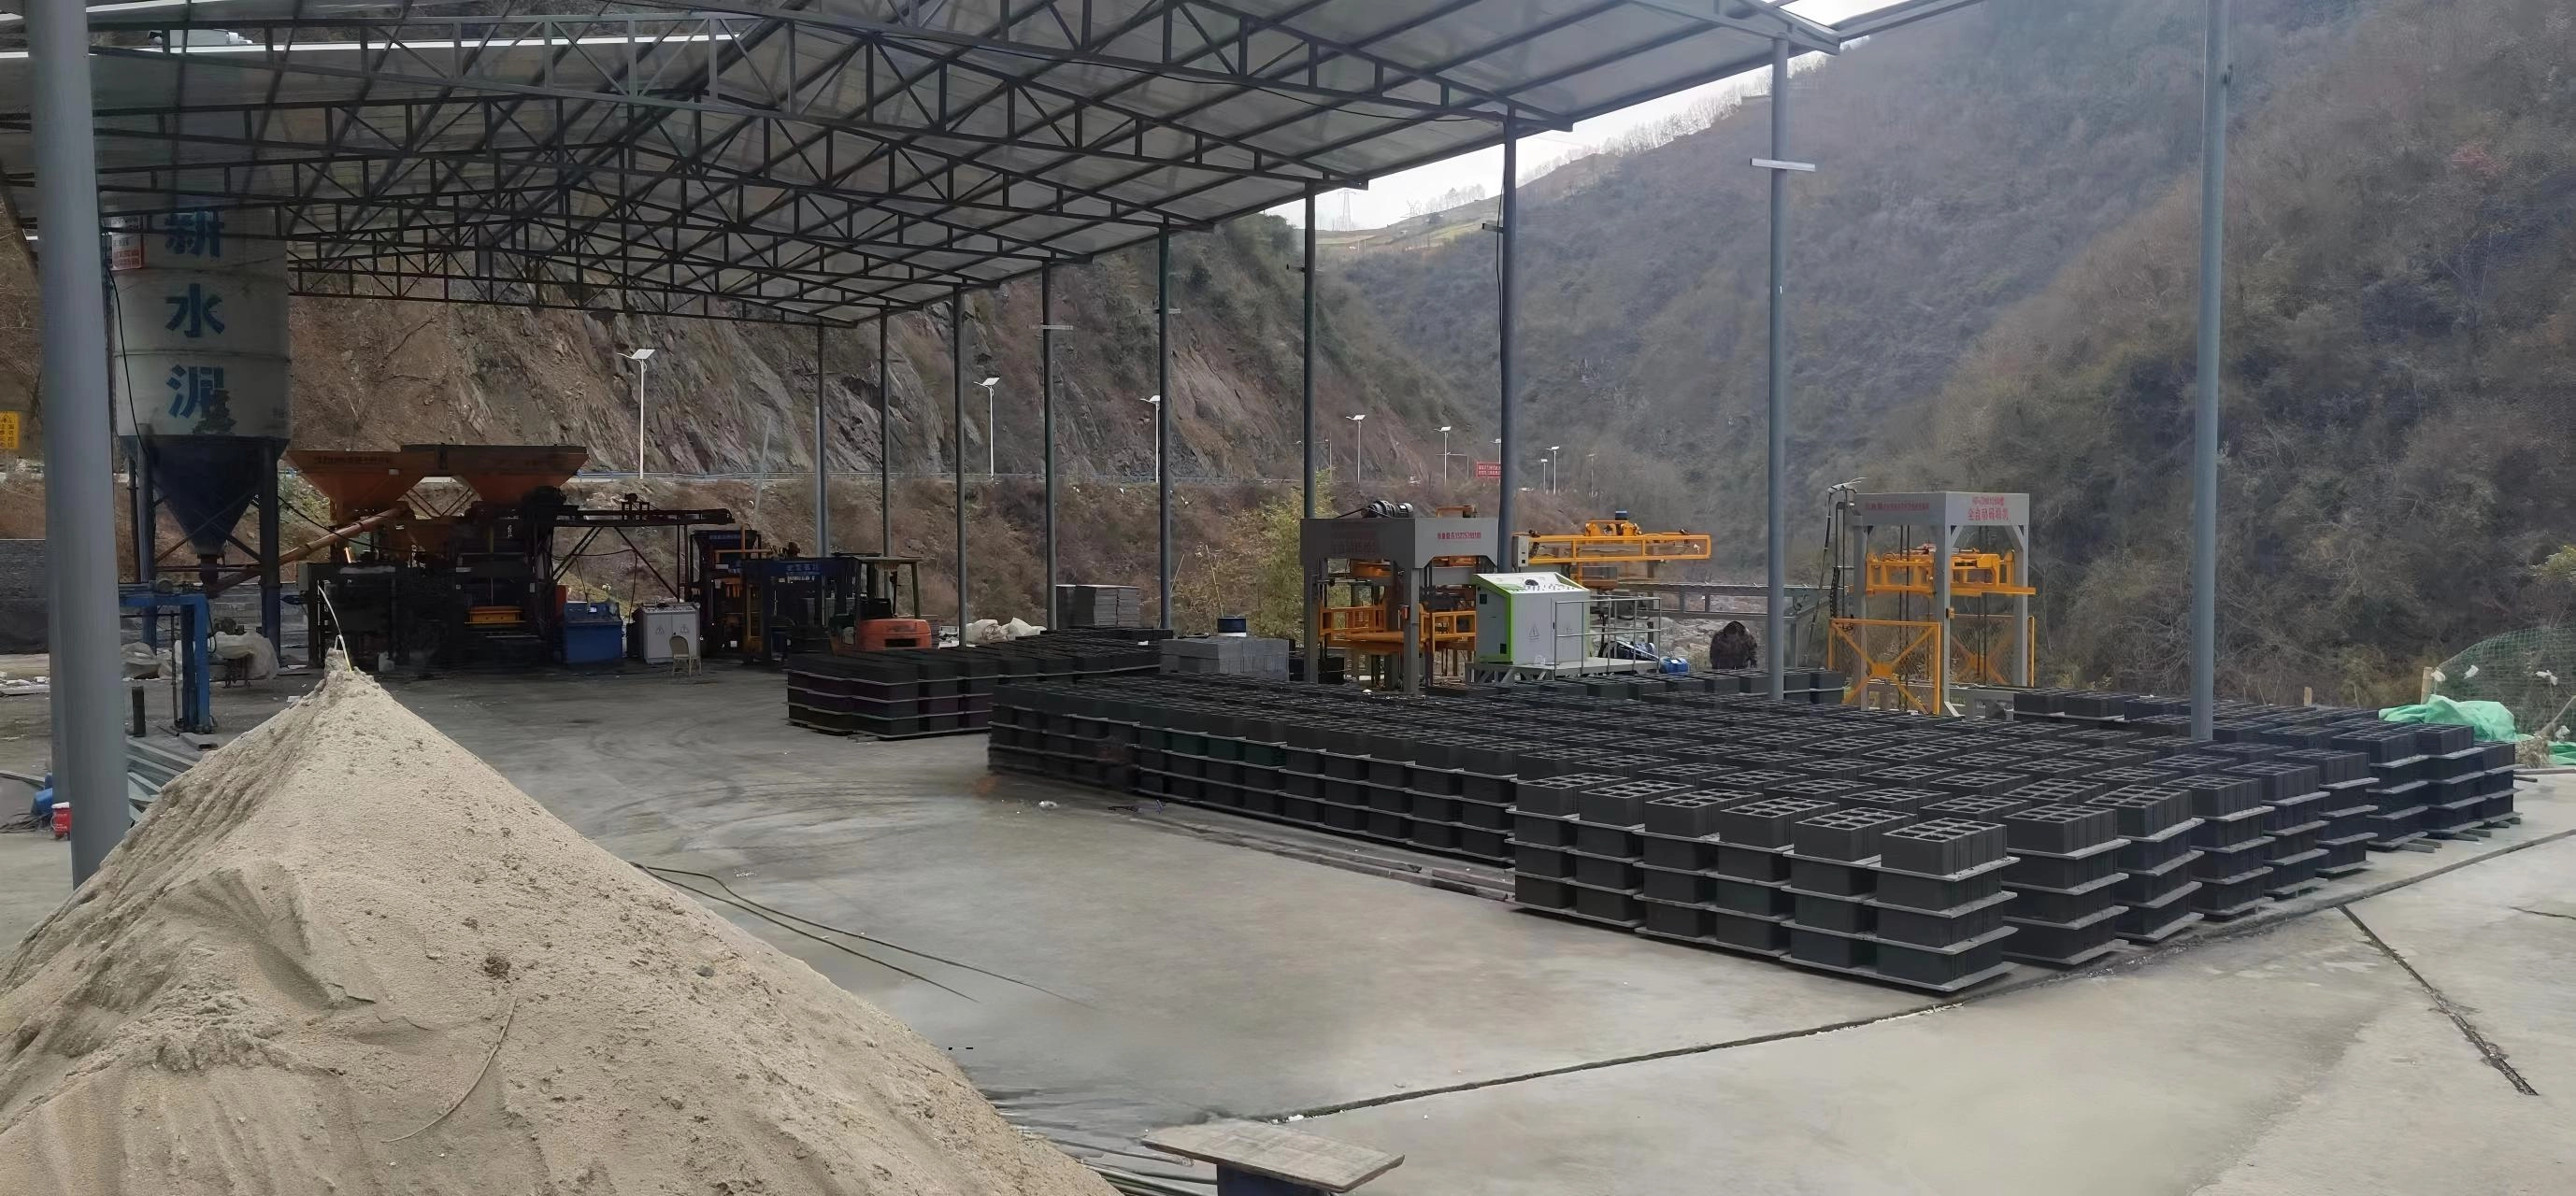
Fully‑automatic brick‑making main machine + mother‑child curing rack + RGV finger transfer vehicle + three‑dimensional curing kiln, applicable to the production of standard cement bricks, tailings solid‑waste bricks and permeable bricks.
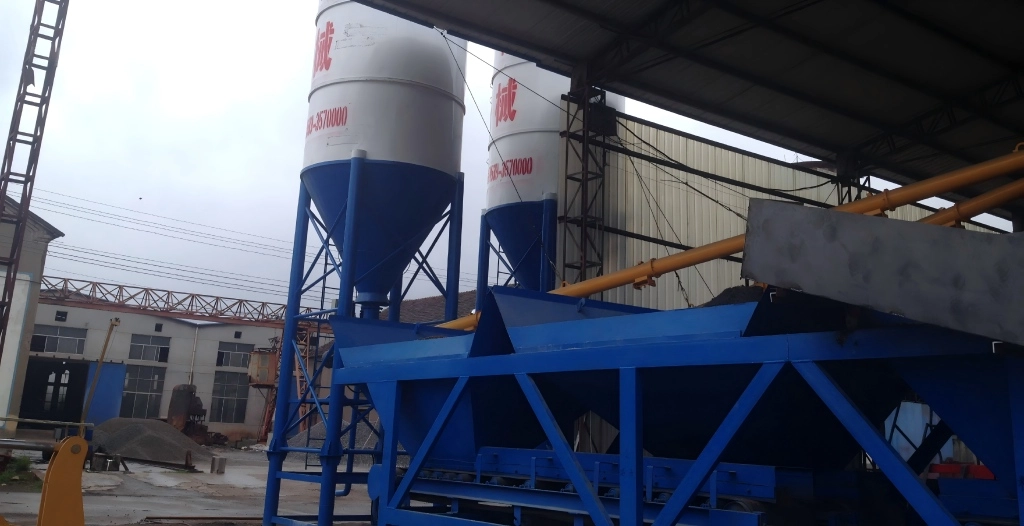
Raw materials including cement, mine tailings, fly ash, stone powder, sand and water are stored in separate silos. The automatic batching system weighs each material according to preset brick formula. All raw materials are transported by belt conveyor to the twinshaft compulsory mixer.
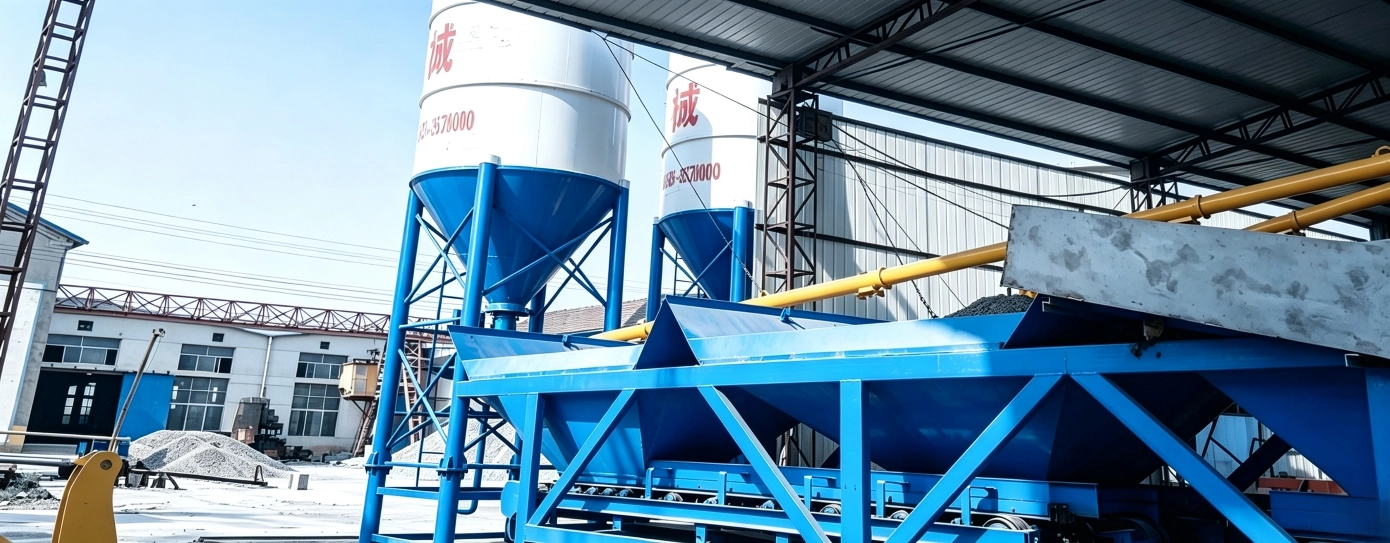
Twinshaft mixer completes highintensity mixing for base material. For colored paver blocks, independent facematerial mixer prepares surface color material separately. Mixed concrete material is discharged to the material receiving hopper of block making host machine.
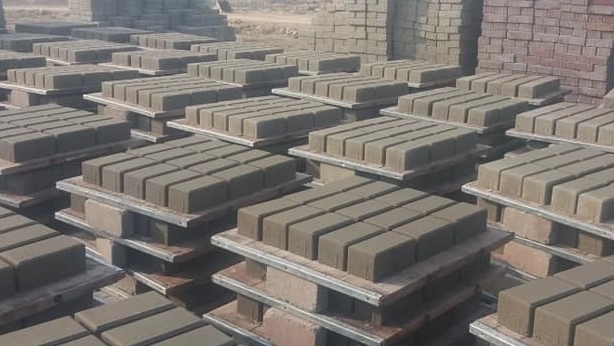
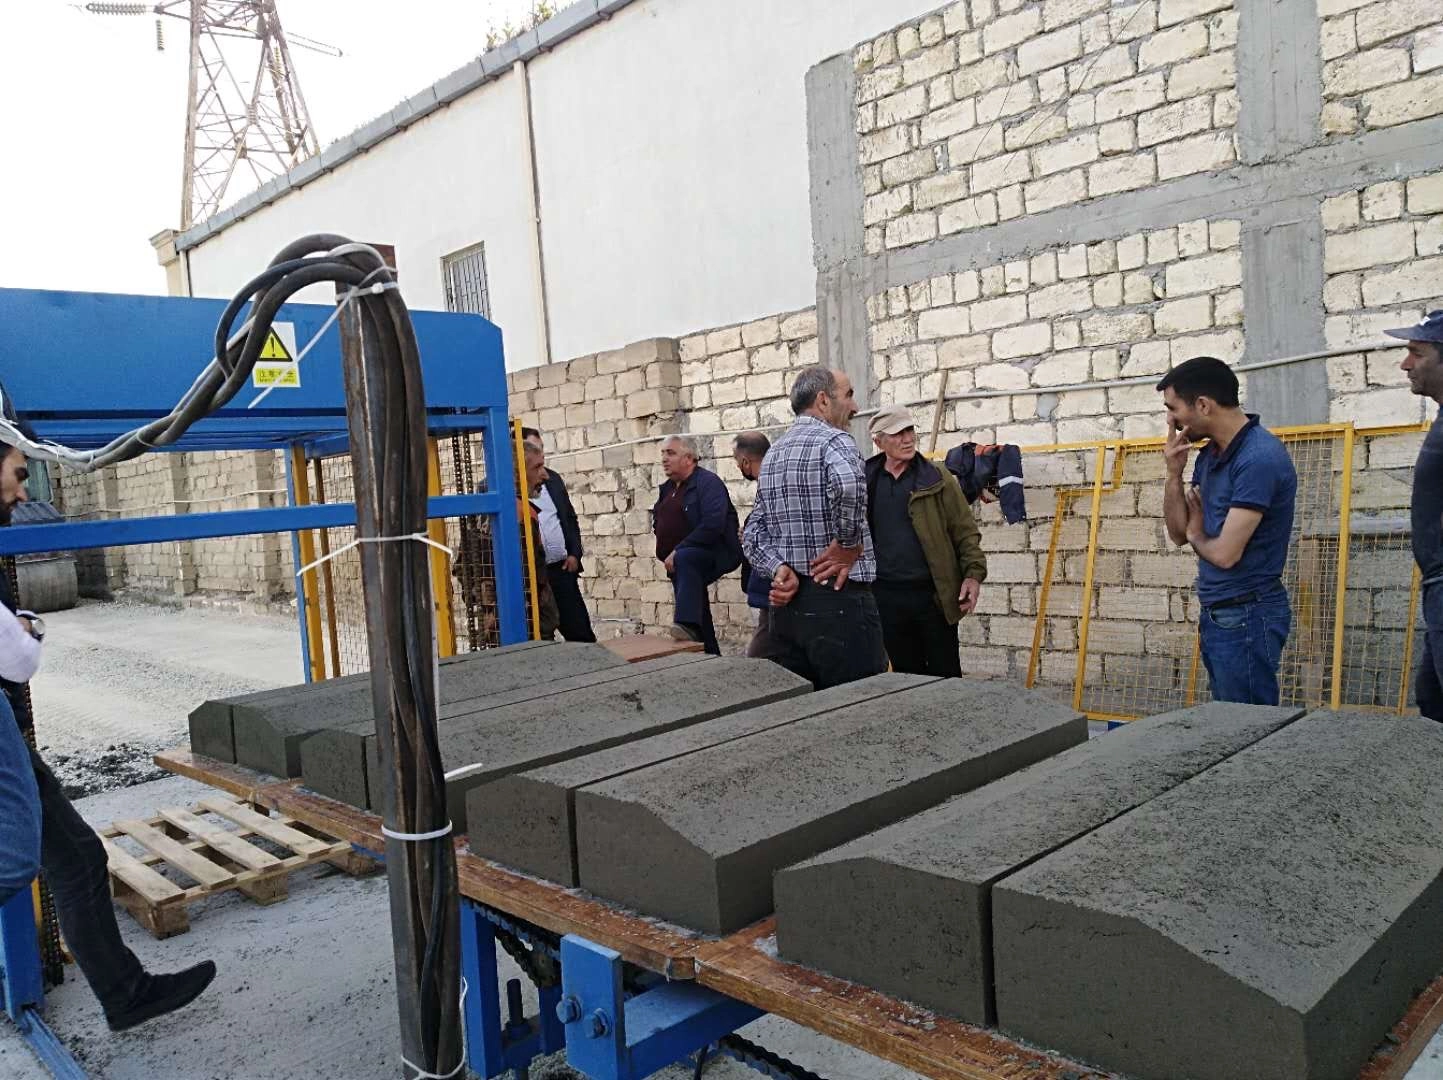
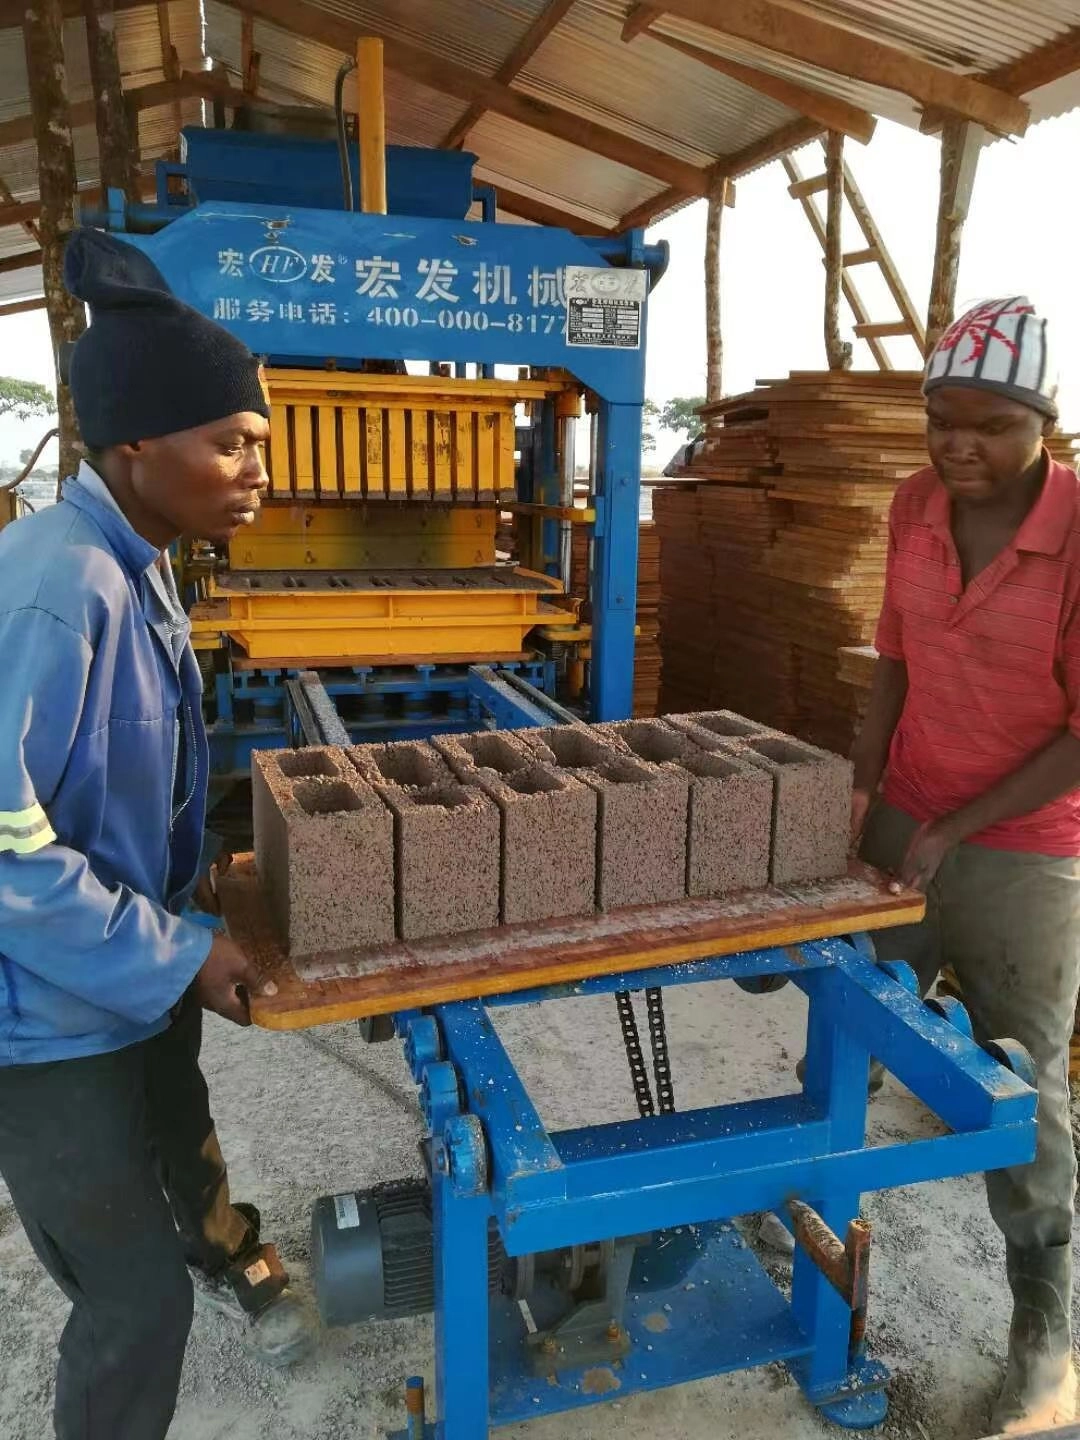
The feeding trolley pushes concrete material into mould box. Highfrequency vibration + hydraulic pressure compacts raw materials inside mould. After forming, the mould lifts up, and green wet blocks are ejected onto the metal pallet. High density green cement blocks are finished in this step.
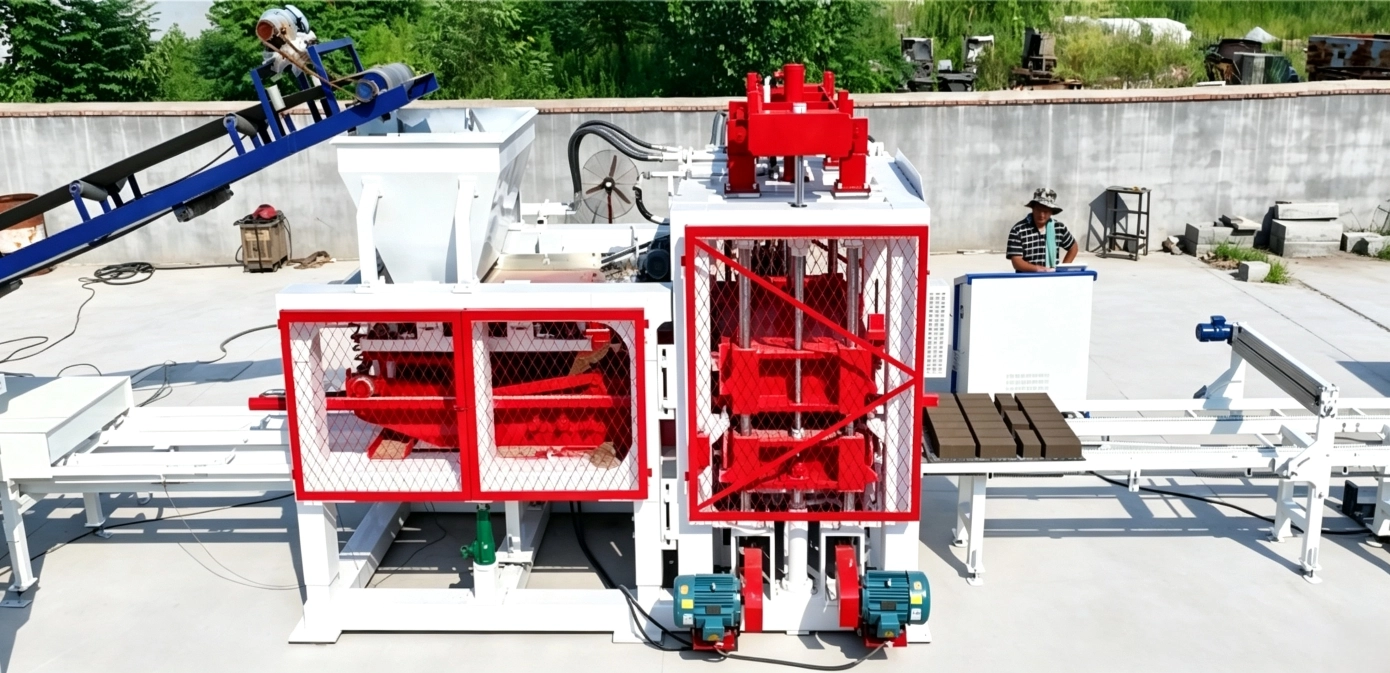
Wet green blocks together with metal pallets are conveyed by roller conveyor. RGV finger car (transfer trolley) grabs pallets carrying green blocks, and loads them layerbylayer onto the empty multilayer curing rack. One full curing rack holds multiple layers of wet blocks.
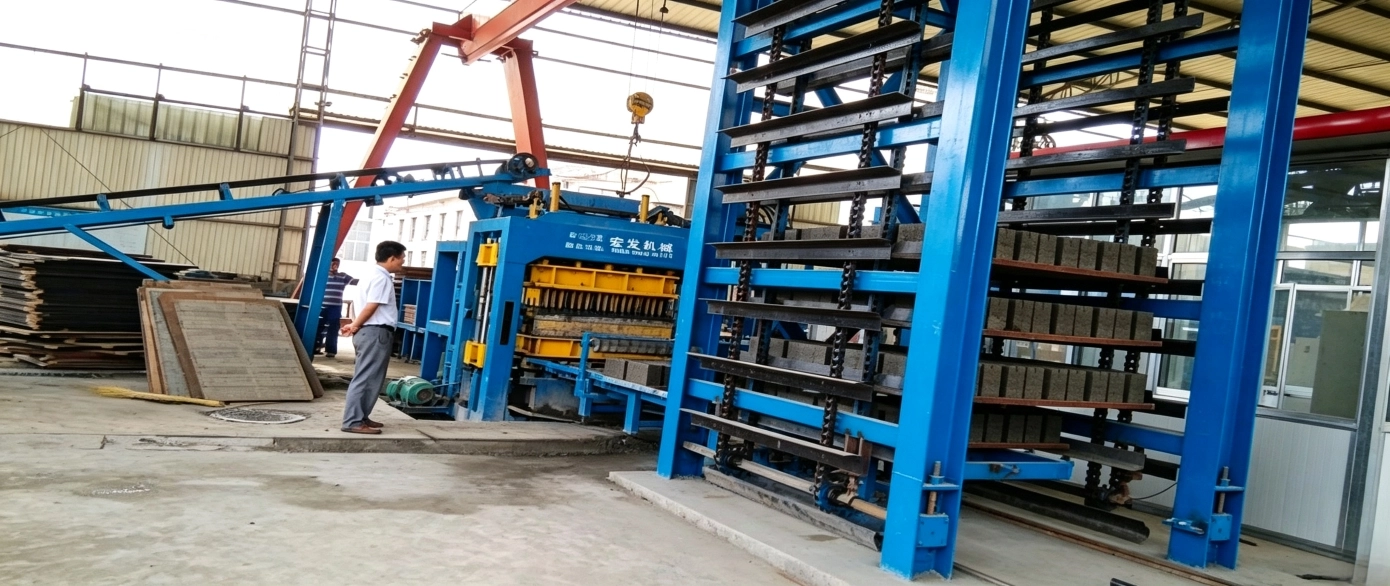
After one curing rack is fully loaded with wet blocks, RGV finger car transfers the whole curing rack into closed thermal curing kiln. Multiple curing racks are arranged inside the curing chamber. Constant temperature & humidity environment is kept inside for block hydration hardening.
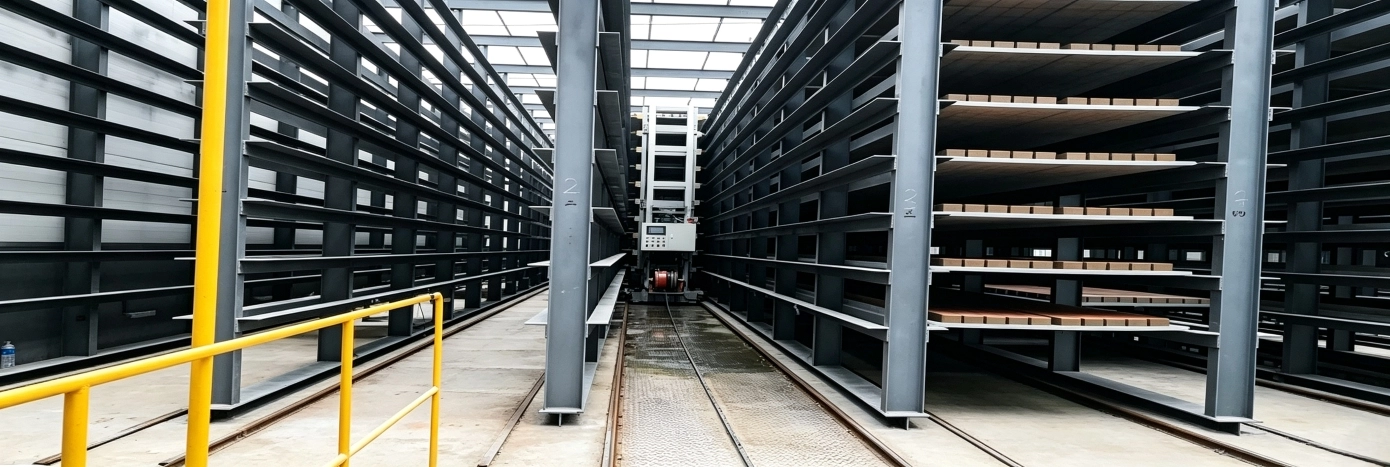
Blocks stay inside curing rack in curing kiln for scheduled curing cycle. Heat source such as airsource heat pump keeps stable temperature. Cement inside green blocks completes hydration reaction, blocks gain compressive strength. Curing time can be adjusted according to local temperature and brick type.
When curing cycle is finished, RGV finger car pulls the whole curing rack out from curing chamber and transports it to deracking station. Blocks have become hard qualified finished cement blocks at this stage.
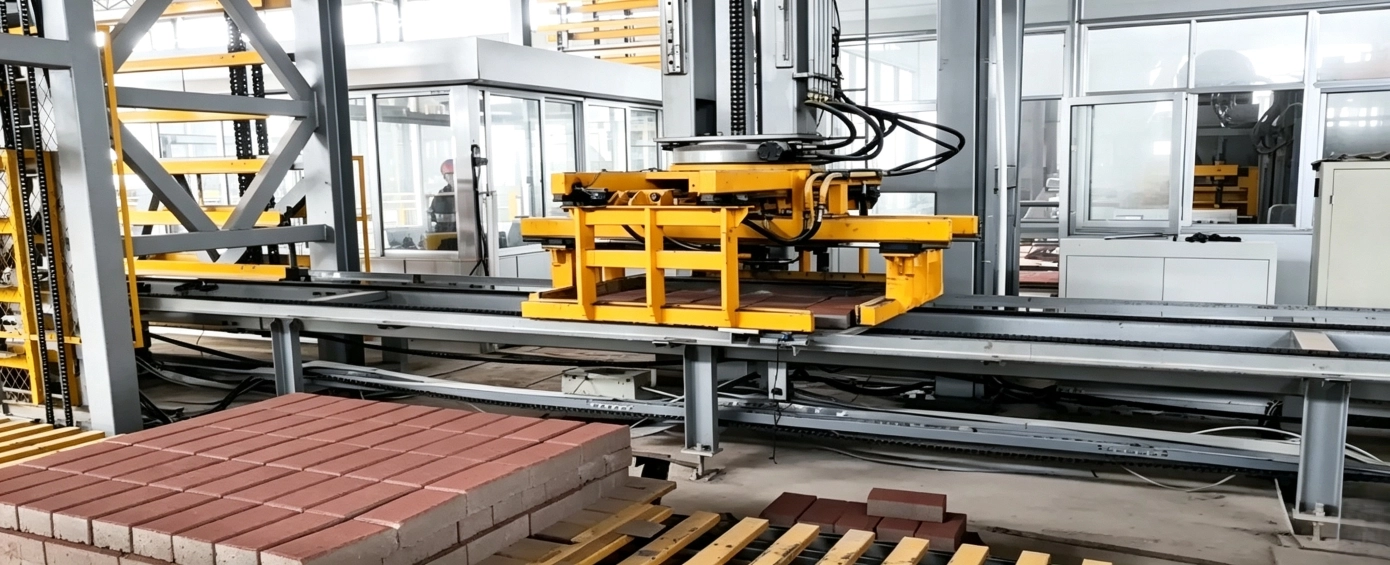
At deracking station, RGV finger car takes out pallets with finished blocks layer by layer from curing rack. Finished blocks on pallets are sent to automatic stacking robot area. Empty curing rack is transported back for next circulation.
Robot stacker picks qualified cement blocks and stacks them onto transport pallet. Finished brick stacks can be wrapped by stretch film for storage or container shipment.
After finished blocks are picked away, empty metal pallets flow back through roller conveyor to block forming host station, for next round brick forming production.
1. Curing racks + RGV finger car realize centralized curing, greatly save factory floor space compared with natural stacking curing.
2. Whole line runs automatically, few workers required.
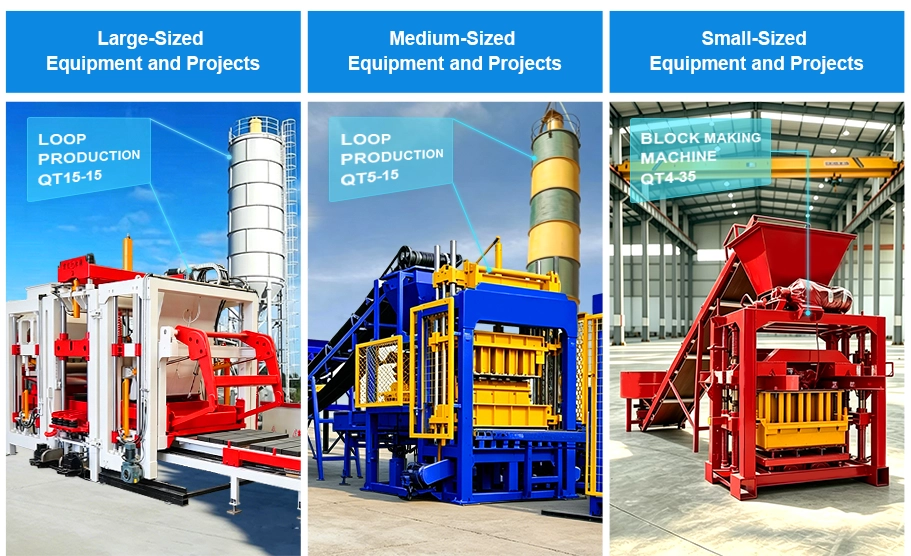
3. Suitable for cement bricks, tailings recycling bricks, paver blocks, hollow blocks.
 QT12-15 Fully Automatic Concrete Brick Making Machine | Hollow Block & Paving Brick Molding Equipment with Custom Molds
QT12-15 fully automatic concrete brick making machine supports custom molds for hollow blocks, pavers, curbs and slope b...
 QT12-15 Automatic Concrete Brick Making Machine in Turkish | Construction Machinery
QT12-15 automatic concrete brick making machine matched for Turkish brick plants, adopts vibration forming method & ...
 QT10-15 Automatic Concrete Brick Making Machine
QT10-15 automatic concrete brick making machine combines machinery, hydraulics and PLC control. Its 21MPa table vibratio...
Shandong Hongfa Scientific Industrial&Trading Co.,Ltd ©️2026Copyright © LU ICP B 16041216-4